
Cpk and Ppk show how a measured injection-molding process compares with specification limits, but they answer slightly different buyer questions. Cpk is commonly used as a within-process capability estimate that considers variation and centering; Ppk is a longer-term performance estimate that uses overall observed variation. Both depend on the sample, measurement system, distribution, tolerance and process conditions behind the calculation. A high number is not, by itself, proof that every future lot will conform.[1] [2]
For an OEM or procurement team in Europe, the United States or the Middle East, ask the molder to connect each index to the approved drawing revision, cavity, resin grade, machine, measurement method and production state. The result should support a decision about risk and controls, not replace dimensional results or a documented control plan.
Quote-oriented CTA model: ‘Please quote a capability study for drawing revision [X], feature [Y], tool/cavity [Z] and resin grade [A]. State the sampling plan, measurement method, stability checks, Cpk/Ppk calculation convention, confidence information, report contents, exclusions and the price for any follow-up study.’
01
What the two indices measure
Both indices relate process spread to the width between the lower and upper specification limits. In the familiar two-sided case, Cpk uses the estimated mean and within-process standard deviation, taking the smaller distance to either limit. It therefore reflects both variation and how close the process average is to the nearer limit. Ppk uses the overall sample standard deviation, so it can include more of the time-to-time, lot-to-lot, shift-to-shift or other observed variation. Exact formulas and naming conventions should be stated in the supplier’s report because software settings and industry practices can differ.[1] ISO 22514-1 provides a formal framework for capability and performance terminology, but the applicable customer or sector method should still be agreed in the quality plan.[4]
Cp is useful as a companion to Cpk because it describes potential spread without the same centering penalty. A gap between Cp and Cpk can indicate that the process is offset toward one specification limit. Pp and Ppk are the corresponding performance view using overall variation. Buyers should not read Cpk or Ppk as a percentage of conforming parts unless the distributional assumptions, tails and calculation method have been checked.[1]
| Index or evidence | What it emphasizes | Buyer interpretation |
|---|---|---|
| Cp | Potential spread relative to tolerance, without centering | Useful with Cpk to see whether centering is reducing the margin. |
| Cpk | Within-process spread plus distance to the nearer limit | Ask whether the process was stable and whether the within variation is defined. |
| Pp | Overall observed spread relative to tolerance | Shows how much variation appeared across the selected study period. |
| Ppk | Overall spread plus distance to the nearer limit | Often the more conservative performance view, but only for the sampled conditions. |
| Time order and control chart | Drift, shifts, cycles or special causes | Essential context; an index cannot explain an unstable process. |
02
Stability comes before capability
A capability index assumes that the process being summarized is sufficiently consistent for the estimate to mean something. NIST describes a stable process as having constant mean and variance over time and recommends examining observations in time order with graphical methods such as scatter plots or control charts.[2] In injection molding, that means considering warm-up, material condition, cavity differences, machine changes, operator adjustments, shift changes, cooling behaviour and tool condition rather than treating a convenient run of parts as automatically representative.
If the data show drift, a step change or special-cause behaviour, first investigate the cause and define the relevant production state. A single pooled Ppk may be low because the process truly performs poorly, because multiple states were mixed, or because the study spans an unapproved change. A high Cpk from a short, carefully adjusted run can also hide longer-term movement. Request the time-ordered data, subgroup logic and any exclusions before accepting the headline value.
03
Sampling determines what the number can say
The sampling plan defines the population that the index describes. Samples taken close together can estimate short-term variation, while samples spread across time, cavities, starts, shifts, lots or production runs can reveal additional sources of variation. ASQ cautions that capability estimates depend on representative sampling from a stable system and that simple rules such as taking roughly 30 observations may not represent the process in every situation.[3]
Ask how many parts were measured, how they were selected, whether all cavities were represented, whether parts were conditioned before measurement, and whether repeated measurements were treated correctly. The report should identify the study window and explain exclusions. A small or narrowly selected sample may be useful for an early check, but it should not be presented as evidence for all future production without qualification.
Cpk and Ppk are sample statistics, not exact properties known without uncertainty. NIST discusses confidence limits and notes that capability-index estimates vary with sample size.[1] For a purchasing decision, request a confidence interval or other uncertainty treatment when the result is close to an internal threshold or when the consequence of misclassification is high.
04
Tolerance and measurement can change the conclusion
Capability is always relative to the specification being used. A broad commercial tolerance may produce a comfortable index while a tighter functional interface on the same part does not. Confirm the lower and upper limits, nominal target, unilateral limits where applicable, units, datum scheme and drawing revision. Do not silently substitute a supplier’s preferred tolerance or a process target for the customer’s released requirement.
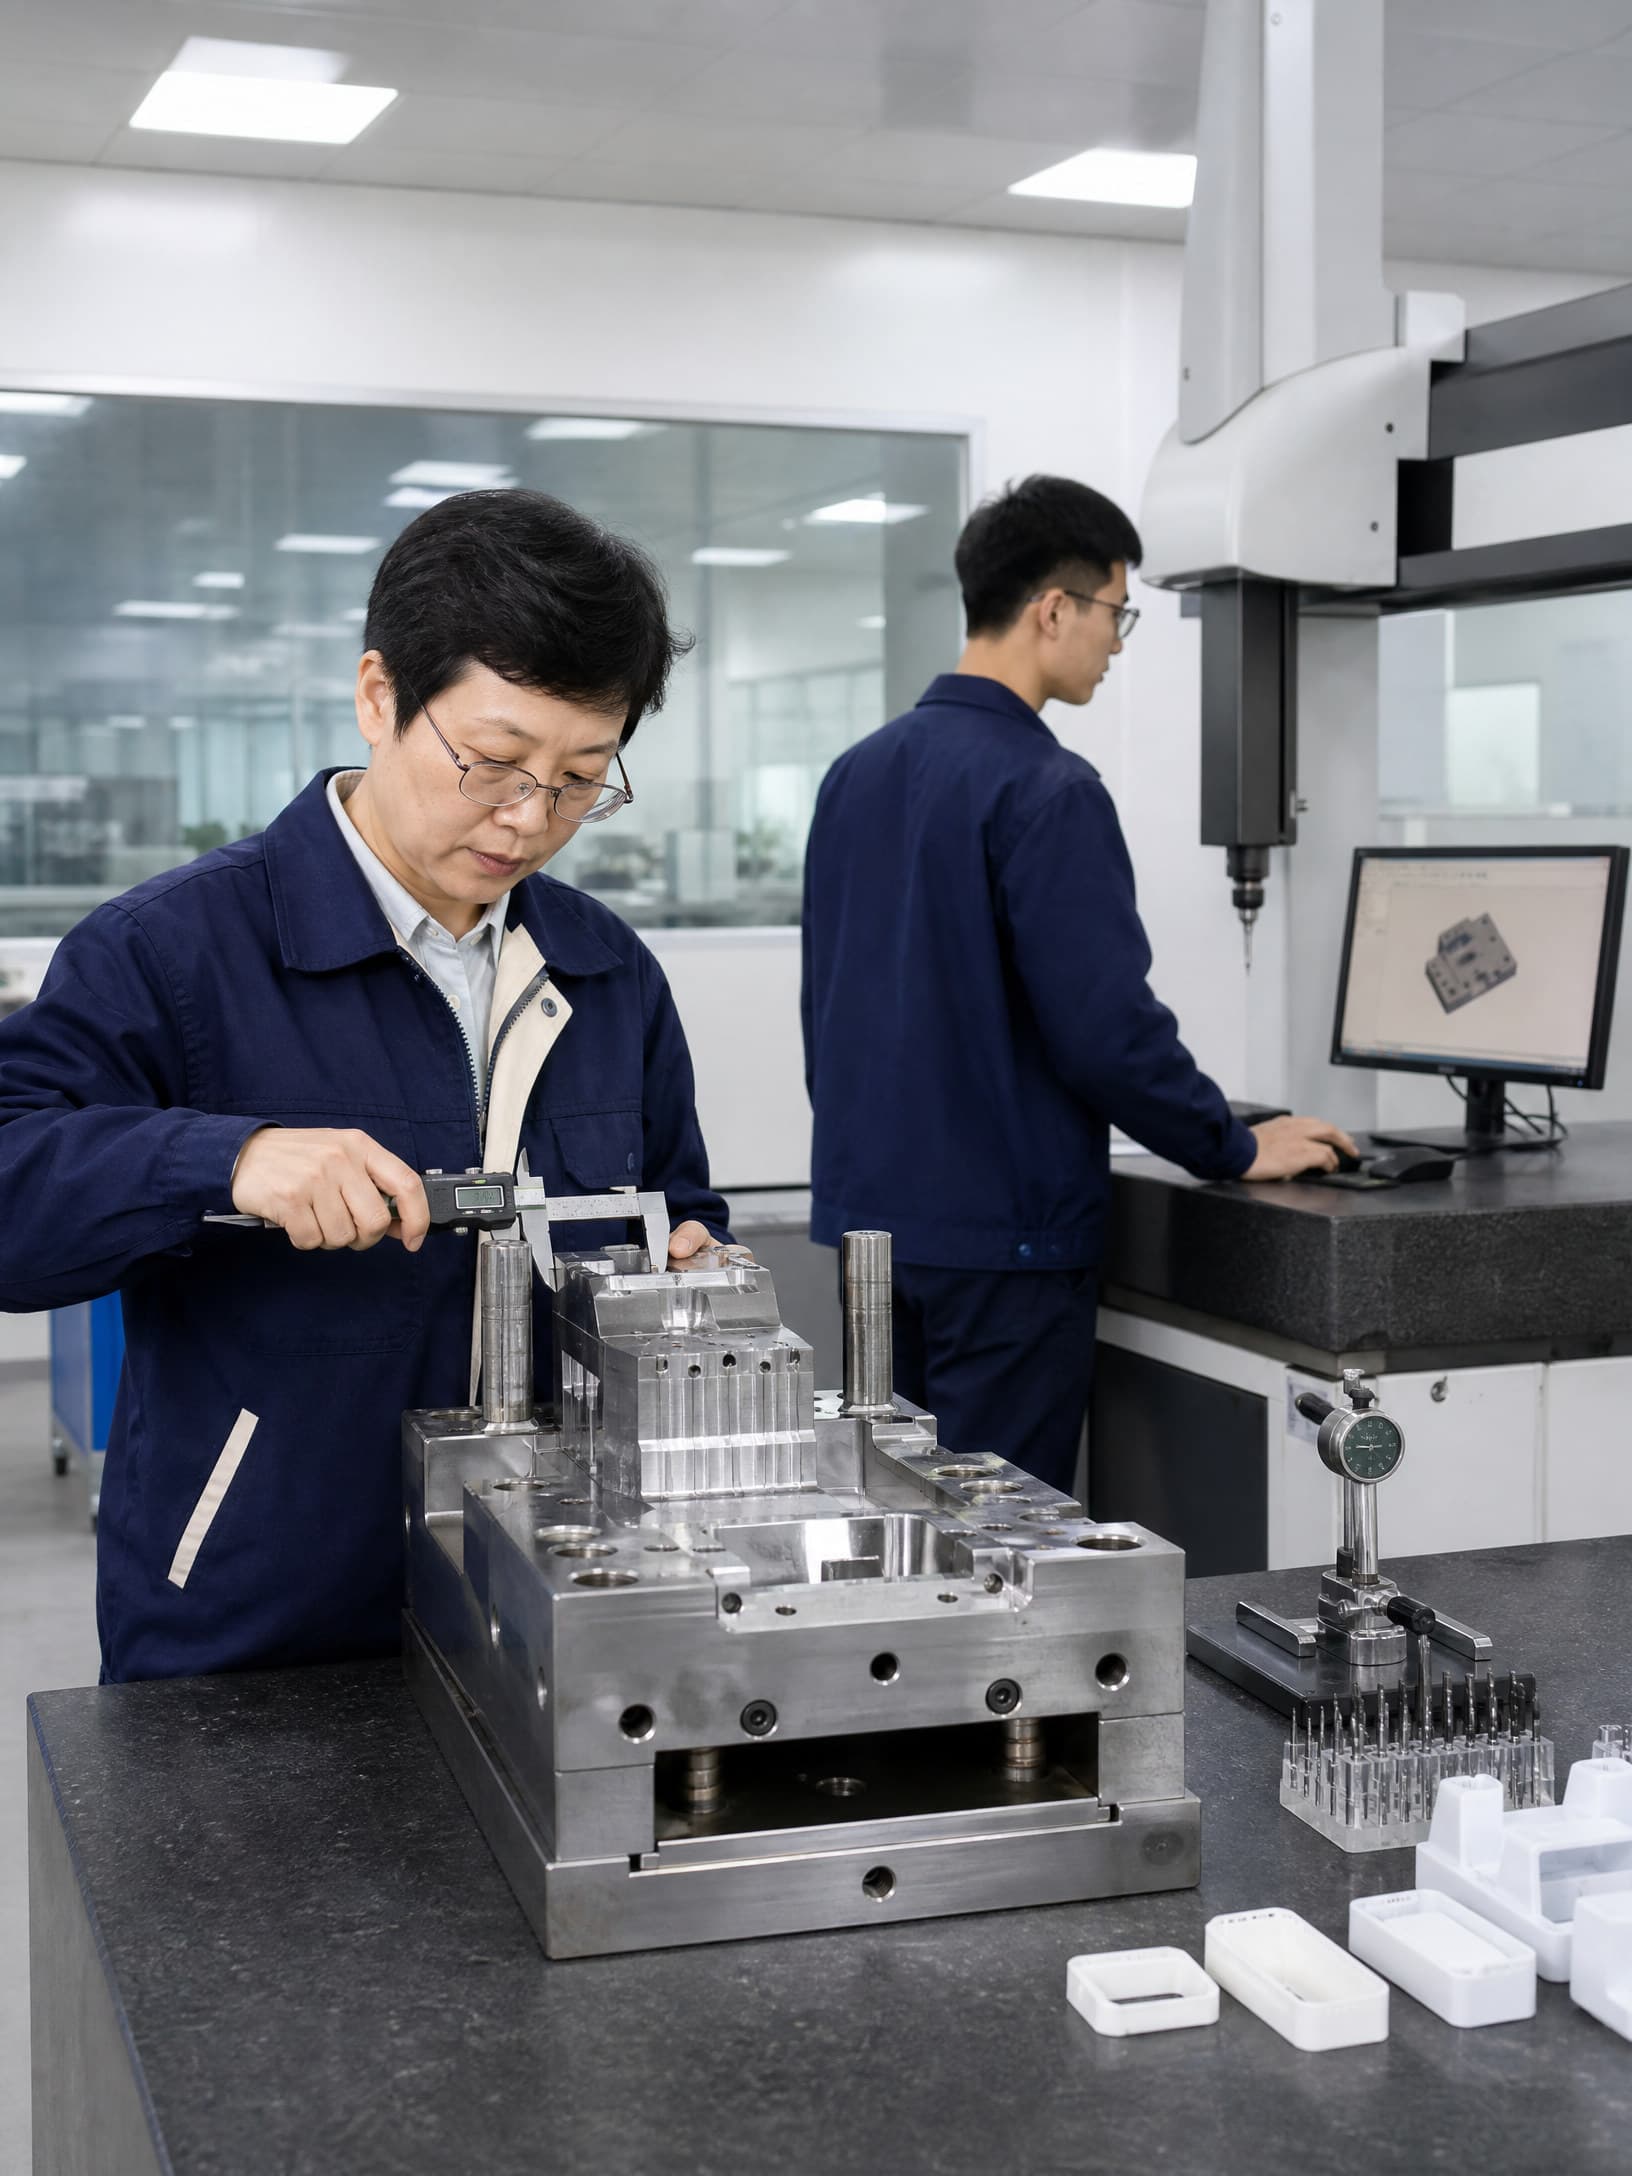
The measurement system is part of the evidence. Identify the instrument, resolution, fixture, calibration status, operator or lab, measurement location, environmental conditions and method for features affected by temperature, conditioning or part handling. If measurement variation is material, the calculated process spread may be distorted. A buyer can reasonably ask for the measurement-system study or justification that supports the selected method before using Cpk or Ppk for release.
05
How buyers should review a capability report
Treat the index as one line in an evidence package. The report should identify the part and revision, feature and limits, tool and cavity, resin and lot, machine, process state, measurement method, sample selection, time order, distribution review, calculation convention, exclusions and raw or summarized results. Ask the supplier to show both the index and the data pattern. A histogram without time order can hide drift; a control chart without tolerance limits cannot show conformance risk.
Avoid adopting a universal pass number without the product owner’s risk analysis, customer requirements and applicable quality plan. If an internal rule is used, record whether it applies to a preliminary capability study, a production performance study, a specific feature class or a special process. When the number is below the decision rule, possible responses include centering the process, reducing variation, revisiting an unrealistic tolerance through formal engineering change, improving measurement, separating cavities or investigating special causes. The appropriate response depends on the failure mode and cannot be inferred from the index alone.
For quotation and supplier selection, ask for a priced evidence package rather than a promise of a future Cpk or Ppk. Define the feature list, study conditions, sample plan, report format, reaction plan and any repeat study after tool, material, machine or measurement changes. That keeps the commercial comparison aligned with the technical decision.
Practical takeaway
Before you move
to the next review.
- The report names the released drawing revision, feature, specification limits, units and tolerance type.
- The sample plan explains part selection, cavity coverage, time span, material condition and exclusions.
- Time-ordered data or control-chart evidence supports the stated process stability.
- The measurement method, equipment, calibration or verification status and measurement-system rationale are documented.
- The supplier states the Cpk/Ppk convention, uncertainty treatment, decision rule, change triggers and follow-up actions.
FAQ
Common questions
Is Ppk always lower than Cpk?
Not always, but it is often lower when overall variation includes changes that are not present in the within-process estimate. The relationship depends on the data, subgrouping and calculation convention. Ask the supplier to show how each standard deviation was calculated rather than assuming a fixed ordering.
Does a high Cpk prove that every molded part will be in specification?
No. It summarizes the sampled process under stated conditions and assumptions. It does not cover an unrepresented cavity, resin lot, machine transfer, tool change, unstable period or measurement problem.
How many samples should an injection-molding capability study include?
There is no single number that fits every part and decision. Sample quantity and spacing should represent the intended production state, account for cavities and sources of variation, and support the desired uncertainty. NIST notes that capability estimates require sufficient data and that their uncertainty matters.[1]
Can capability indices be used for non-normal molded-part data?
They can require additional analysis or an alternative method. Cpk and related conventional estimates are sensitive to distributional assumptions. Review the data shape, transformation or non-normal approach with the quality and engineering teams before applying a normal-based interpretation.[3]
Should buyers request Cpk or Ppk in an RFQ?
You can request a capability study, but define the feature, limits, sample plan, process state, measurement method and report contents first. Requesting a bare target number may encourage a narrow or adjusted study that is difficult to compare across suppliers.
References
Source material
- [1] National Institute of Standards and Technology, “What is Process Capability?”
- [2] National Institute of Standards and Technology, “Assessing Process Stability.”
- [3] American Society for Quality, “What is Process Capability?”
- [4] International Organization for Standardization, “ISO 22514-1:2014 Statistical methods in process management — Capability and performance — Part 1.”
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.