
FAI, PPAP and process capability studies answer related but different buyer questions. First Article Inspection asks whether a representative part has been checked against the released requirements. PPAP packages the evidence and approvals needed for a defined production process, especially where an automotive customer or contract requires that framework. A capability study examines variation against specification limits under stated conditions. None of these labels, on its own, proves that every future shipment will conform. The useful procurement question is: what was measured, on which parts and process, using which method, against which revision, and who approved the remaining risk?
Treat FAI, PPAP and capability as linked evidence streams, not interchangeable certificates. Agree the required submission level, sample conditions, acceptance criteria, deviation route and production-release authority before the supplier starts the approval run.
01
Define the approval question before requesting documents
Start with the product and programme context. A new mold, revised cavity, changed resin grade, transferred tool, changed machine or long production interruption may trigger a new or partial first-article review, a PPAP resubmission or another customer-defined approval. The trigger depends on the purchase specification, quality agreement, customer requirements and industry context. Do not assume that the word PPAP automatically defines the same submission contents for every buyer.
Separate three decisions in your request. FAI evidence should show that the released design requirements were understood and checked on identified parts. PPAP should show that the proposed production process and its controls support the agreed product requirements. Capability evidence should show how selected characteristics behaved under stated production conditions. If the part is aerospace, ask whether the customer flows down the current AS9102 requirement; IAQG describes 9102 as a standardized FAI process for aviation, space and defense products, while noting it can be used in other sectors when agreed [1].
Put the approval boundary in writing. The product owner defines functional requirements, critical-to-quality features, visual standards and market obligations. The supplier explains the molding process, inspection method, control plan and available records. For a regulated product, the legal manufacturer or responsible product owner remains accountable for its regulatory and validation decisions; the supplier’s package is supporting evidence, not a substitute for that approval.
02
Request an identifiable first-article package
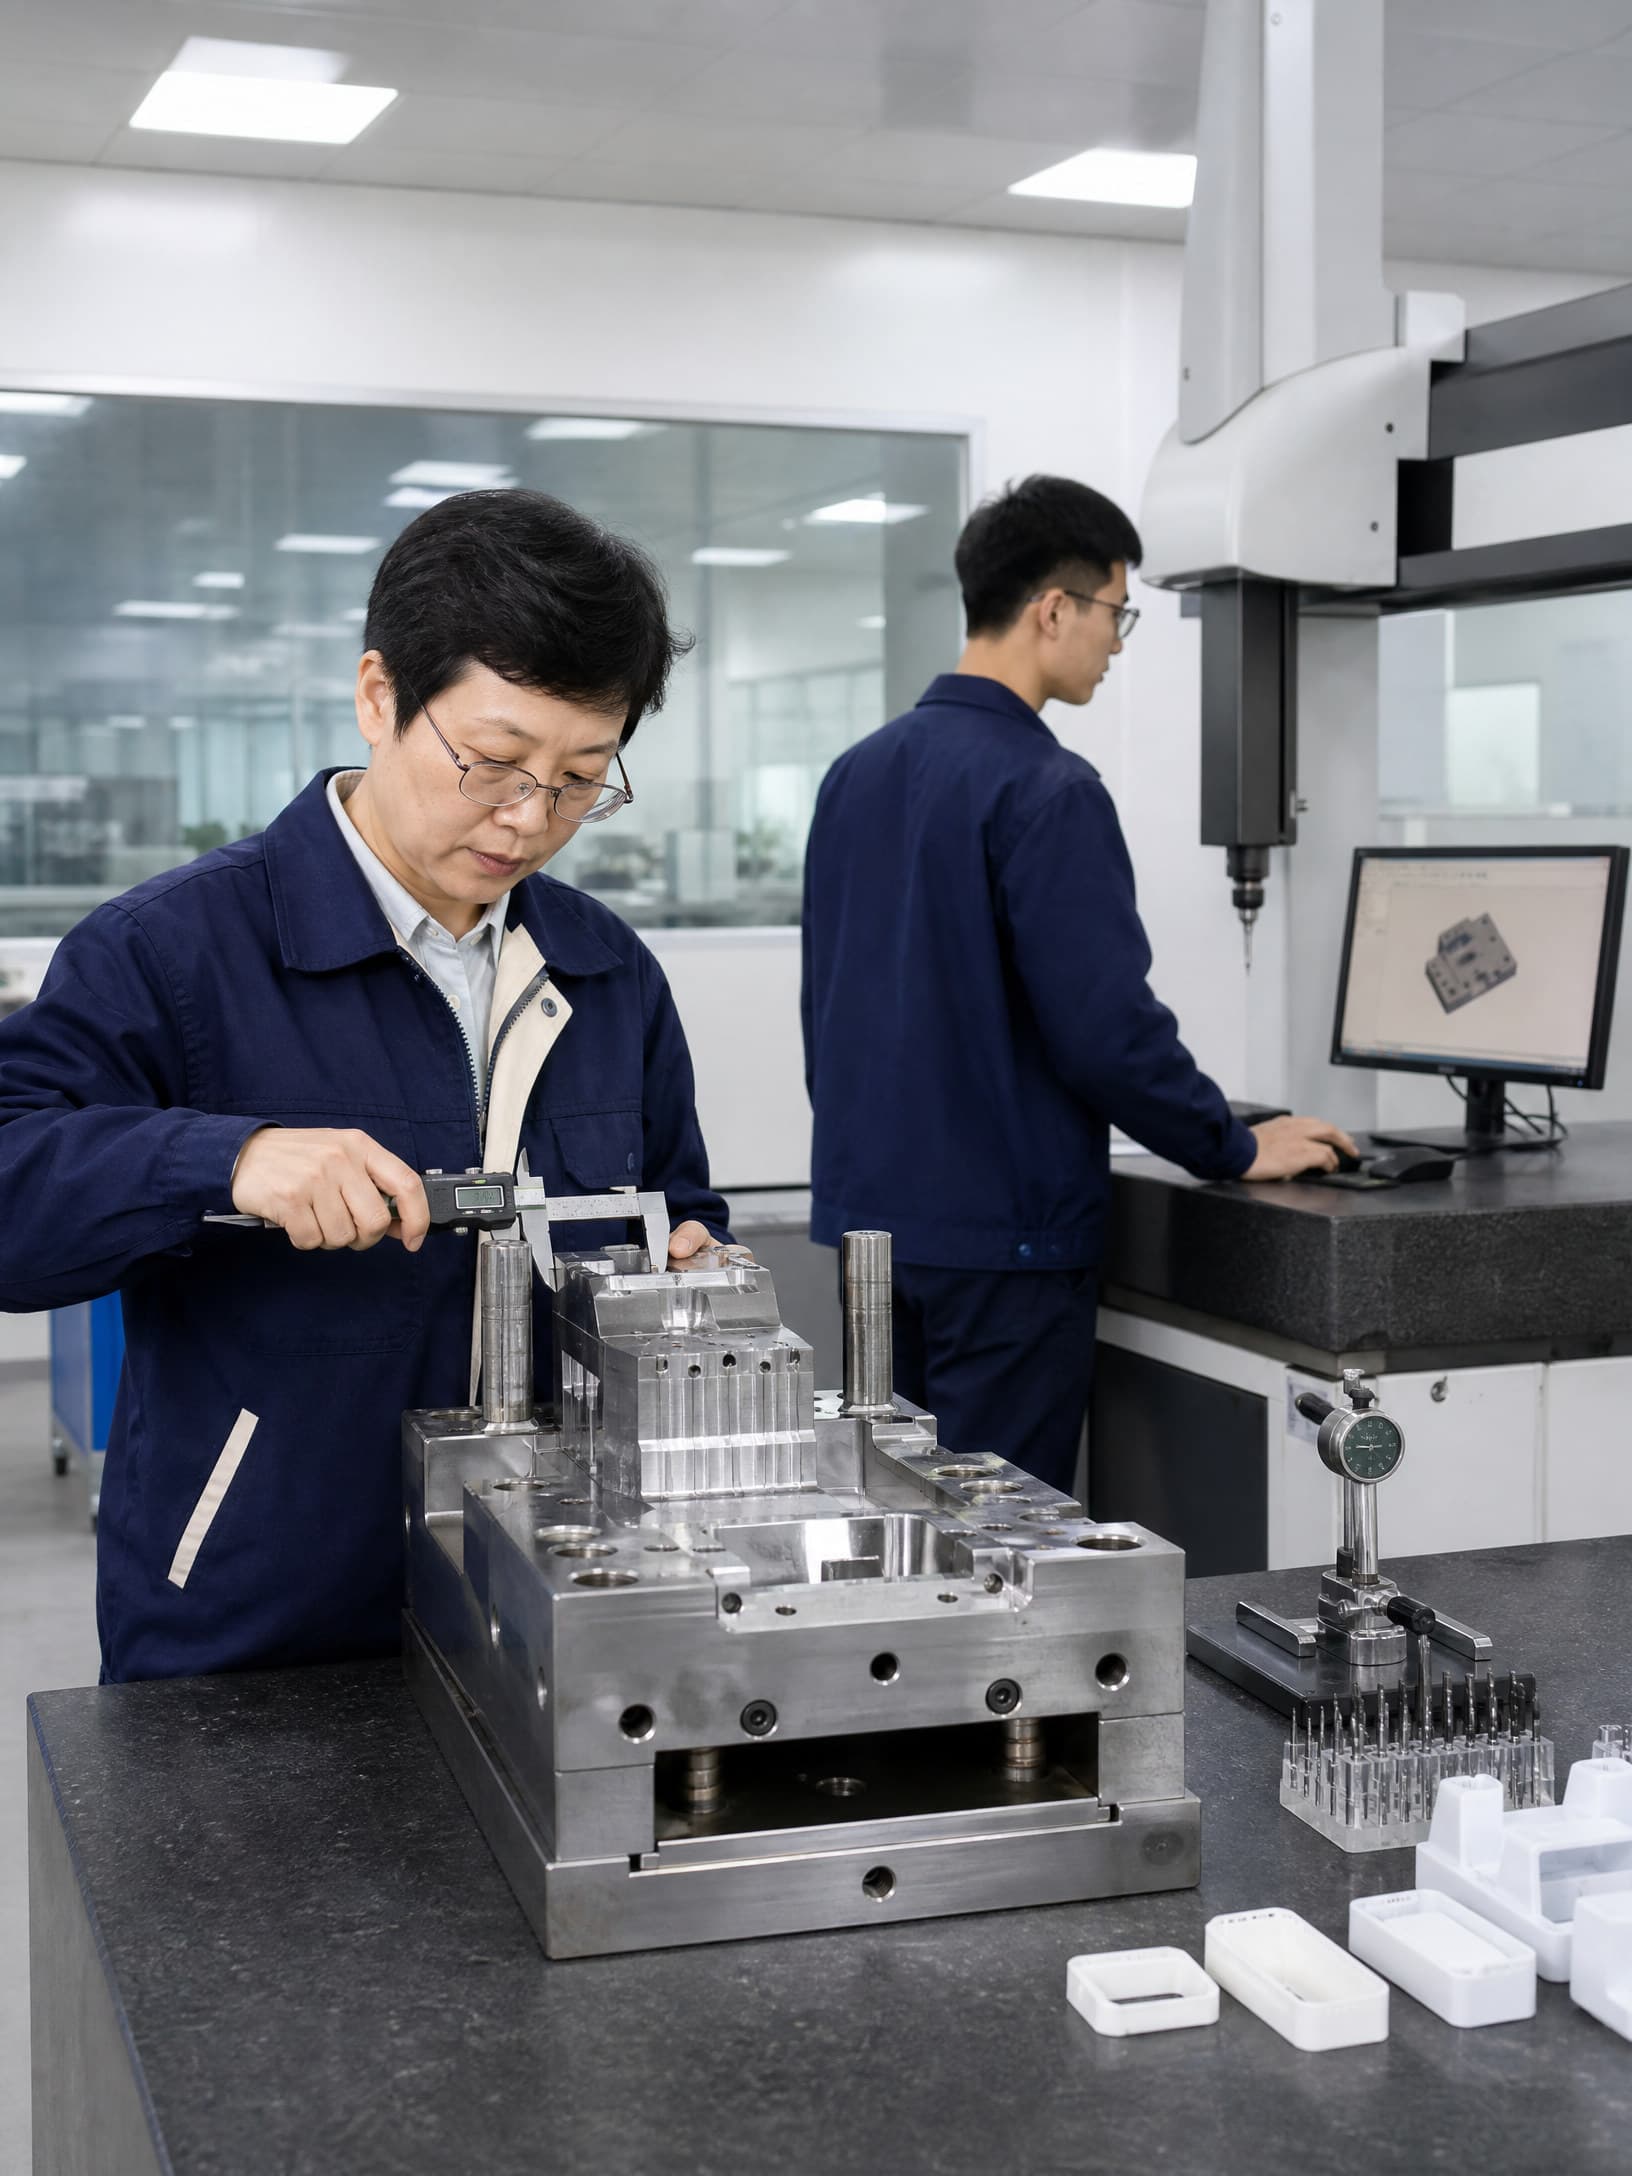
A useful FAI package lets a reviewer trace each result to the correct part, drawing revision, tool, cavity, material lot and inspection method. Ask for the controlled drawing or CAD revision, ballooned characteristic list, material and process identification, sample identification, dimensional results, functional or performance results where applicable, and a record of any nonconformance or approved deviation. For multi-cavity tools, make cavity identity visible rather than presenting an unlabelled mixed sample.
The report should show the requirement and the observed result together. A statement such as ‘meets drawing’ is weaker than a characteristic number, nominal, tolerance, measured value, unit, instrument or method, and pass/fail disposition. Confirm the measurement conditions that could affect polymer parts, such as conditioning, temperature, time after molding, fixture, datum scheme and measurement resolution. The buyer and supplier should agree those conditions before the inspection run, especially for dimensions affected by shrinkage or relaxation.
Ask how the supplier handles a result outside specification. The record should identify the affected characteristic, quantity, containment, root-cause or correction status, reinspection result and approval authority. A conditional release is not the same as full approval. Link the package to the supplier’s [quality](/quality) workflow and request a scoped [quote](/request-a-quote) that names the required samples and records instead of leaving documentation as an undefined extra.
| Evidence area | What to request | Buyer review question |
|---|---|---|
| Revision and identity | Part and drawing revision, tool and cavity, machine, resin grade and lot, sample IDs and inspection date. | Can every result be traced to the approved production configuration? |
| Dimensional FAI | Ballooned characteristic list, nominal and limits, measured values, units, datums, method and disposition. | Were the CTQs measured under the agreed conditions? |
| Material and function | Material certificate or agreed lot record, appearance results and functional or performance test results where specified. | Does the evidence cover what the part must do, not only its dimensions? |
| Deviation control | Nonconformance, containment, correction, concession or deviation approval, and verification evidence. | Is any open risk visible and formally accepted by the right owner? |
| Sample retention | Identified master or approval samples, photographs where useful, retention period and storage responsibility. | Can future disputes be compared with the approved reference? |
03
Make PPAP a connected production-control package
PPAP is not simply a larger dimensional report. AIAG describes its PPAP manual as ensuring engineering design and product specification requirements are met, within a wider set of quality core tools that includes APQP, control plans, FMEA, SPC and MSA [2]. For an injection-molded part, agree which elements are required, which may be summarized, and which are customer-specific. The supplier should be able to link the submitted records to the actual mold, machine, resin and control plan proposed for production.
Depending on the agreed scope, request the design record and change status, authorized engineering change documents, process flow, process FMEA or risk analysis, control plan, measurement-system evidence, dimensional results, material and performance tests, capability studies for designated characteristics, sample parts, master sample or visual standard, and the signed submission warrant or equivalent approval record. Do not demand sensitive supplier information without a reason; a controlled summary can be sufficient when it preserves the decision trail and agreed confidentiality.
Review the internal consistency. The CTQ in the drawing should appear in the risk analysis, control plan, inspection record and capability output. The machine and cavity in the trial record should match the production plan. A changed gate, resin, mold insert, inspection fixture or process window should have a documented impact review. Production approval should identify whether it is approved, approved with actions, rejected or pending customer decision, and should state who can release routine shipments.
04
Read capability studies with the data behind the index
Ask first whether the data represent a stable and reasonably understood process. NIST defines process capability as comparing the output of an in-control process with specification limits using capability indices [3]. A polished Cp or Cpk value without a run plan, time order, control evidence, sample identity and specification source is difficult to interpret. Request the raw or traceable data set, sampling interval, subgroup logic, cavity or machine separation, process settings, material lot, inspection method and any exclusions or rework treatment.
Cp describes spread relative to a two-sided specification; Cpk also reflects how close the process mean is to a specification limit. NIST notes that common capability-index assumptions include a suitable sample size and an approximately normal distribution, and that index estimates have uncertainty [3]. Therefore, do not impose a universal ‘pass’ number in a generic purchase order. Set the threshold, confidence approach, characteristic type and response to failure with the customer and supplier for the specific application.
Check whether the study is short-term or long-term and whether it covers all cavities, shifts, operators, material lots or machines that matter. A capability result can support launch approval without being a permanent guarantee. Use ongoing SPC, periodic dimensional checks, defect trends and reaction rules after release. If the process is not capable, ask for containment, correction, a revised study plan and an explicit decision about whether shipment is blocked, conditionally allowed or subject to sorting.
| Capability-study field | Evidence to request | Why it matters |
|---|---|---|
| Characteristic and limits | CTQ description, nominal, LSL/USL, target and drawing revision. | An index is meaningless without the correct specification basis. |
| Sampling plan | Part count, time order, subgroups, cavity or machine split, shifts and material lots. | Shows what production variation the study actually represents. |
| Measurement system | Gauge or CMM method, calibration status, resolution, fixture and MSA evidence where required. | Separates process variation from measurement variation. |
| Analysis | Raw values or traceable data, histogram or control chart, mean, standard deviation, Cp/Cpk or agreed alternative, and assumptions. | Lets the buyer assess stability, centering and uncertainty rather than trusting one number. |
| Reaction plan | Containment trigger, owner, disposition, correction and resampling or requalification rule. | Connects the study to an actionable production decision. |
05
Turn evidence into a signed production-release gate
Build a one-page approval matrix that names each required record, its revision, status, owner and due date. Include open deviations, missing tests, temporary controls, sample quantities, packaging and labeling, traceability, and the first shipment condition. A supplier’s quality certification may support confidence in the system, but it does not replace programme-specific evidence. Likewise, a successful first article does not automatically approve an unexamined production change.
Use clear dispositions: approved for routine production, approved with documented actions, limited release for a defined quantity or date, or not approved. For a limited release, identify the containment method and expiry trigger. Align the approval with the [injection molding process](/process), and specify when a new FAI, PPAP update, capability review or customer notification is required after a tool, material, machine, cavity, inspection method or process change.
Before placing an evidence-heavy order, send InjeForm the controlled part files, target volumes, CTQs, approval framework and destination requirements through the [request-a-quote](/request-a-quote) page. The objective is not the longest dossier. It is a reviewable chain from requirement to measurement to process control to authorized release, with uncertainty and responsibility visible to both buyer and supplier.
Practical takeaway
Before you move
to the next review.
- Define whether the programme requires FAI, PPAP, a capability study or a customer-specific combination before the approval run.
- Request revision-, tool-, cavity-, machine- and material-lot traceability for every submitted result.
- Require measurement methods, conditions, raw or traceable data, deviations and dispositions—not only summary pass statements.
- Review capability indices alongside stability, sampling, measurement-system evidence, assumptions and agreed thresholds.
- Record a signed production-release status with owners, open actions, containment limits and change-trigger rules.
FAQ
Common questions
Is FAI the same as PPAP?
No. FAI is a documented inspection of a representative first article against defined requirements. PPAP is a broader production-part approval package whose contents depend on the customer and agreed submission level. A programme may require one, both, or another customer-defined process.
What capability index should an injection molding supplier achieve?
There is no universal threshold for every part or industry. Agree the index, characteristic class, data conditions, confidence approach and reaction plan with the customer. NIST cautions that capability indices depend on process assumptions, sample size and specification limits.
Should capability data include every cavity?
Usually the study should represent the production configuration and the CTQ risk. For a multi-cavity tool, ask the supplier to explain cavity sampling and whether cavity-level results are needed. A pooled result can hide a weak cavity.
Can a supplier use inspection data from trial parts for production approval?
Only if the agreed approval plan accepts that evidence and the trial conditions represent the intended production process. Identify the machine, tool, resin, settings, cavity, quantity and any differences from routine production.
What happens when an FAI or capability result fails?
The supplier should contain affected parts, identify the characteristic or source of variation, document correction and recheck the result. The buyer then decides whether to reject, request requalification, accept a defined deviation or permit a limited release under written authority.
References
Source material
- [1] IAQG, ‘9102 First Article Inspection Requirement.’
- [2] AIAG, ‘Quality Core Tools.’
- [3] NIST/SEMATECH e-Handbook of Statistical Methods, ‘What is Process Capability?’
- [4] NIST/SEMATECH e-Handbook of Statistical Methods, ‘Assessing Process Capability.’
- [5] U.S. Food and Drug Administration, ‘Process Validation: General Principles and Practices.’
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.