
An injection molding first-article inspection (FAI) gives a buyer evidence about a defined part made from a defined tool, material direction and process context. It is useful when the team needs to decide whether a new or changed mold, cavity, resin grade, supplier or production route is ready for the next gate. It is not automatically a certificate of every future production part, a substitute for process control or proof of product-level performance. The scope and approval authority should be agreed in the purchase or quality documents before samples are made.
Start with the released drawing, CAD revision, material and colour direction, appearance references, mating-part assumptions and application risks. Then identify the characteristics that can prevent assembly, sealing, locating, operation, safety or acceptable appearance. Ask the supplier to map those requirements to sample identification, measurement method, result, acceptance limit and disposition. A clear FAI package helps procurement, engineering and quality review the same decision rather than debating an unexplained pass statement.
Do not approve an FAI because every cell is filled in. Approve it only when the sample identity, released definition, measurement method, results and deviations support the specific release decision.
01
1. Define what the injection molding FAI is meant to prove
Before requesting an FAI inspection report, define the decision it must support. A first article may confirm that a new tool produces a part against the current drawing, that a transferred mold still meets the definition, or that a material, cavity, supplier or major process change needs review. Those cases can require different samples, tests and approval owners. A first-article report should not silently become a guarantee of ongoing capability or a replacement for a product qualification plan.
Separate the part-level FAI from related evidence. Dimensional inspection addresses measured characteristics under stated conditions. Material documentation addresses the resin and any agreed traceability. Functional, leak, torque, assembly, pressure, electrical or environmental tests address use-related risks where required. Process validation, capability studies and routine control plans answer different questions. Reference each requested evidence item to the requirement and state whether it is mandatory for release, informative, or to follow at a later gate.
For a new tool, ask whether the samples are from the intended production tool and named resin, and whether all cavities are represented when cavity variation matters. If the sample is from a prototype tool, a hand-trimmed part or a substitute resin, label that limitation clearly. A useful FAI begins with sample status rather than allowing an attractive report to obscure how the part was made.
02
2. Build the inspection scope from the released definition
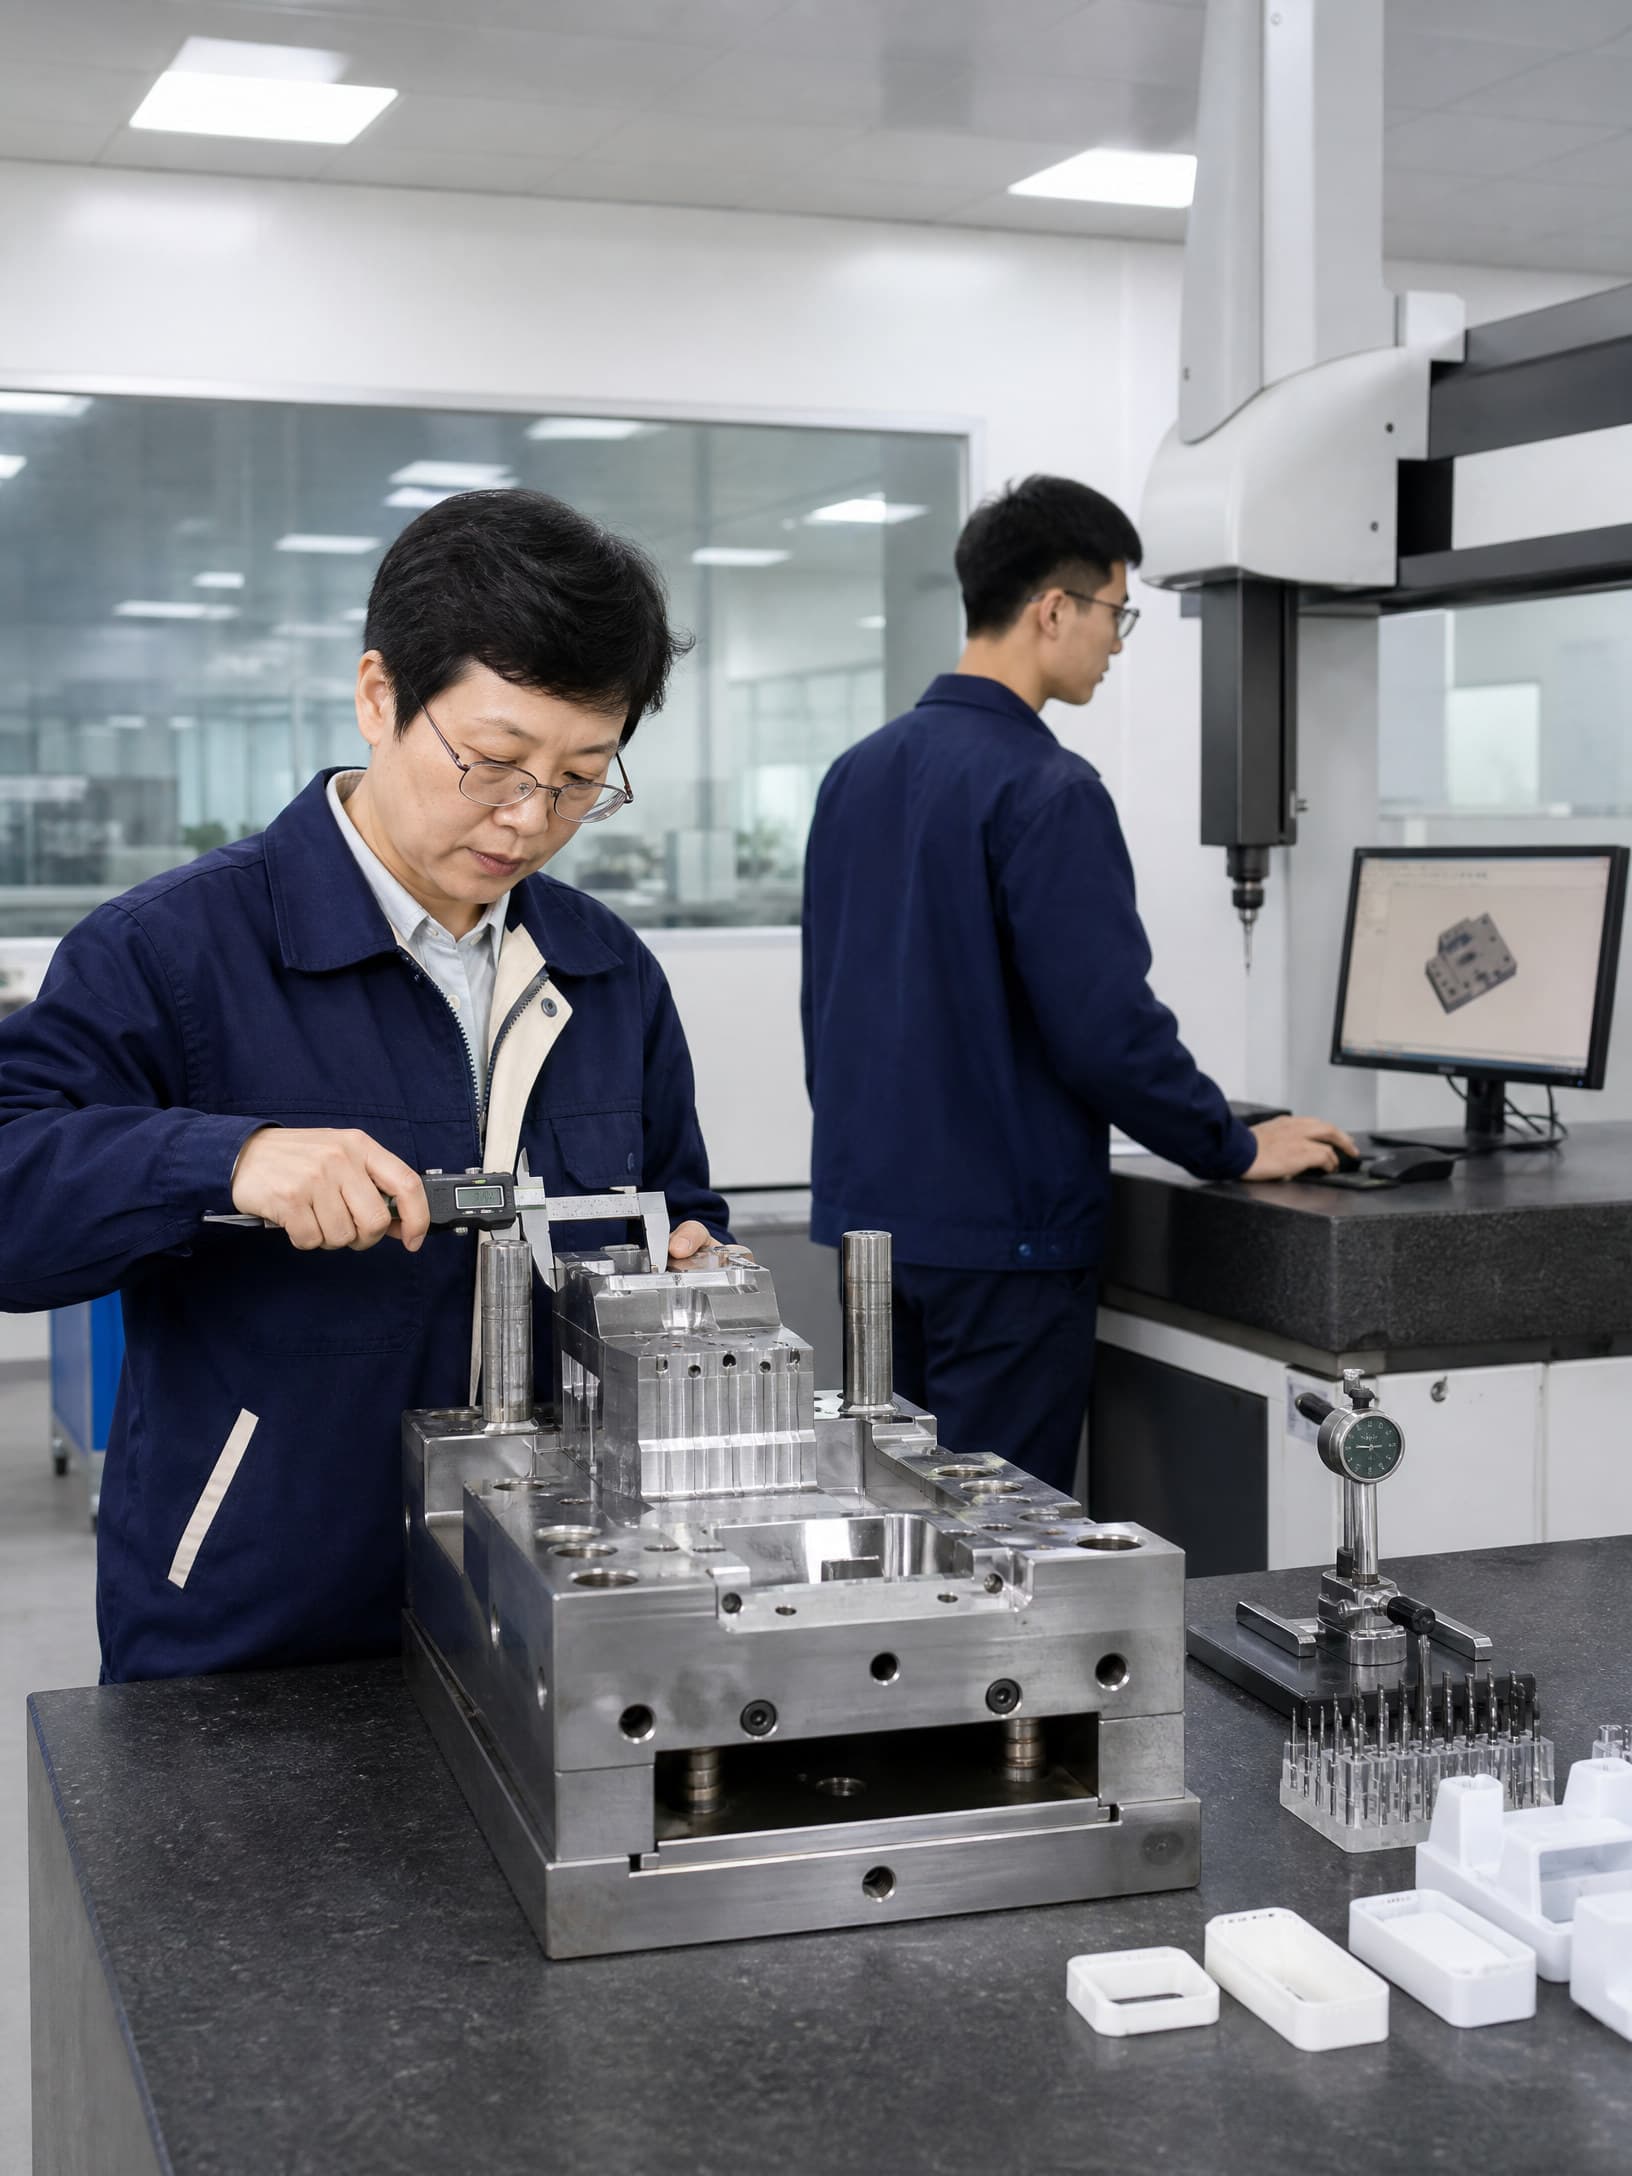
Use the current drawing revision and controlled CAD as the inspection baseline. Include general tolerances, GD&T, datums, material, colour, inserts, threads, marking, appearance zones and any approved boundary samples. Identify critical-to-function characteristics separately from ordinary dimensions so the reviewer can see which results could block assembly or service. ISO 20457 describes tolerances and acceptance conditions for plastics moulded parts, but the buyer and supplier still need to agree the part-specific requirements and conditions.
A characteristic list should give each item a traceable identifier: balloon or item number, drawing note, datum feature or model reference. Record nominal, lower and upper limits, unit, result, method and status. Where a requirement is visual, define the lighting, viewing distance, comparison standard and permitted location as far as the application needs. Where a feature is flexible or temperature-sensitive, state free-state or fixtured condition, conditioning time and measurement force.
Avoid treating every drawing line as equally important. Overly broad reporting can bury a seal diameter, locating boss, shutoff edge or connector interface among low-risk dimensions. A focused characteristic set is easier to review, but omitted requirements must be an intentional decision recorded by the accountable engineering or quality owner.
| FAI evidence block | What it should answer | Buyer review question |
|---|---|---|
| Part and sample identity | Which part revision, cavity, lot, tool and manufacturing date were inspected? | Can I trace the reported results to the actual production-intent samples? |
| Dimensional results | Do the measured characteristics meet the released limits under the stated method and condition? | Are datums, units, tolerances, method and out-of-tolerance results unambiguous? |
| Material and process context | What resin grade, colour/additive basis and relevant process state produced the samples? | Is this the approved material and is any substitution or regrind direction disclosed? |
| Visual and functional checks | Do appearance, fit or use-related requirements meet the agreed criteria? | Are visual standards and functional tests defined rather than implied by dimensional pass results? |
| Deviation and disposition | What does not meet the baseline, and who accepted the risk or required correction? | Is there a linked concession, containment action, rework decision or open corrective action? |
| Approval record | Who reviewed the evidence and what gate does the decision release? | Does the signature or approval state identify scope, date, revision and remaining conditions? |
03
3. Make measurement evidence defensible
An FAI result is only as useful as the method behind it. Request the instrument or gauge type when it affects interpretation, along with fixture, datum strategy, measurement force, part condition and sampling detail. A CMM may be appropriate for positional relationships and profiles, while optical equipment, gauges or controlled functional fixtures may be better for other features. NIST notes that measurement equipment selection is part of inspection planning; buyers should seek a method matched to the requirement rather than impose one device for every characteristic.
Flexible molded parts can deflect under a probe, and parts can change dimension after molding, conditioning or assembly. State whether dimensions are taken at a defined time after molding, at room condition, after conditioning or in an assembled state. For cosmetic acceptance, include the agreed visual reference and inspection environment. If a result is near a limit, ask whether method variation or uncertainty could change the disposition and whether a second method or review is warranted.
For multi-cavity tools, identify cavity and sample count. A single composite result can conceal cavity-to-cavity differences. The right amount of coverage depends on risk, tool architecture and the agreed plan, but the report should never imply all cavities were proven when only one was measured.
04
4. Review failures, concessions and change impact
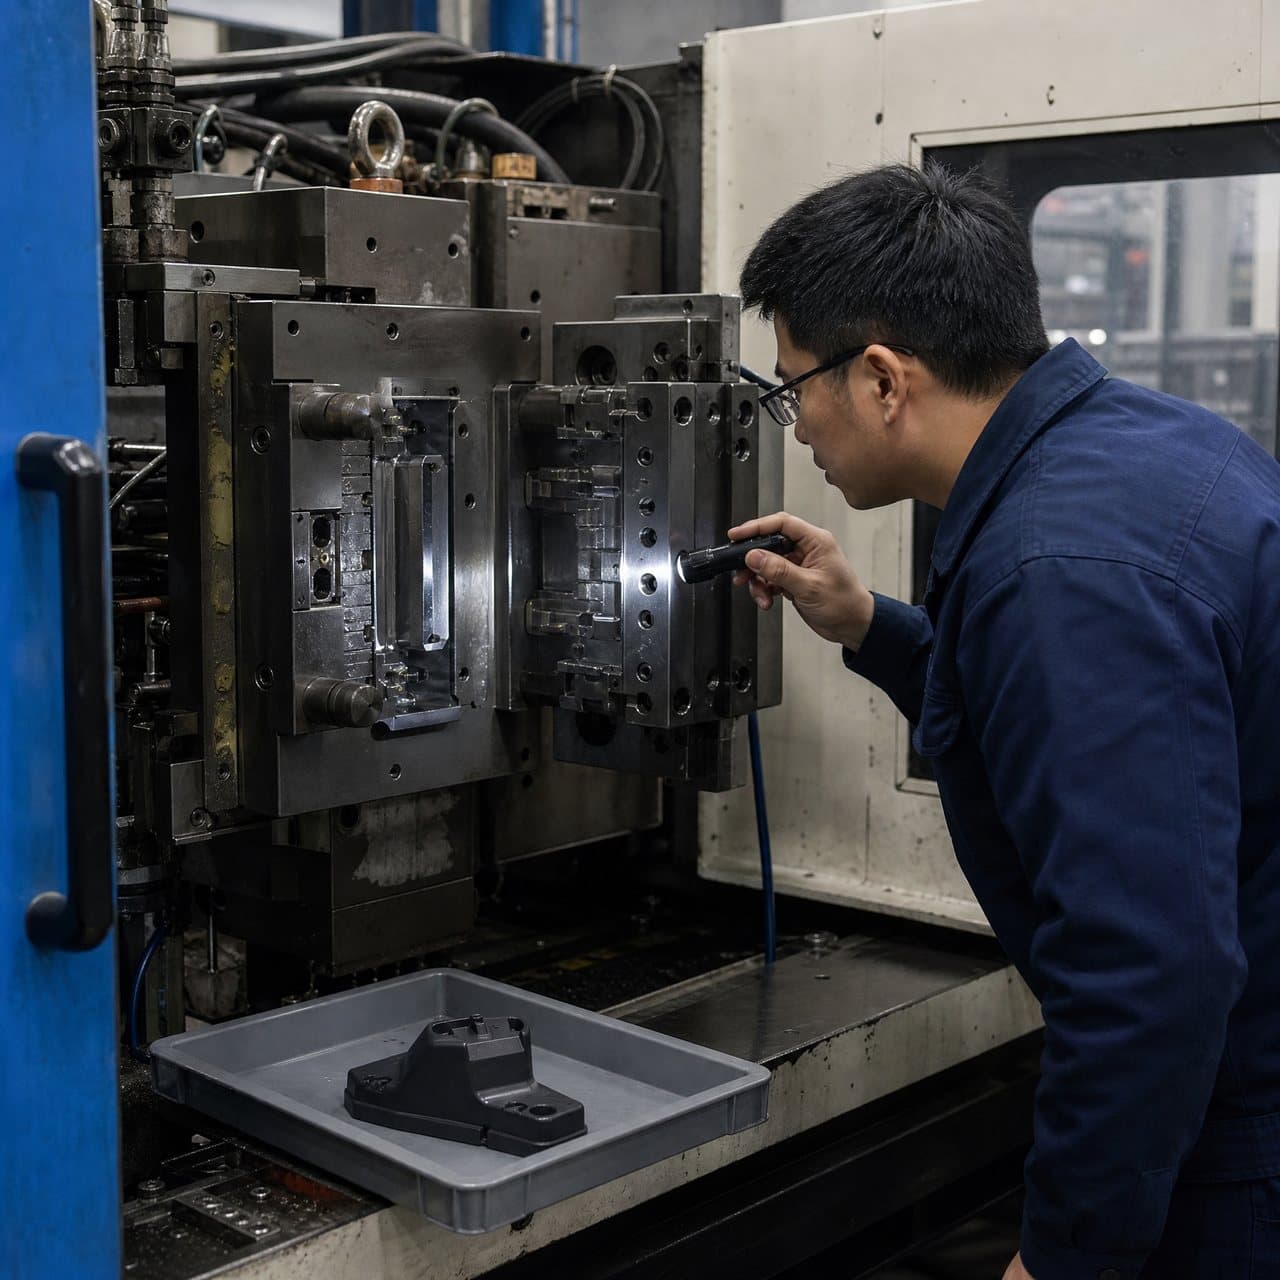
An FAI with an out-of-tolerance result is not necessarily useless, and a report with no recorded deviation is not automatically reliable. First determine whether the result is real: confirm part identity, drawing revision, method, datum, unit, instrument and repeatability. Then classify the issue as a drawing interpretation problem, tool condition, molding variation, material effect, measurement issue, cosmetic difference or functional risk. Keep the original result visible; do not replace it with a corrected value without an audit trail.
A concession should identify the exact characteristic, affected quantity or sample, risk assessment, temporary or permanent duration, containment, corrective action and approving authority. Commercial acceptance does not automatically mean engineering acceptance. If a tool correction, resin change, gate alteration, process-window change or design revision follows, decide whether a partial or full re-FAI is needed. The answer should be written before the change is released.
Treat FAI as one gate in change control. A passed first article does not authorize an unreported material substitution, cavity repair, tooling modification or supplier transfer. Link the report to the relevant change record and define what event triggers renewed inspection. This protects both parties from relying on a document whose original assumptions no longer apply.
05
5. Connect first-article approval to production readiness
After the FAI review, agree what is released and what remains open. The decision may be approved, conditionally approved with named actions, rejected pending correction, or accepted only for a limited trial. Record the applicable part and tool revisions, cavities or samples covered, open risks, owner and due date. Do not use a generic ‘approved’ stamp if production is restricted by a pending functional test or an accepted cosmetic deviation.
Routine production control should then take over the risks that the FAI cannot prove. Agree start-up checks, in-process or lot checks, reaction rules, material traceability and change notification according to the application. ISO 2859-1 can provide a sampling framework for attribute inspection, but an AQL-style plan does not prove every unit conforms and should not replace a suitable measurement method or functional test. Sampling, frequency and lot definition belong in the part-specific quality agreement.
For a practical handoff, request a compact evidence matrix: requirement, source revision, characteristic or test, method, sample identity, result, disposition, owner and next gate. If the programme needs an automotive-style submission, medical-device validation or customer-specific format, name that obligation explicitly rather than assuming that the word FAI has one universal meaning. Buyers can use InjeForm’s process overview to align DFM, tooling, trial and production discussions, then send the drawing, CAD, material direction and acceptance questions through the quote route.
Practical takeaway
Before you move
to the next review.
- Freeze the part number, drawing and CAD revision, material and colour direction, appearance references, mating parts and the approval decision the FAI must support.
- Identify function-critical, assembly-critical and cosmetic characteristics, and link each to a nominal, limit, method, datum or visual standard where applicable.
- Require sample identity, tool and cavity coverage, manufacturing date or lot, resin grade, process context and any limitation such as prototype tooling or substitute material.
- Review measurement method, fixture, part condition, instrument context, units and raw or reported results before treating a pass statement as evidence.
- Record every deviation, concession, containment action, corrective owner and re-FAI trigger; never hide an out-of-tolerance result by overwriting the original record.
- Define the release state and handoff to routine inspection, process control, material traceability and change notification, with open actions assigned to named owners.
FAQ
Common questions
What does FAI mean in injection molding?
FAI usually means first-article inspection: a documented review of a defined sample made under stated tool, material and process conditions against a released part definition. The exact report format and approval scope are not universal, so the buyer and supplier should define them in the quality or purchase documents.
Is an injection molding FAI the same as a T1 sample approval?
Not necessarily. A T1 sample often refers to an early mold trial and its sample review, while an FAI is an evidence package tied to specified requirements and an approval decision. A T1 sample can be used for FAI only when its tool, material, process context, sample identity and inspection scope meet the agreed release basis.
How many parts are needed for an injection molding FAI?
There is no universal quantity. The required number depends on cavity count, characteristic risk, variation, functional testing, customer requirements and whether the goal is dimensional confirmation or broader qualification. State the sample size and cavity or lot coverage before inspection; do not infer that one part proves every cavity or future production run.
Can a buyer approve an FAI with deviations?
A buyer may approve a limited or conditional release only when the deviation is visible, risk-assessed, bounded and accepted by the appropriate authority. The record should identify the affected characteristic, quantity, containment, corrective action, expiry or re-FAI trigger. Commercial urgency alone is not a technical disposition.
What should be included in an injection molding FAI report?
At minimum, request the part and revision, sample or lot identity, tool and cavity context, characteristic list, nominal and limits, measured results, units, method or condition where material, visual or functional evidence where required, material context, deviations, disposition and approval record. Add raw data, photos, capability or validation evidence when the programme specifically requires it.
References
Source material
- [1] ISO, ‘ISO 20457: Plastics moulded parts — Tolerances and acceptance conditions.’
- [2] ISO, ‘ISO 2859-1: Sampling procedures for inspection by attributes.’
- [3] National Institute of Standards and Technology, ‘Rule Model for Selecting Dimensional Measurement Equipment in Inspection Planning.’
- [4] Automotive Industry Action Group, ‘Quality Core Tools.’
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.