
A first article inspection (FAI) package should let a buyer connect a physical molded part to the released product definition and a known manufacturing condition. For an injection-molding programme, that means more than a spreadsheet of dimensions. The package should identify the part and mold revision, the cavity or cavities represented, the approved resin condition, the trial or production condition, the measurement approach, the actual results, and any departures from the requirement. It gives engineering, quality, procurement, and supplier-management teams a shared basis for a controlled approval decision before routine supply or a defined next stage of the programme.
A requirement is binding only when it is stated in the drawing, CAD model, purchase order, quality agreement, customer-specific requirement, applicable market rule, or an accepted deviation. A request for a ballooned drawing, photographs, cavity-coded results, or a gauge study is normally a recommendation unless those documents are made contractual. The right FAI scope depends on resin, geometry, tolerance and datum scheme, tool architecture, cavity count, molding machine, downstream operations, intended market, and contract terms. It should not be treated as a universal promise of future mold life, dimensional capability, cycle time, certification, or product compliance.
Approve the controlled part and the evidence conditions together: a result without its drawing revision, datum strategy, cavity identity, resin, measurement method, and deviation status is not a reliable release record.
01
1. Define what the FAI must approve before samples are measured
Begin with a written FAI plan that says what decision the package supports: tool-trial learning, first-off approval, production-intent release, a customer submission, or re-approval after a change. Define who supplies the controlled technical baseline and who has authority to approve, reject, or grant a time-limited deviation. A supplier may prepare the report, but a buyer should not allow it to substitute an unreleased drawing, unresolved CAD conflict, or undefined visual and functional requirement. If the customer invokes an aerospace, automotive, medical, or other sector process, state the applicable edition, submission level, and customer-specific rules rather than calling every report an equivalent FAI. IAQG 9102 is a standardized FAI process developed principally for aviation, space, and defense; it is not an automatic requirement for general industrial molded parts [1].
Issue a frozen input list before the run. At minimum, include the approved part number and revision; drawing or model and any GD&T convention; material grade, supplier, color and additive restrictions; approved mold and cavity configuration; inserts, overmolding, assembly, finishing, packaging, and test requirements; critical characteristics; visual reference; sampling plan; and the required report format. Mark which items are contractual requirements and which are buyer recommendations. When a dimension is unclear, when datum logic is missing, or when a functional interface has no acceptance method, resolve it by engineering change or documented clarification before asking the supplier to measure it. ASME Y14.5 provides a common language for communicating and interpreting GD&T, but the released product definition remains the acceptance basis [4].
Ask the supplier to declare the article condition in the cover sheet. The declaration should distinguish a tool tryout from a production-intent run and identify all temporary conditions, such as reduced cavity use, hand trimming, a development fixture, nonstandard material preparation, or manual handling. Those conditions do not automatically invalidate an FAI, but they determine what the evidence can support. For multi-cavity tools, agree whether approval is by tool overall, by cavity, by family-member configuration, or by a defined representative selection.

02
2. Request a ballooned drawing and traceable report, not an unlinked data file
A buyer should request a ballooned drawing or controlled model-based characteristic list that assigns a unique identifier to every required dimensional, geometrical, material, visual, marking, assembly, and functional requirement within the agreed FAI scope. The inspection report should repeat that identifier and show the nominal, tolerance or limit, unit, actual result, inspection method, result status, and report page or record reference. This traceability prevents a favourable measurement from being disconnected from the feature, datum, revision, or acceptance rule it is supposed to support.
Do not assume that every nominal drawing dimension deserves identical reporting depth. The buyer should require the characteristics stated by the submission requirement and add a risk-based focus on locating features, sealing and mating interfaces, threads, insert locations, snap fits, wall-sensitive geometry, appearance zones, material or color requirements, and product-specific functional checks. For a feature controlled by GD&T, request the feature-control-frame interpretation, datum reference scheme, fixture or alignment strategy, and any applicable material-boundary or modifier treatment. A list of X-Y-Z points is not automatically evidence that a positional, profile, or runout requirement was evaluated correctly.
The FAI report should also make omissions visible. Require a clear notation for not applicable, not measured, pending, reworked, or out-of-tolerance results; never accept blank cells as implied pass results. Link every nonconformance to a disposition number, containment status, corrective-action owner, and the person authorized to accept the deviation. If a part is accepted conditionally, write the quantity, lot, cavity, time limit, affected requirement, and re-submission trigger into the approval record.
03
3. Check whether dimensional results are credible and comparable
Read a reported value together with its measurement context. The supplier should identify the instrument or gauge, program and revision where relevant, calibration or metrological-confirmation status, resolution, fixture, operator or automated method, datum alignment, part condition, environment when material to the result, and sampling quantity. ISO 10012 describes measurement-management requirements intended to create confidence in valid and reliable results; a calibration certificate alone does not prove that a selected setup, fixture, program, or resolution is fit for a particular molded feature [3].
For polymer parts, record the state in which the part was measured. Resin, reinforcement, moisture condition, post-mold conditioning, elapsed time after molding, temperature, warpage restraint, and secondary processes can all influence an observed dimension. The buyer should specify or agree the conditioning and timing rule for features where this can matter, then compare supplier results under the same rule. Do not compare a supplier's warm, unconstrained sample to an incoming inspection result from a conditioned part without investigating the difference.
When comparing bids, sites, cavities, or repeat submissions, use the same released requirement and decision logic. Demand cavity-coded data where a multi-cavity tool or risk assessment warrants it; aggregate results can mask an unfavorable cavity. For tight or disputed features, request a proportionate measurement-system study, correlation plan, or repeat measurement rather than accepting a bare assertion of accuracy. NIST notes that gauge repeatability and reproducibility studies address errors affecting production measurement, including repeatability, reproducibility, stability, bias, resolution, linearity, and drift [3].
| Report element | What the buyer should check or request | Approval point |
|---|---|---|
| Controlled baseline | Part number, drawing or model revision, revision date, GD&T convention, approved material and process route, mold ID, cavity map, and sample quantity. | Approve only when the report and physical samples are traceable to the intended released configuration. |
| Characteristic traceability | Balloon number or model characteristic ID, requirement, nominal and limits, unit, actual values, inspection method, result status, and source record. | Confirm every required characteristic is accounted for and that blank fields do not conceal missing evidence. |
| Measurement basis | Gauge or CMM identity, program or fixture revision, calibration or confirmation status, resolution, datum setup, part condition, and any relevant environment or conditioning rule. | Accept results only when the method can support the specified feature and the setup matches the product definition. |
| Molding and tool context | Resin manufacturer, grade, lot or traceability as agreed, color or additive condition, machine, mold revision, cavity identification, process state, and disclosed temporary conditions. | Determine whether the evidence supports trial learning, production-intent approval, or a limited conditional release. |
| Exceptions and disposition | Out-of-specification or pending result, deviation number, containment, quantity and cavity affected, corrective action, re-inspection, and approval authority. | Approve, reject, or conditionally release each exception in writing; do not infer acceptance from shipment or silence. |

04
4. Review tool and part evidence as one decision package
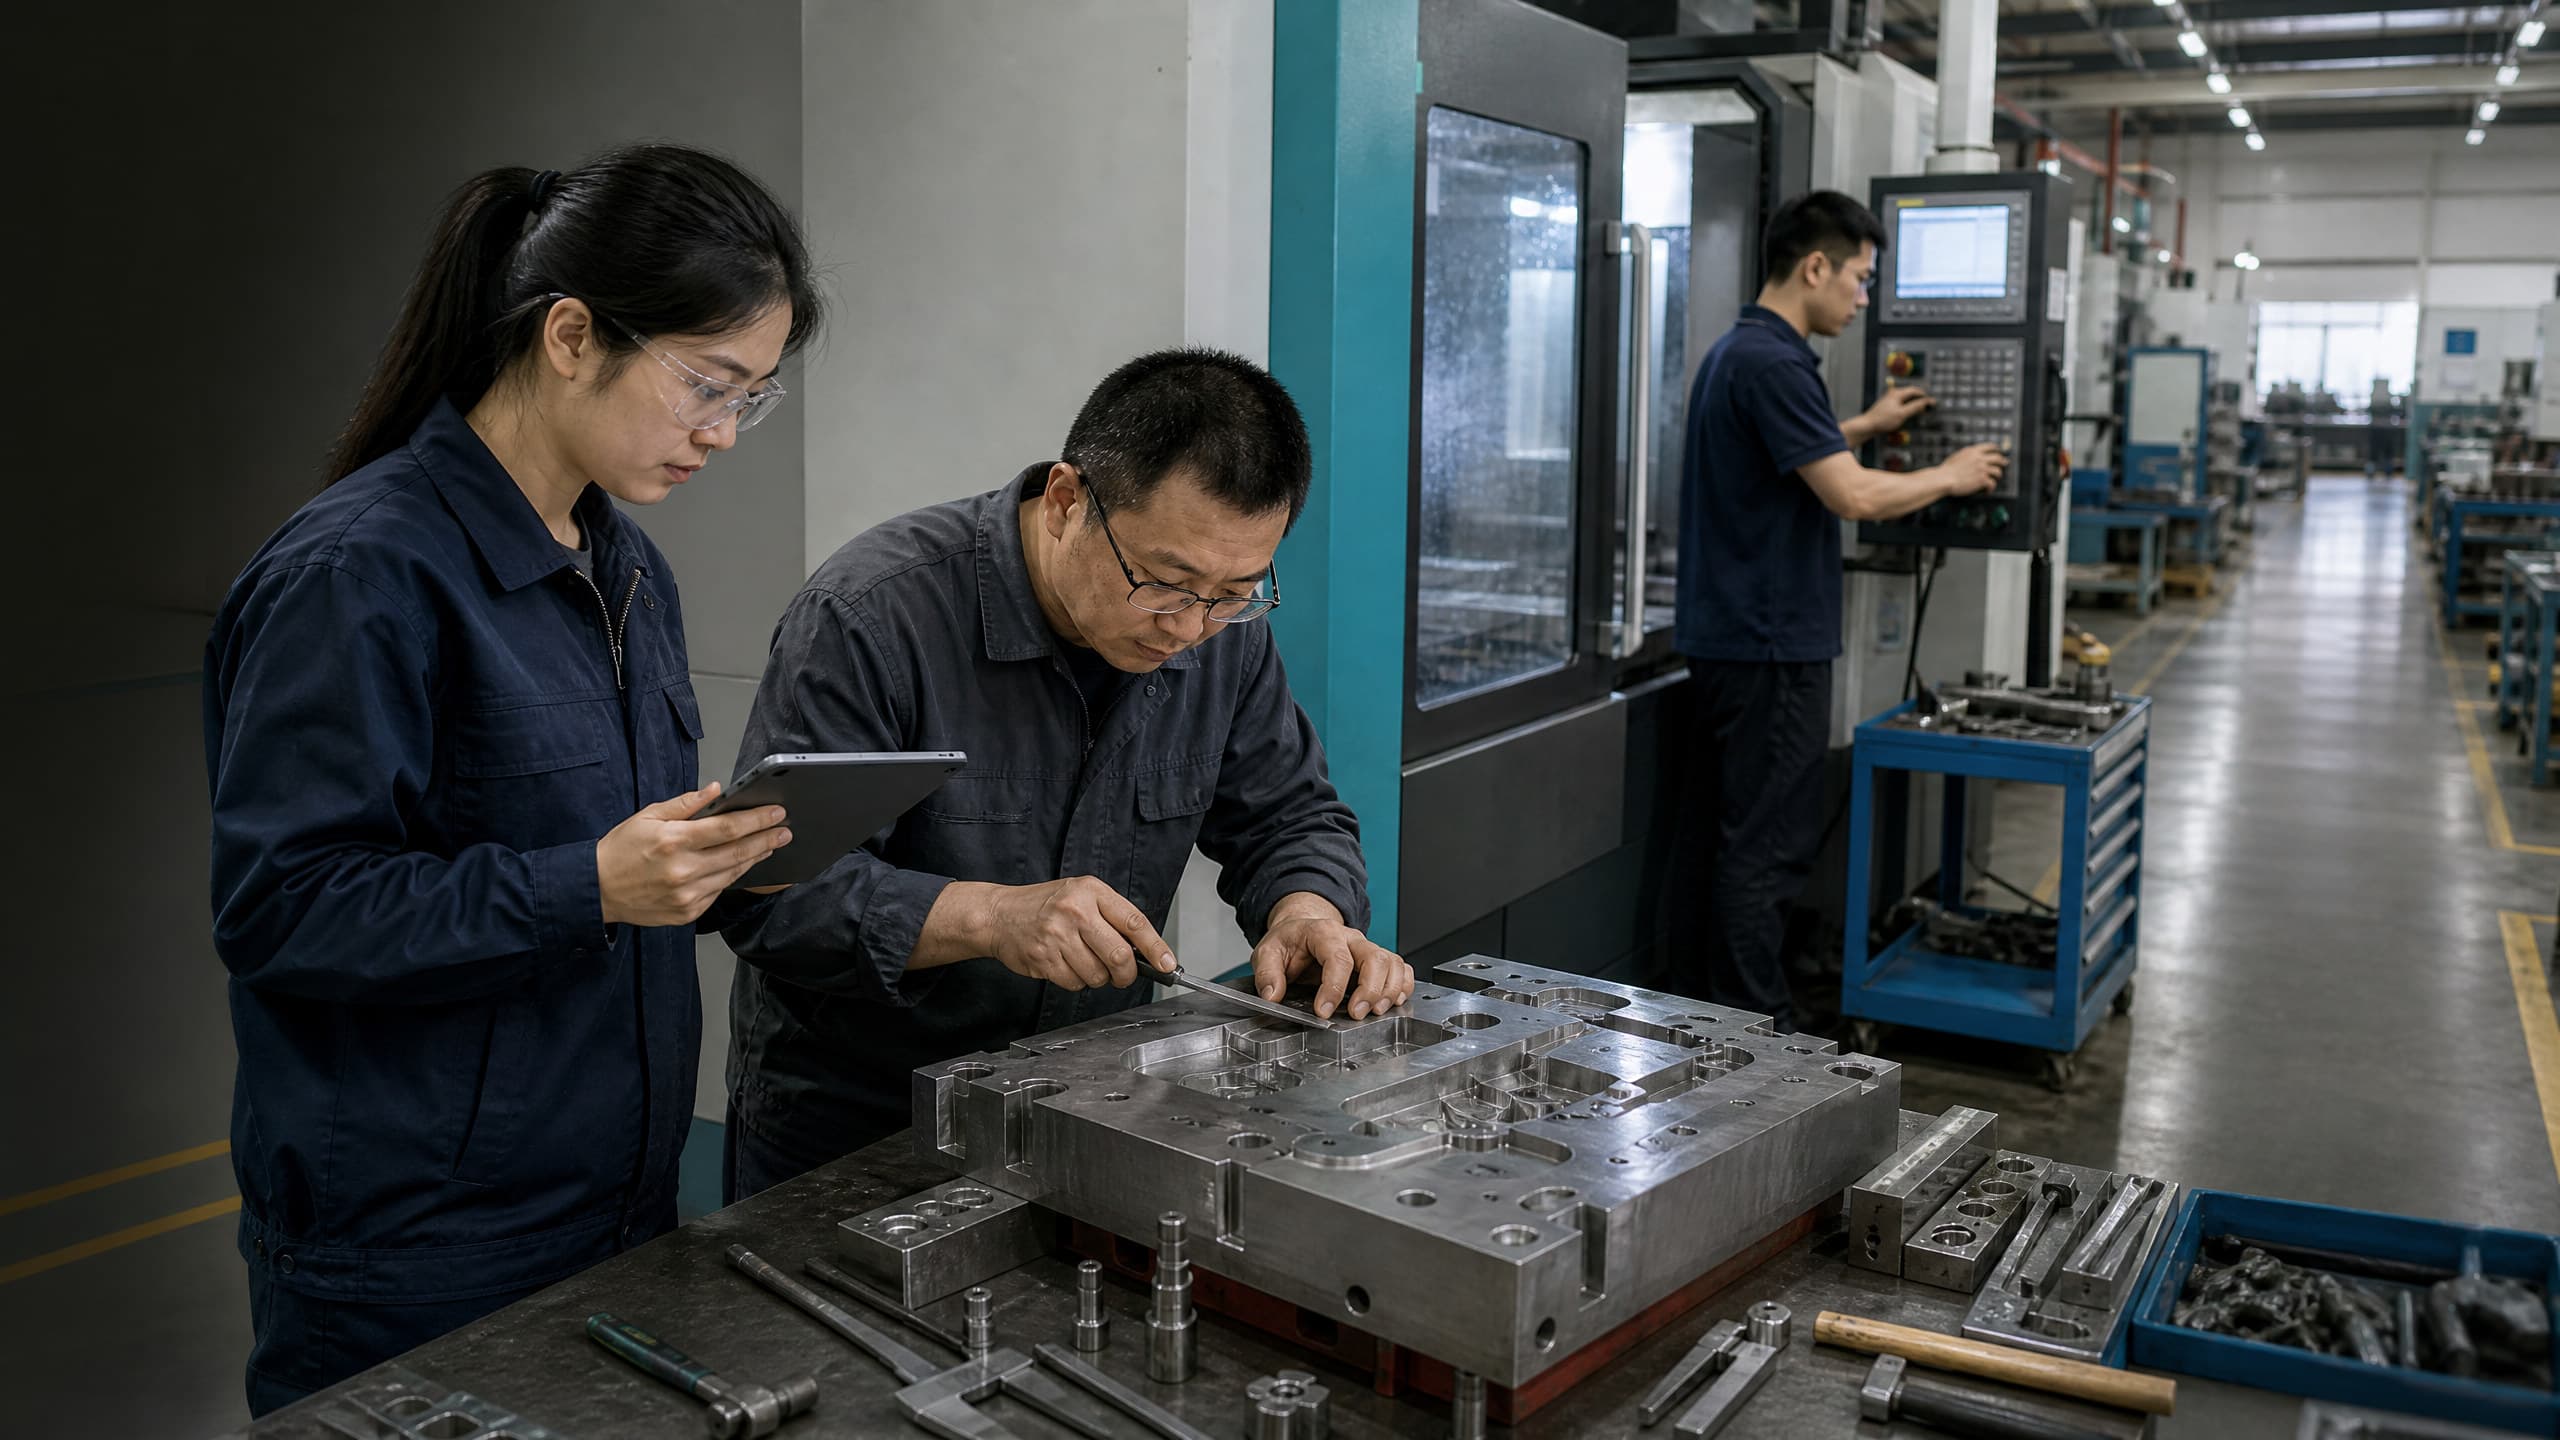
A molded-part FAI should be read with the tool and trial record when the approval concerns a new or modified injection mold. Request the mold ID and revision, cavity and core identification, gate and runner configuration where relevant, insert or slider configuration, tool maintenance or repair disclosure, and a description of any change made after the samples were molded. The objective is traceability, not a demand that a supplier disclose every proprietary construction detail. A tool change, cavity repair, gate revision, hot-runner adjustment, changed insert, or different downstream trimming route can affect the relevance of earlier results and should be reviewed through agreed change control.
Ask for evidence that matches the part's actual risks. Dimensional results may need to be complemented by photographs under an agreed viewing condition, mass data, material identification, leak or pressure checks, assembly or fit checks, torque or retention tests, color or surface reference comparisons, marking verification, or packaging checks. A passing dimensional report is not by itself proof of functional performance, cosmetic acceptability, regulatory status, or long-term durability. Conversely, a visually acceptable sample does not prove all drawing requirements were met.
Separate technical findings from commercial release. Engineering may accept a temporary dimensional deviation for a defined build while procurement holds a purchase-order release until corrective evidence arrives. Record the exact decision, scope, owners, dates, and notification route. If an automotive programme requires PPAP, use its stated submission requirements: AIAG describes PPAP as a process for demonstrating that engineering design-record and specification requirements are consistently met during an actual production run at production rates [2]. A general FAI can contribute evidence, but it should not be represented as a complete PPAP unless the required package and conditions have been met.
05
5. Set written acceptance gates and re-submission triggers
Use explicit gates instead of a single broad statement such as 'FAI approved.' Before sampling, approve the drawing baseline, report plan, critical-characteristic list, measurement approach, material and trial conditions, and functional or visual methods. At report review, verify characteristic completeness, sample identification, measurement context, actual results, and exception status. At release, issue one of four written outcomes: approved; approved with defined conditions; rejected pending correction; or accepted only under a numbered deviation. State whether the outcome authorizes another trial, pilot build, routine production, shipment, or no further activity.
The approval record should say what must happen after a conditional approval. Examples include tool correction, cavity-specific containment, additional samples, correlated measurement, updated photographs, a revised FAI, a production-intent confirmation, or customer sign-off. Assign the buyer approver, supplier owner, required evidence, deadline, and change to the drawing, tool, process, or records. Approval should never rely solely on email language that leaves the affected part revision, quantity, and expiry undefined.
Agree re-submission triggers in the quality agreement or project plan. Potential triggers can include a drawing or CAD revision; change of resin grade, source, colorant, or additive restriction; tool repair or geometry change; cavity addition, replacement, or reactivation; gate or hot-runner change; machine or process-route change; new fixture or inspection program; a nonconformance trend; or a lapse in production that the parties define. The appropriate evidence after each change is risk-based. It may be a focused remeasurement, a new cavity study, functional retest, or a complete resubmission; neither a full FAI nor no review is universally correct.
Practical takeaway
Before you move
to the next review.
- Require a controlled FAI plan that identifies the release decision, product definition, material and tool configuration, sample condition, required evidence, and named approval authorities.
- Request a ballooned drawing or model characteristic list linked one-to-one to actual results, measurement methods, units, status, and any exception record.
- Verify measurement context for risk-critical features: datum and fixture strategy, instrument or program identity, calibration or confirmation status, resolution, part conditioning, and cavity identification where relevant.
- Compare supplier submissions only when they use the same released revision, resin and process basis, characteristic list, sampling logic, measurement rule, and exception disposition standard.
- Approve in writing as approved, conditionally approved, rejected, or deviation-only, and define re-submission triggers for material, tool, cavity, process, inspection-method, or design changes.
FAQ
Common questions
What should a buyer require in an injection mold FAI report?
Require enough information to trace each agreed requirement to the released drawing or model, the measured sample, and the measurement result. A practical package includes the controlled revision; a ballooned drawing or characteristic list; nominal, limits, actual result and status; method and datum setup; sample, mold and cavity identity; approved resin condition; trial or production condition; photographs or functional evidence when applicable; and a visible disposition for every exception. The required depth should be set by the contract and the part's risks, not copied blindly from another programme.
Is a first article inspection report the same as PPAP?
No. An FAI is a verification package for a first article or defined configuration. PPAP is an automotive production-part approval process with its own customer, submission, and production-run requirements. An FAI report may be one useful element of a PPAP-type submission, but it does not by itself demonstrate that all PPAP or customer-specific requirements have been satisfied. State the required process and submission level in the purchase documents.
Can a calibration certificate prove that a molded part dimension is acceptable?
No. Calibration supports confidence in an instrument's stated performance, but acceptance also depends on a suitable method, resolution, fixture, datum alignment, program, part condition, operator or automated process, and the correct interpretation of the released requirement. For a close-tolerance or disputed characteristic, ask for evidence that the full measurement process is fit for the decision.
When should the supplier repeat FAI or dimensional evidence after a mold change?
Decide the trigger before release. Reassessment may be needed after a design revision, tool repair or geometry change, cavity change, resin or colorant change, process-route or machine change, new measurement method, or a quality event that could affect the approved requirement. The needed scope should be proportionate to the change and risk: it may be focused remeasurement, cavity-specific evidence, functional testing, or a broader submission. Require supplier notification and written buyer approval when the agreement or customer requirement calls for it.
References
Source material
- [1] International Aerospace Quality Group (IAQG), “9102 First Article Inspection Requirement”
- [2] Automotive Industry Action Group (AIAG), “Production Part Approval Process”
- [3] International Organization for Standardization (ISO), “ISO 10012:2026 Quality management — Requirements for measurement management systems”
- [4] American Society of Mechanical Engineers (ASME), “Y14.5 Dimensioning and Tolerancing”
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.