
A PPAP package for injection molded parts should include the customer-assigned submission level, a completed Part Submission Warrant (PSW), the applicable design and change records, process flow, PFMEA, control plan, measurement-system evidence, dimensional and material or performance results, representative samples and any customer-specific forms. The exact bundle is not universal: the OEM, contract, part risk and reason for submission decide what must be submitted and what the supplier retains. AIAG positions PPAP, FMEA, control plans and MSA as connected quality core tools rather than unrelated forms [1].
For Europe, the United States and Middle East procurement teams, the practical test is traceability. A reviewer should be able to follow the chain from the current drawing and CTQs to process risks, controls, inspection methods, results, deviations and the person authorized to approve the submission. A PPAP file is evidence for a defined part, tool, material and production condition; it is not a blanket promise that every later lot or design revision will perform identically.
Quote-oriented CTA model: ask suppliers to quote the tooling and molding scope separately, then state which PPAP level, sample quantity, dimensional report, MSA study, material or performance tests, packaging evidence and customer forms are included. Ask the supplier to list exclusions and assumptions before you compare prices. The visuals in this guide are illustrative only; they do not depict an InjeForm customer part, facility or production result.
01
Start with the submission level and approval reason
PPAP levels control what is sent to the customer, not whether the supplier should internally understand every applicable element. Common AIAG-style descriptions are Level 1, warrant only; Level 2, warrant with samples and limited supporting data; Level 3, warrant with samples and complete supporting data; Level 4, warrant plus customer-defined requirements; and Level 5, warrant with complete supporting data available for review at the supplier. A customer-specific manual can define the levels differently or limit the choices. Enerpac, for example, documents its own level definitions and defaults its stated process to Level 3 unless otherwise agreed [2].
Before requesting a quote, identify the reason for submission: a new part, design or drawing change, material change, tooling transfer, process change, supplier change, corrective action or periodic reapproval. Then ask the customer quality contact to confirm the level, due date, sample basis, retention rules and any OEM-specific forms. IATF Global Oversight publishes separate customer-specific requirements for multiple OEMs, which is a useful reminder that an automotive PPAP instruction cannot be assumed to apply unchanged across customers [4].
A lower submission level does not automatically mean lower internal discipline. The supplier still needs enough records to support the PSW and to show that the submitted results came from the named revision, resin, tool and process condition. If evidence is omitted from the customer copy, record where it is retained and how it can be retrieved if the customer asks for a review.
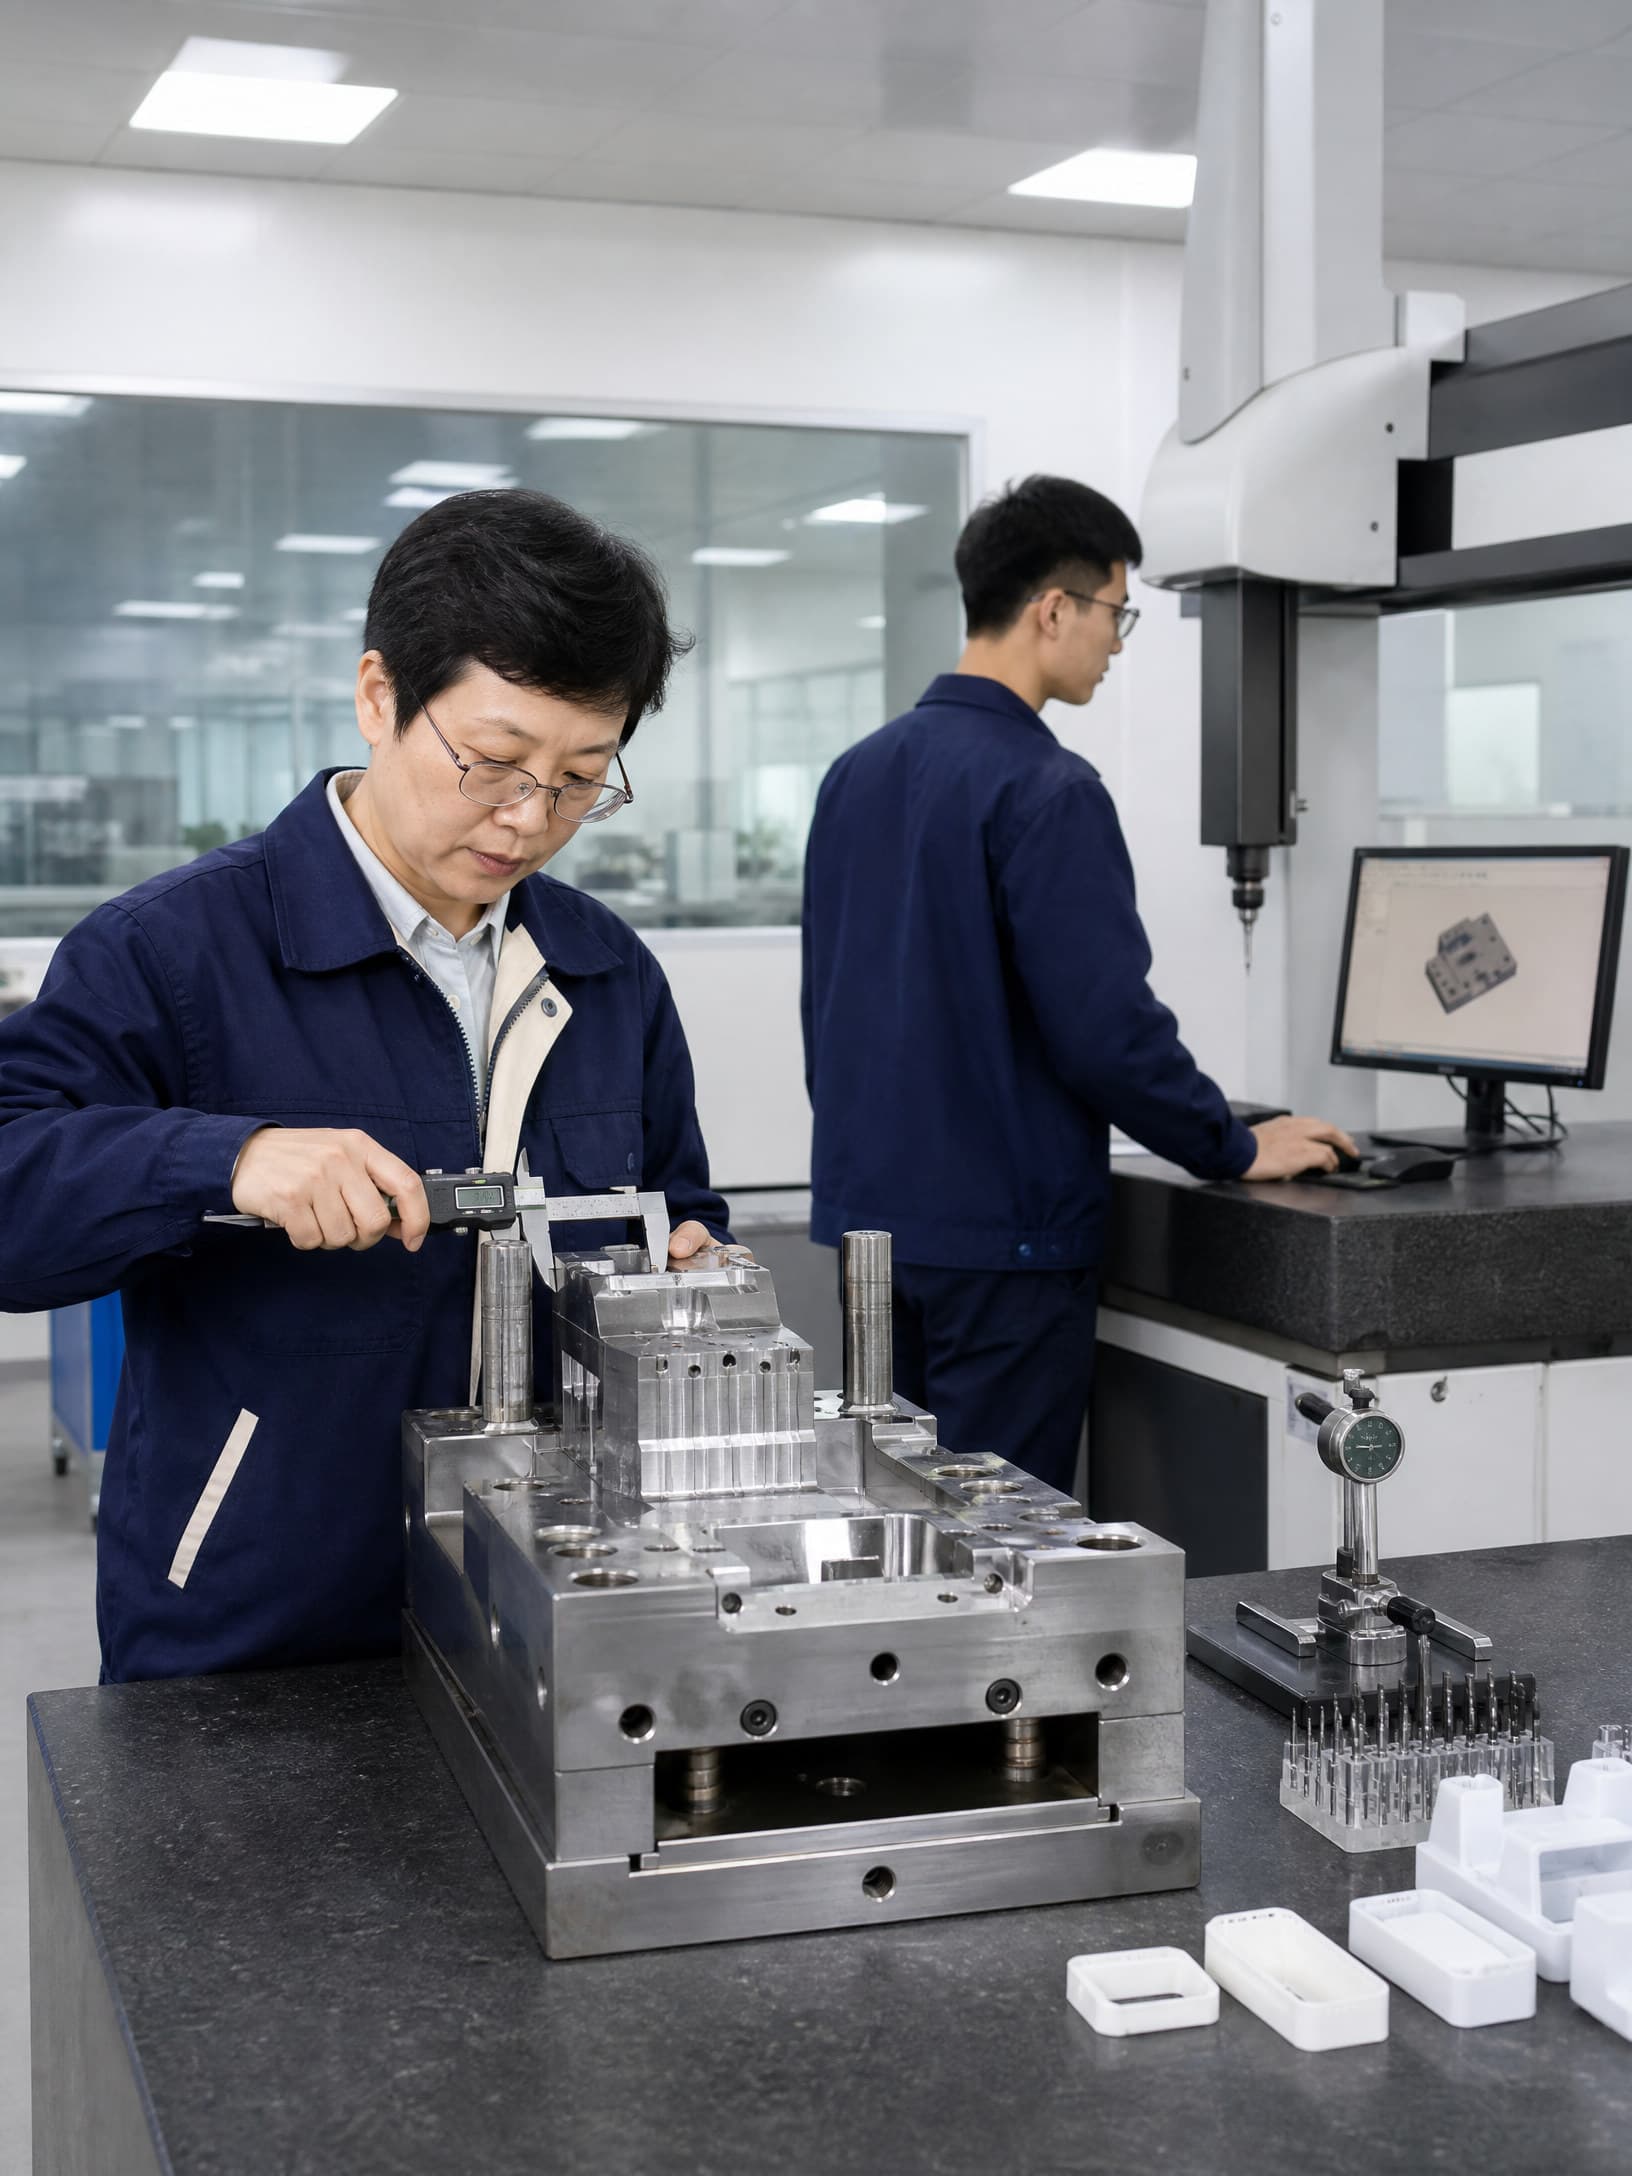
| Submission level | Customer typically receives | Buyer decision to confirm |
|---|---|---|
| Level 1 | PSW or warrant, often with limited data or appearance information as requested | Why is limited evidence adequate, and what supporting records are retained? |
| Level 2 | PSW, product samples and selected supporting data | Which elements are included, and which are available on request? |
| Level 3 | PSW, samples and complete supporting data | Is this the default for a new molded part or significant change? |
| Level 4 | PSW plus customer-defined requirements | Which customer checklist or portal rules replace the standard bundle? |
| Level 5 | PSW and complete data available for review at the supplier | Who will review the records, and what site or remote access is required? |
02
Use the PSW as the package index and approval record
The PSW should let a customer identify the part number, revision, supplier, manufacturing location, submission reason, submission level, material or specification basis, sample status and approval declaration. It should point to the package contents and state any deviations, exceptions or incomplete items. A signed PSW is not a substitute for missing evidence; it is the summary and decision record for the evidence behind it [2].
For molded parts, check that the PSW aligns with the drawing revision, CAD revision, cavity configuration, resin grade and colour or additive direction used for the run. If a family mold, insert mold, overmold or multi-cavity tool is involved, identify the configuration and how samples represent it. If the submission is interim or conditional, state the quantity, time limit, affected requirement and approver rather than using an unqualified approval statement.
The PSW should also make the commercial handoff readable. In a quote request, ask whether document preparation, sample parts, packaging, testing, translations, portal upload and customer responses are included. That prevents a low tooling or unit price from being compared with a broader quality scope.
03
Connect PFMEA, process flow and the control plan
The process flow describes the route from incoming resin and components through molding, trimming or assembly, inspection, packing and release. The PFMEA then asks what can fail at each step, what causes or controls exist, and what response is needed. The control plan turns the relevant risks and product requirements into operating controls: the characteristic, specification, method, sampling or frequency, reaction plan and responsible role. AIAG describes FMEA, control plans and PPAP as connected core tools, so buyers should look for consistent part names, process-step numbers and critical characteristics across the documents [1].
For injection molding, the control plan may address resin identity and drying where applicable, machine and mold setup, cavity or insert configuration, process-window checks, first-off approval, dimensional and visual inspection, functional checks, packing and change control. Do not require a generic list of machine settings as proof of control. Ask which parameters or checks are critical for this part, how they are recorded, what happens after an out-of-control result and how nonconforming parts are contained.
The PFMEA and control plan should explain the evidence request. A critical sealing diameter may need a defined fixture and measurement study. A cosmetic face may need a limit sample and lighting condition. A material-sensitive feature may need resin-lot identification or conditioning before measurement. The documents should not promise controls that the production floor cannot perform or that the inspection report cannot verify.
| Package record | Question it should answer | Evidence to cross-check |
|---|---|---|
| Process flow | What happens, in what order, and where are parts identified or released? | Part revision, tool configuration, inspection and packing steps |
| PFMEA | What can fail, why, and how is risk reduced or detected? | Process steps, special characteristics and reaction logic |
| Control plan | What is checked, by which method, how often and with what response? | Drawing CTQs, PFMEA controls, gauges and inspection results |
| Reaction plan | What happens when a result is out of specification or a control is lost? | Containment, disposition, escalation and restart authorization |
| Change record | What changed after the approved baseline and what evidence was repeated? | Engineering change, revised PFMEA, control plan and PSW status |
04
Make MSA and dimensional evidence defensible
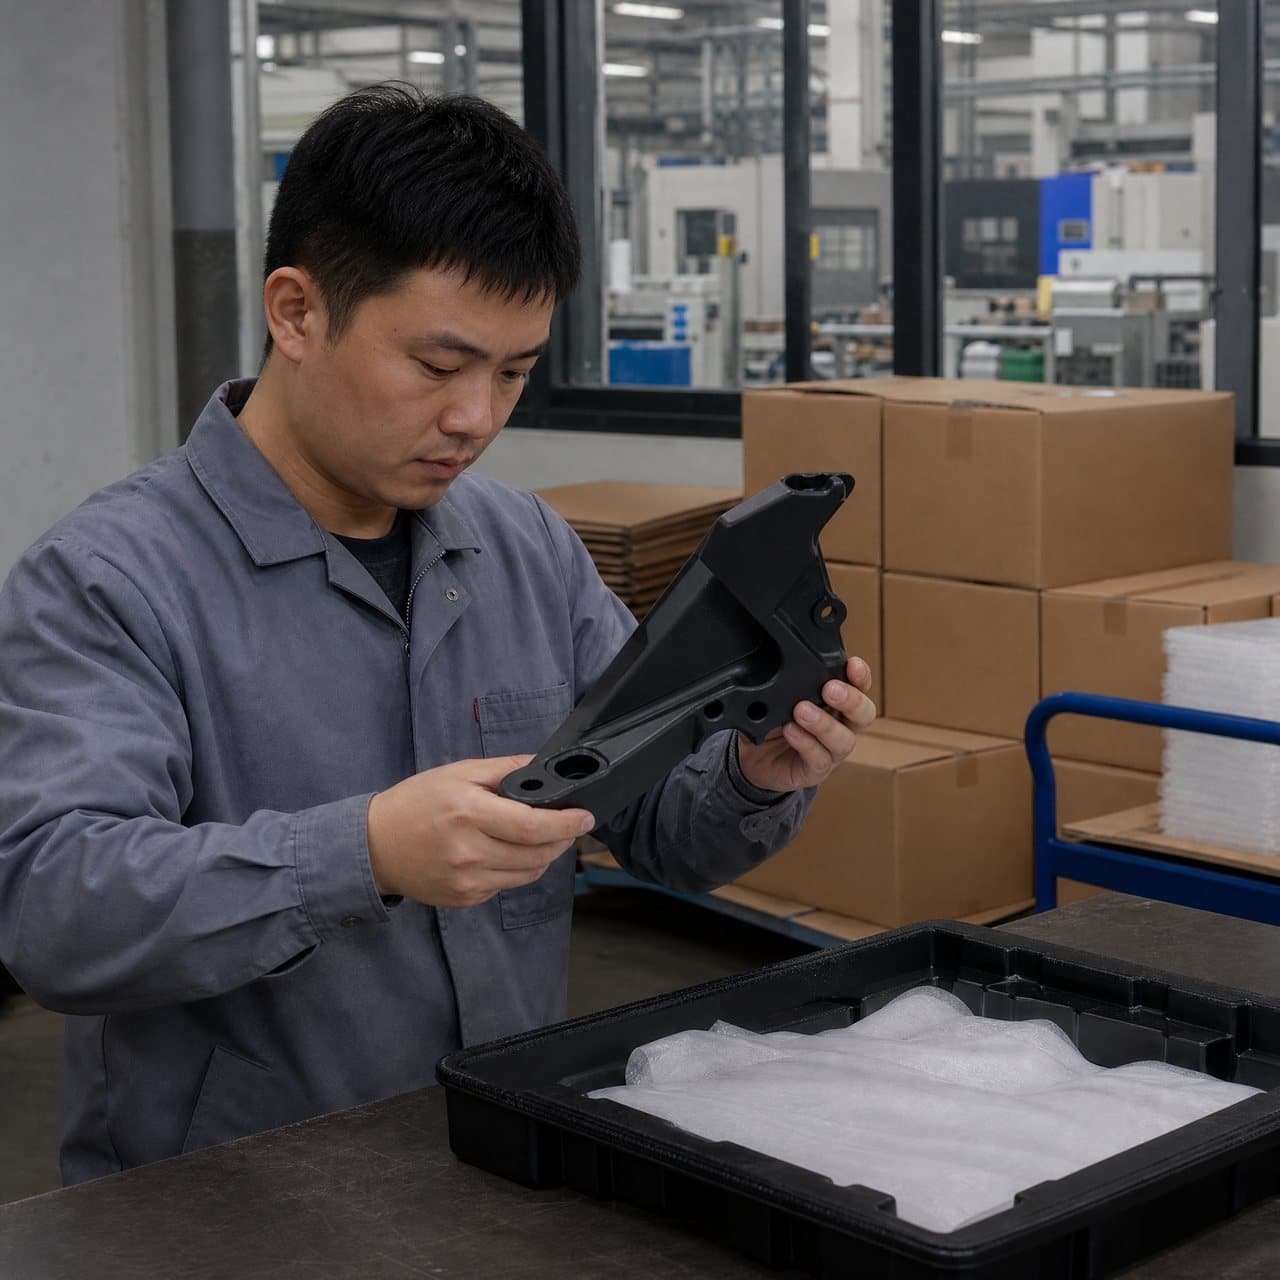
Measurement System Analysis (MSA) supports confidence that the measurement method can distinguish conforming from nonconforming molded parts. NIST describes gauge R&R studies as a way to characterize gauge and instrument performance in production, including repeatability and reproducibility; its handbook also discusses stability, bias, resolution and linearity as relevant measurement issues [3]. For a PPAP package, the appropriate study depends on the characteristic, gauge, fixture, operators, resolution, environment and customer requirement.
Ask for calibration or verification status for the equipment used, the measurement method or work instruction, the study scope, the data summary and the acceptance basis agreed with the customer. A gauge R&R result should not be copied from another part or fixture without checking whether the same measurement setup and tolerance context apply. Attribute agreement or a defined visual limit-sample method may be more relevant for subjective appearance checks than a variable gauge study, but the choice should be documented.
Dimensional results should identify the part and drawing revision, sample or cavity identity, characteristic number, nominal and tolerance, measured value, method and disposition. Include material or conditioning state where it can affect the result. If a result is close to a limit, review the measurement uncertainty and method suitability rather than presenting extra decimal places as certainty. Link material certificates, laboratory reports, performance tests, appearance approvals and master samples to the same part and submission baseline.
05
Review the evidence package before approving production
A complete review compares the PPAP checklist with the actual files. Depending on the level and customer, the package may include design records and ballooned drawings, approved engineering changes, customer engineering approval, process flow, PFMEA, control plan, MSA, dimensional results, material or performance test results, initial process studies, qualified laboratory records, appearance approval, sample parts, master samples and checking aids. The supplier manual reviewed for this guide lists these elements and notes that customer-specific requirements may add tooling, packaging or measurement-equipment information [2].
Confirm that the samples came from a significant and identified production condition, or clearly mark them as trial or development samples if they did not. Review cavity-to-cavity representation, resin manufacturer and grade, lot traceability where required, machine and tool identity, process records, inspection method, nonconformities and concessions. Do not infer capability indices from a small convenience sample or treat a clean dimensional report as proof of ongoing process control.
The final approval should name the decision: approved, interim or conditional approval, rejected for correction, or held pending evidence. It should identify open actions, owners, due dates and whether production shipment is permitted. For a quote-oriented procurement file, request a document matrix that labels each item as included, customer-supplied, not applicable with rationale, available on request or excluded from the price. This makes the supplier’s offer and the eventual PPAP review easier to compare.
Practical takeaway
Before you move
to the next review.
- Confirm the customer-assigned PPAP level, submission reason, due date, sample basis and customer-specific forms before the supplier starts the package.
- Check that the PSW, drawing, CAD, material, tool configuration, process flow, PFMEA and control plan use the same part and revision baseline.
- Request dimensional, material, performance, appearance and process evidence that is traceable to identified samples, cavities, lots, gauges and production conditions.
- Review MSA scope, gauge status, method suitability and reaction plans instead of accepting an unqualified gauge R&R statement.
- Record the approval status, deviations, concessions, open actions, owners and permitted shipment conditions in the final decision.
FAQ
Common questions
Is Level 3 PPAP always required for injection molded parts?
No. The customer or contract assigns the level, and some customers define their own submission routes. Level 3 is often used for new or higher-risk parts, but confirm the current customer-specific requirement rather than assuming a default.
Does the PSW replace PFMEA and the control plan?
No. The PSW summarizes the submission and records the supplier's declaration. PFMEA explains process risk, while the control plan defines how requirements and risks are controlled and reacted to.
Does every PPAP need a full gauge R&R study?
Not necessarily. MSA scope should match the characteristic, measurement method, risk and customer requirement. Critical variable measurements may need a gauge R&R study; visual or attribute checks may need another documented method.
Can a supplier submit PPAP evidence from a T1 mold trial?
It can be used when the customer accepts the trial basis and the evidence is clearly identified, but T1 is not automatically production approval. Ask whether the run used representative tooling, material, process conditions and sample quantities for the decision being made.
What should a buyer do if a supplier says an item is not applicable?
Ask for the customer's rule, the reasoned applicability decision and the supporting record retained by the supplier. If the item affects a critical requirement, agree an alternative evidence route or a documented concession before approval.
References
Source material
- [1] Automotive Industry Action Group (AIAG), Quality Core Tools and PPAP resources.
- [2] Enerpac, Supplier PPAP Manual Global, Revision 2.0.
- [3] National Institute of Standards and Technology (NIST), Gauge R&R Studies.
- [4] IATF Global Oversight, OEM Customer Specific Requirements.
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.