
Injection-molded snap-fit housings can remove separate screws, inserts or secondary assembly steps, but a snap is not automatically the lowest-risk joining method. It must flex during assembly, retain the mating half in service and still be moldable, ejectable and inspectable. The right decision depends on the resin grade, arm geometry, mating geometry, wall map, appearance constraints, expected assembly method, service temperature, chemicals, repeated-use expectation, tooling concept, annual volume and the customer’s own acceptance requirements.
For an overseas OEM or procurement team, the practical question is not simply whether a supplier can mold clips. It is whether the supplier can turn the specified housing interface into a controlled, reviewable part of the program. This guide separates buyer-defined requirements from engineering recommendations, identifies the evidence worth requesting, and sets approval gates from DFM through production release. It is intentionally not a universal dimension, force, tolerance or material prescription: those outcomes have to be demonstrated on the nominated resin, tool, process and assembly condition.
Requirement: define what the housing must retain, survive, look like and document. Recommendation: choose the snap architecture, resin grade and validation plan only after the mating condition, service environment and production method are known.
01
When is a snap-fit housing the right product and sourcing route?
A snap-fit housing is a good candidate when two molded halves or a cover and body need fast assembly without a separate fastener, and the product can accept the access, retention and service limitations of an integral plastic joint. Common examples include consumer devices, electrical covers, sensor shells and equipment enclosures. The design team should first decide whether the enclosure is intended to be permanently closed, opened for service, opened many times, or used as a locating feature before another joining operation. These are requirements because they determine the load case and failure definition. A snap used once during final assembly is not the same design problem as a battery door or field-serviceable access panel. Snap fits need comparison against screws, ultrasonic welding, adhesive bonding, heat staking or a hybrid approach—not a default selection. Screws can support controlled service access and potentially higher clamp loads, but add components and assembly operations. Welding or adhesive can help with permanence or sealing, but can complicate repair, inspection or disassembly. A snap may lower piece-count and assembly complexity where the geometry and resin support it; it may be a poor fit where a specified seal, high sustained load, repeated opening, aggressive environment, tamper resistance or controlled torque is central to the product requirement. Ask the supplier to show the proposed joint architecture on the parting-line, gating and ejection concept, rather than accepting a generic statement that clips can be molded. At RFQ stage, provide the latest 3D model and drawing, both mating components, intended assembly direction, estimated volumes, any assembly fixture or automation concept, product environment, expected number of openings, visible-surface zones and the functional definition of a successful latch. A buyer should identify whether retention, opening force, flushness, rattle, ingress behavior, cosmetic marks or service access is critical. Where a requirement is not yet fixed, mark it as an open decision with an owner and approval date. This makes quotations comparable and prevents a supplier from silently choosing geometry or material assumptions that later become a fit dispute.
02
Convert the housing function into a snap-fit design brief
A usable brief describes the complete elastic path, not only the final engaged position. For a cantilever hook, that means the arm root, length, section change, hook, lead-in, undercut, mating land, clearances and stop features. The assembly path should avoid an unintended hard interference that drives the arm beyond its intended deflection. The retained condition should avoid loading an edge that can creep, wear or become sensitive to tolerance accumulation. A deliberate lead-in and a clear retention face may help, but their geometry must remain compatible with mold opening, draft and tool steel access. Recommendation: use strain-based engineering analysis or appropriately representative development testing to screen a feature before committing tool steel. Covestro’s snap-joint guide explains that permissible undercut is tied to the material’s permissible strain and shape, and that the joining force includes both bending and friction effects.[1] Treat guide values and formulas as a starting method, not as approval limits for a different resin, color, filler level, wall map or temperature. Reinforcement, modifiers, regrind policy, moisture condition, weld lines and orientation can alter behavior. The selected resin supplier’s current grade data and the actual molded feature should govern the released design. Requirement: specify the interfaces that must locate and the directions in which the two halves may not move. Also define which conditions are cosmetic and which are functional. Recommendation: use positive locators or rails to manage alignment separately from the flexible latch where feasible, and allow draft, radii, ejection support and robust steel conditions to be reviewed with the mold design. A local thick root can create molding and cosmetic risks, while a sharp transition can concentrate stress; neither a universal radius nor a single wall-ratio rule resolves every housing. The supplier should document any compromise between structural behavior, sink risk, filling, cooling and visible-face quality for buyer engineering review.
03
Select resin and architecture by the operating condition—not family shorthand
Material selection for a snap feature needs more than a generic request for ABS, PC-ABS, nylon or POM. The nominated grade must be reviewed for short-term flexing, retained stress, creep or stress relaxation, impact exposure, temperature range, humidity or chemical exposure, color and appearance, electrical or flame-related project requirements, and compatibility with the mating component. BASF notes that material behavior under sustained loading and the effects of modifiers and reinforcement can vary, which is directly relevant when a housing latch stays deflected or carries load in service.[2] That does not make one polymer family universally suitable; it means the exact grade and use condition matter. The comparison below is a selection aid for an RFQ and design review. It is not a material approval matrix, a warranty of life, or a substitute for a grade data sheet and molded-part validation. If a regulatory, flammability, food-contact, medical or electrical condition applies, the product owner must state the applicable requirement and approval route. UL explains that UL 94 classifications describe small-scale specimen behavior under controlled test conditions; they do not by themselves establish the performance or approval of an assembled housing.[3]
| Decision factor | What the buyer should specify | Evidence to request | Approval gate |
|---|---|---|---|
| One-time assembly or repeated service | Expected opening cycles, assembly speed, access direction and acceptable actuation or removal behavior. | Feature analysis or trial plan; representative assembly method; proposed pass/fail criteria. | Engineering accepts the assembly and service-use definition before tool release. |
| Sustained retention or load | Load direction, duration, temperature profile, vibration or drop condition, and allowed movement or noise. | Named resin grade data; risk review for creep, relaxation and mating contact; part-level test proposal. | Customer approves the duty-cycle and retention-validation plan. |
| Environment and exposure | Service and storage temperatures, humidity, UV, cleaners, oils, disinfectants or other relevant media. | Grade-specific compatibility information where available; stated assumptions and any test recommendation. | Product team accepts the environment matrix and gaps before sampling. |
| Appearance and molding feasibility | Show surfaces, permitted gate or ejector zones, texture, color, sink and parting-line acceptance criteria. | DFM with gate, weld-line, venting, ejection and wall-transition review; cosmetic sample plan. | Buyer signs off the controlled visual standard or sample disposition. |
| Electrical or flame-related requirement | Exact requirement, applicable thickness or configuration, market and end-product responsibility. | Current grade documentation relevant to the stated condition; traceability and change-control proposal. | Product owner confirms that material evidence supports the specified product approval route. |

04
Design the tooling and process review around fit, molding and assembly together
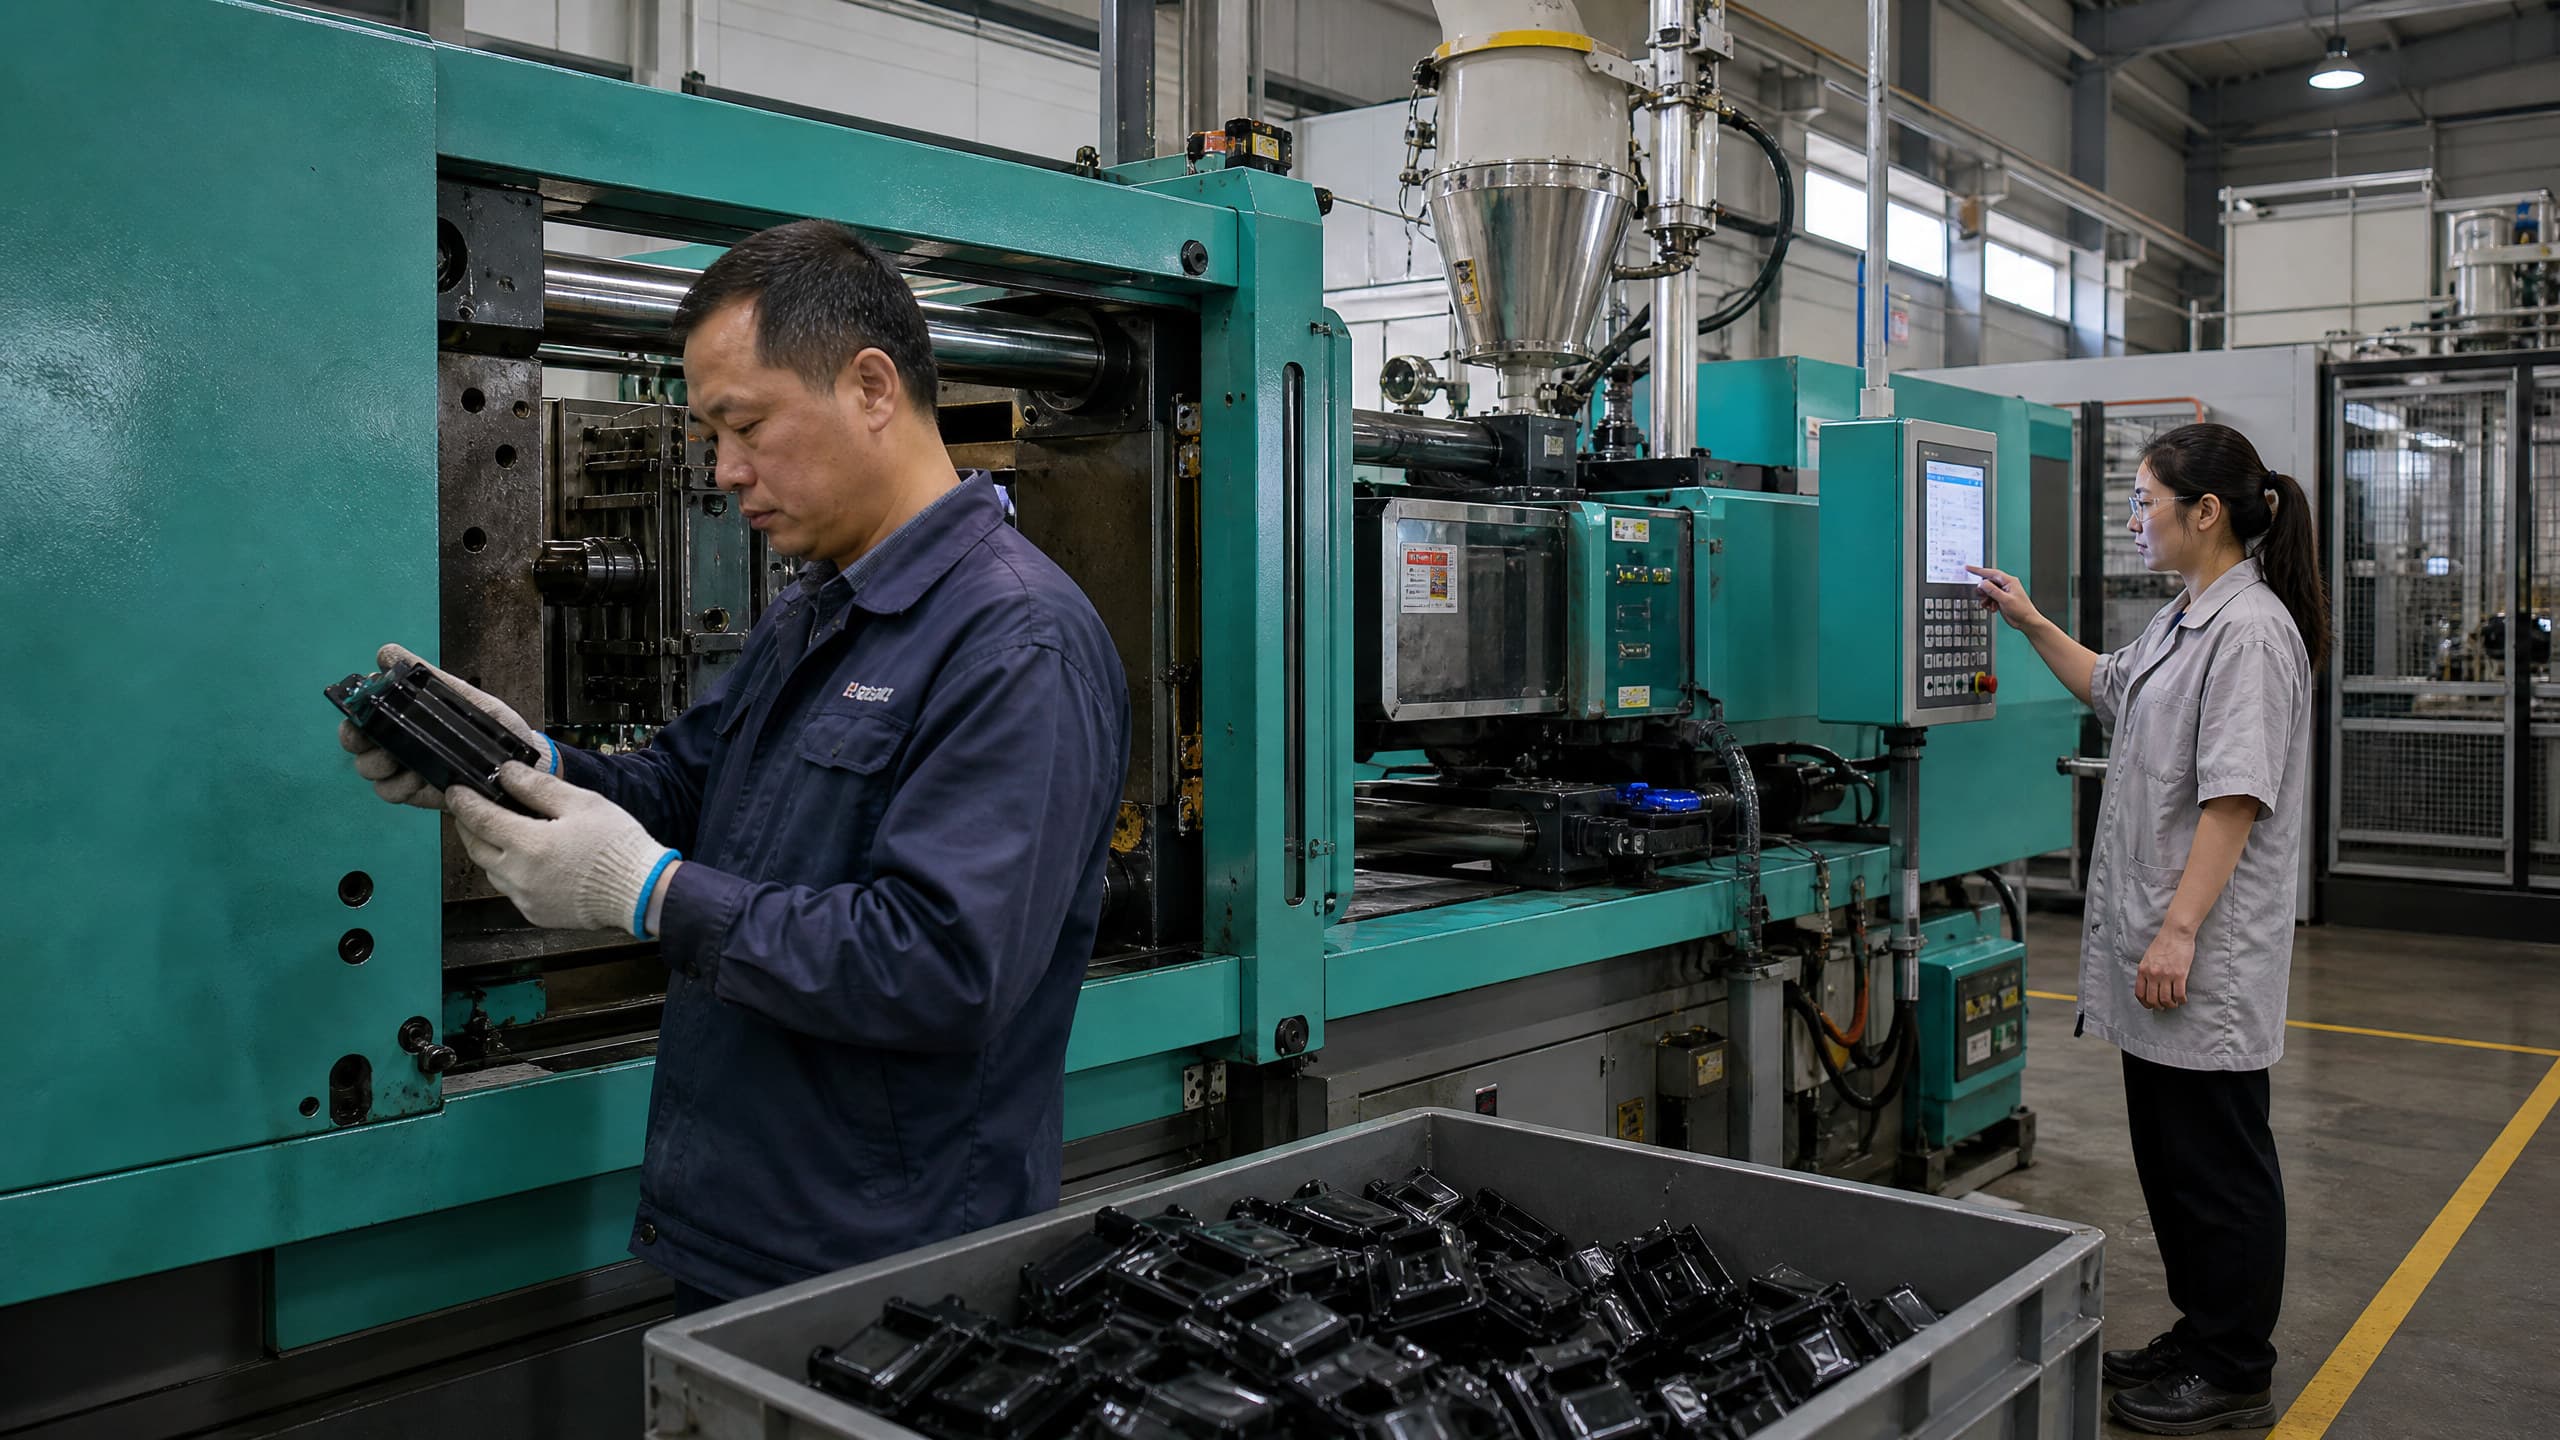
Tooling choices can change the risk profile of a snap-fit housing. Parting-line placement, gate location, flow direction, weld-line position, venting, cooling, ejection, slide or lifter access, cavity layout and surface texture all interact with a latch and its mating half. A feature that is mechanically plausible in CAD can be difficult to fill, pack, cool or eject without witness marks, distortion or damage. The supplier should therefore review the full assembly, not each half as an isolated cosmetic shell. If a latch is close to a weld line, a highly textured face, a gate vestige or an ejection point, ask what the expected effect is and how it will be assessed at trial. Requirement: the customer should define drawing revision, critical-to-function and cosmetic characteristics, material and color direction, permitted alternatives, and the approval authority for tool or process changes. Recommendation: ask the supplier for a DFM package that includes nominal and local wall sections, draft direction, proposed gates, parting lines, ejection, likely steel conditions, shrinkage assumptions and open risks. For a pair of housings, request a mating-stack review that identifies the interfaces driving closure gap, engagement and flushness. Avoid an unexplained universal tolerance callout. Actual capability depends on the resin, geometry, tool construction, molding machine, process window, cavity behavior, measurement method and the agreed specification. Sampling should mimic the approved process intent as closely as practical. Record tool and cavity identification, material lot and grade, color, relevant machine and process settings, sample quantity, conditioning where relevant, inspection method and deviations. This record does not certify a product by itself; it allows the customer to understand what was actually evaluated. Where automated assembly is proposed, validate with the intended fixture, motion and rate or a justified surrogate. Hand assembly can hide interference, force or orientation problems that an automated station will reveal. Conversely, do not use an unrepresentative fixture result to promise an automated cycle time or assembly yield.
05
Use evidence-led validation and release gates with the supplier
A snap-fit validation plan should test the feature’s defined function and likely failure modes. Depending on the product brief, this can include first assembly, disengagement where serviceable, retention after engagement, closure gap and flushness, rattle or movement, damage inspection, repeated opening, temperature-conditioned assembly, drop or vibration exposure, and relevant chemical exposure. The buyer should define the test article configuration, sample condition, method, fixture, measurement system, pass/fail criteria, owner and disposition route. A result without these details is difficult to compare across trials or suppliers. Use sequential gates rather than treating the first molded sample as a final release. Gate 1 is a documented DFM and risk review before cutting steel. Gate 2 is a tool-trial review of fill, ejection, appearance, dimensions and preliminary assembly. Gate 3 is functional validation using the agreed representative assemblies and conditions. Gate 4 is production-release approval after the customer has reviewed the specified evidence, deviations and control plan. The depth of each gate should match the product’s risk, volume and customer specifications. A low-risk consumer cover may need a different evidence package from a safety-related, regulated or long-life industrial enclosure. Ask for a supplier evidence pack that matches those gates: controlled drawing and revision status; resin manufacturer, exact grade, color and traceability statement; DFM and tool concept; cavity and sample identification; dimensional and visual results against the agreed requirements; assembly or retention results; process record; deviation log; and a documented change-notification route. Define what changes need approval, including resin grade or source, colorant, tool steel, cavity repair, gate or vent changes, process location, mold transfer and revised assembly equipment. Procurement can then compare scope, evidence and change discipline rather than selecting only on quoted piece price. Production approval should remain with the customer’s designated authority; supplier samples are evidence, not an automatic authorization to ship.

Practical takeaway
Before you move
to the next review.
- Define whether the housing is permanent, serviceable or repeatedly opened, and state the required retention, access, appearance and environmental outcomes.
- Provide both mating-part revisions, interface datums, local wall map, critical features, assembly direction, expected volumes and any fixture or automation assumptions.
- Nominate the resin manufacturer and grade direction, color, permitted alternatives, exposure conditions and any customer-defined approval requirements.
- Request a joint DFM and mating-stack review that shows gates, parting lines, ejection, draft, steel conditions, open risks and proposed actions.
- Release tooling and production only through documented sample, functional-validation, deviation and change-control approval gates.
FAQ
Common questions
Are injection-molded snap-fit housings cheaper than screwed housings?
They can reduce separate fasteners and assembly steps, but they are not automatically the lower-total-cost choice. Compare tooling complexity, material, cycle and handling assumptions, assembly equipment, service needs, scrap risk, validation work and the cost of any later design change. Ask each supplier to state the assumptions behind the quote instead of accepting a generic saving claim.
Which plastic is best for a snap-fit enclosure?
There is no universal best resin. Select a named grade against the actual deflection, retained load, temperature, chemicals, humidity, impact, cosmetic, electrical and reuse requirements. Reinforcement and additives can materially change snap behavior. Confirm the supplier’s proposed grade with current technical information and representative molded-part evaluation.
How should an OEM validate a snap-fit housing before mass production?
Start with a DFM and mating-stack review, then assess representative molded assemblies against buyer-defined function, appearance and environment conditions. Record the material, tool or cavity, process context, sample condition, fixture and pass/fail criteria. Close deviations and approve a control and change-notification plan before production release. The exact test scope should follow product risk and customer specifications.
Can a UL 94 material rating approve a snap-fit electronic housing?
No. UL describes UL 94 as small-scale material flammability testing under controlled conditions. It can be relevant material evidence when the exact grade and stated condition match the requirement, but it does not itself approve an assembled product, establish regulatory compliance or prove snap-fit function. The product owner should define the applicable end-product requirements and validation route.
References
Source material
- [1] Covestro — Snap-Fit Joints for Plastics: A Design Guide
- [2] BASF — Ultraform POM Product Brochure
- [3] UL Solutions — Combustion Fire Tests for Plastics
- [4] ISO — ISO 9001:2015 Quality Management Systems
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.