
Lightweighting an injection-molded part is not simply a matter of choosing the lowest-density polymer. The buyer must preserve the functions that the part performs while understanding how resin family, fiber loading, geometry, processing, environment, production volume and customer specifications interact. A lighter material may change stiffness, impact response, shrinkage, warpage, surface appearance, tooling assumptions and validation scope. This guide gives overseas OEM, procurement, quality, engineering and product teams a practical way to compare candidates and approve a controlled material decision.
Treat weight reduction as a requirements-and-evidence project: define the maximum acceptable mass, functional limits and compliance needs first; then require supplier data, molded samples and approval gates before releasing a resin or geometry change.
01
What should buyers compare when selecting a lightweight polymer?
Start with requirements, not a preferred resin name. The requirement may include a mass target, load case, deflection limit, drop or impact condition, temperature range, chemical exposure, appearance, flame or other customer-controlled specification, dimensional tolerance and expected production life. Recommendations such as a resin family, fiber percentage or wall-thickness concept should remain provisional until the part and process are evaluated.
Density is useful for screening, but it does not predict finished-part performance by itself. Compare specific stiffness and strength, impact behavior, creep, moisture sensitivity, shrinkage, weld-line performance and surface requirements. Ask whether the published values describe the same grade, test direction, conditioning and temperature that apply to the product. ASTM D638 provides a tensile-property test method, while ISO 294-4 addresses molding and post-molding shrinkage of injection-molded thermoplastics; neither standard removes the need for part-level validation.[1] [2]
A practical shortlist normally includes an unfilled engineering thermoplastic, a mineral- or glass-reinforced grade, and a lower-density option such as a foamed or specialty grade when the application permits. The right comparison is application-specific. A reinforced resin can raise stiffness but may increase anisotropy and tooling or cosmetic risk. A lower-density grade can reduce mass but may reduce load capacity or require a geometry change.
02
Polymer comparison for a first procurement screen
The table below is a screening framework, not a substitute for a grade-specific datasheet, mold-flow review or molded-part test. Values and behavior vary substantially by polymer family, additive package, fiber content, moisture condition, part geometry and process window. Buyers should ask suppliers to complete the comparison using the exact proposed commercial grades.
| Candidate family | Potential lightweighting route | Typical trade-offs to investigate | Evidence to request before approval |
|---|---|---|---|
| Unfilled PP or similar commodity thermoplastic | Low material density and broad availability can support mass reduction where loads and temperature are moderate. | Lower stiffness than many engineering grades; creep, impact, shrinkage and chemical exposure may govern the design. | Exact grade datasheet, conditioned impact and tensile data, shrinkage assumptions, cycle study and sample dimensional report. |
| Unfilled engineering thermoplastic such as PC, ABS or PBT | Can combine moderate density with controlled appearance or dimensional performance, depending on the family and grade. | Cost, moisture or temperature sensitivity, impact behavior, surface expectations and chemical compatibility differ by resin. | Grade-specific thermal, mechanical, impact, flammability or customer-specification data; processing window and aging plan. |
| Glass- or mineral-reinforced thermoplastic | Higher modulus may allow ribs, wall or section changes that reduce mass while retaining stiffness. | Fiber orientation can make properties directional; weld lines, surface read-through, shrinkage imbalance, abrasion and tool wear need review. | Fiber content and orientation assumptions, mold-flow results where warranted, gate concept, warpage risk review and molded coupons or parts. |
| Foamed or microcellular molded grade | Cell structure may reduce density or pack weight in suitable geometries. | Surface finish, dimensional control, cell uniformity, strength, sealing and customer acceptance can be more process-sensitive. | Foam-process capability, density distribution, surface samples, dimensional capability and application-specific mechanical testing. |
| Specialty low-density or recycled-content grade | A material formulation may reduce mass or support a customer sustainability requirement. | Supply continuity, lot variation, odor, colour, moisture, mechanical consistency and qualification status must be confirmed. | Traceable formulation and supplier declaration, lot-to-lot data, change-notification terms and approved-source plan. |
03
How lightweighting changes stiffness, impact, shrinkage and warpage
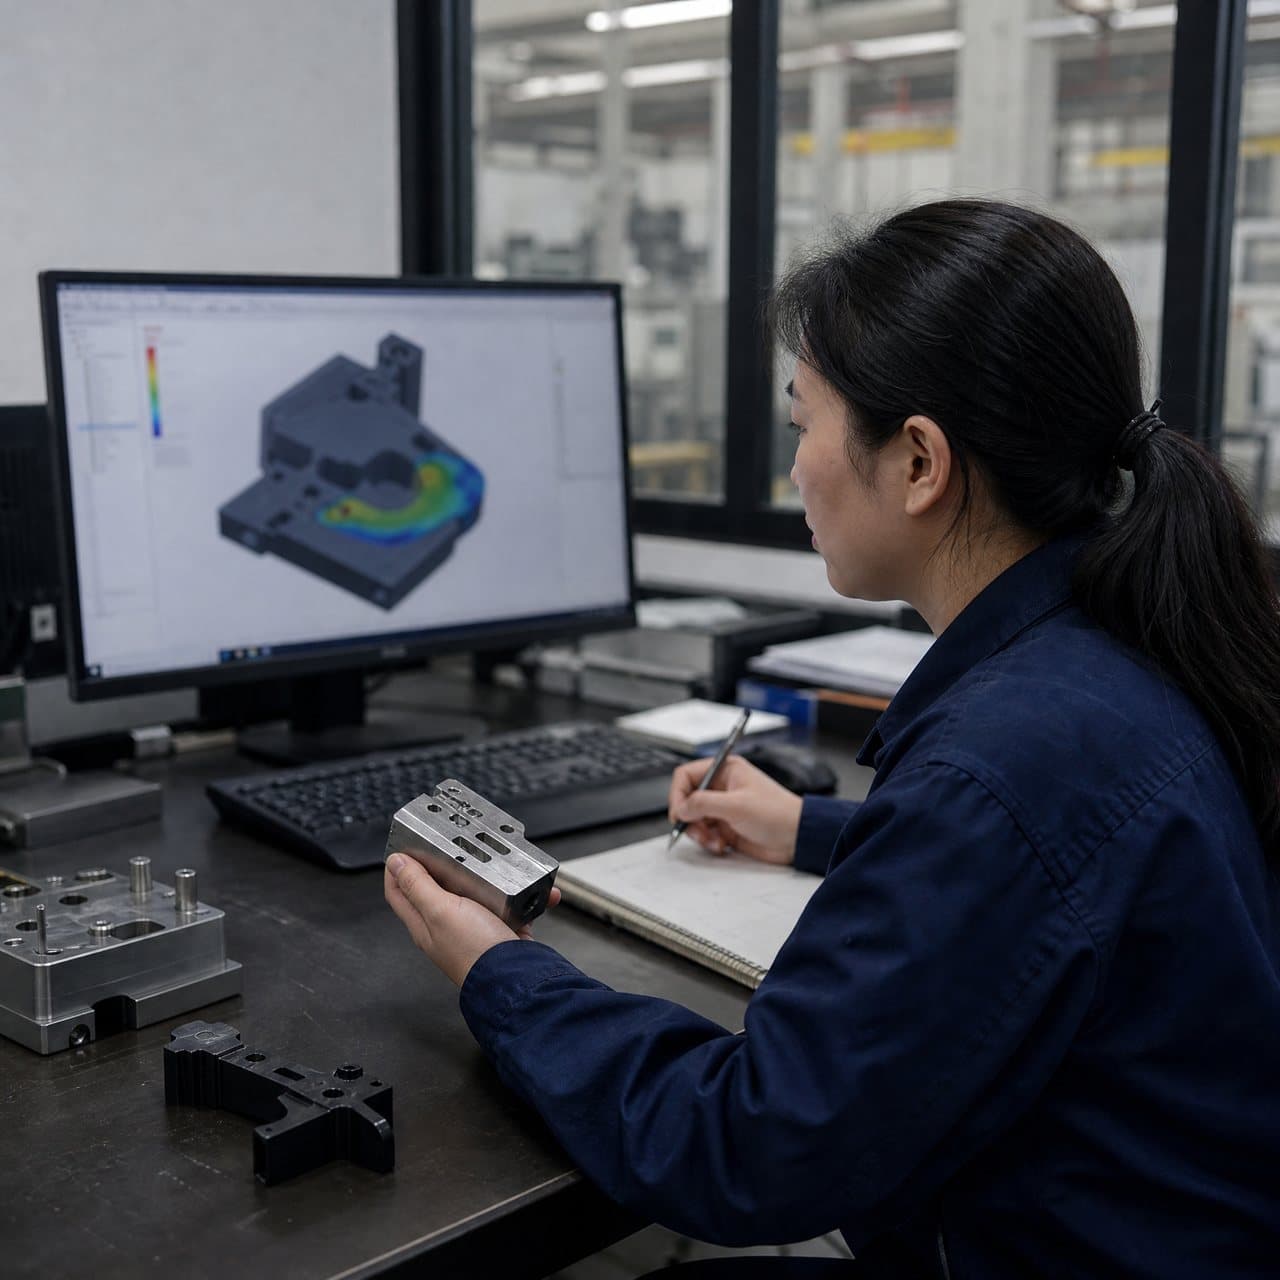
Removing material from a section usually reduces bending stiffness unless the geometry is reconfigured with ribs, beads, closed sections or other load-efficient features. Increasing fiber loading can raise modulus in the flow direction, but the resulting part may not behave isotropically. Autodesk’s molding guidance notes that fiber orientation strongly affects mechanical behavior and that warpage is linked to regional shrinkage variation.[3] Treat orientation, weld lines and gate location as design variables rather than after-the-fact process details.
Impact performance can move independently from stiffness. A part that passes a static load case may still fail in a drop, snap-fit, vibration or cold-temperature event. Lower density, thinner walls, notches, sharp transitions and weld lines can all change the failure mode. Require the product team to define the relevant impact or abuse test, including temperature and conditioning, instead of using a generic “toughness” claim.
Shrinkage and warpage also depend on resin, fiber loading, flow length, wall transitions, mold temperature, packing, cooling and ejection. Lightweight geometry can make filling or packing less forgiving, while ribs and local thickness changes can create visible sink or dimensional drift. A supplier’s analysis should identify the assumed process window and show how the proposed material and geometry affect critical datums, interfaces and cosmetic zones.
04
Tooling, processing and validation implications
A resin change is not automatically a drop-in change. Flow behavior, melt temperature, mold temperature, drying requirements, shrinkage, abrasive fillers, venting, gate design and ejection loads may change. A reinforced or foamed grade can require different tool steels, wear allowances, gate details or maintenance assumptions; the actual need depends on the grade, fiber or additive content, volume and tool concept. Ask the molder to identify which tooling assumptions are requirements and which are recommendations.
For an overseas programme, establish approval gates before commercial production: material shortlist, resin and grade approval, DFM and mold-flow review where warranted, first-tool sampling, dimensional and functional testing, process capability review, and production-part approval. Quality should define the sample size, conditioning, measurement method, critical-to-quality features and record package. Procurement should make the approved grade, source, change-notification requirement, lead-time assumption and alternate-source plan part of the purchase documentation.
Supplier evidence should include the exact grade and revision, certificate or lot traceability as applicable, processing guidance, moisture controls, recycled-content or additive declaration where relevant, test reports, sample identification, dimensional results and open deviations. Do not treat a supplier datasheet, simulation image or prototype result as universal proof of production performance. The final acceptance basis remains the customer specification and the agreed validation plan.
05
A buyer’s decision path for approving weight reduction
First, freeze the non-negotiables: maximum mass, functional loads, interfaces, service temperature, exposure, appearance, compliance or customer requirements, annual volume and programme timing. Second, request two or more feasible material-and-geometry concepts rather than one resin recommendation. Third, compare normalized assumptions, including grade, fibre or foam content, cavity strategy, cycle basis, scrap, secondary operations, inspection and tooling changes.
Then approve the lowest-risk concept that meets the requirements with evidence, not necessarily the lowest-density or lowest quoted-cost option. Require a design review when the change affects wall sections, ribs, gates, weld lines, inserts, seals or mating dimensions. Require production-intent samples before releasing a customer-facing claim about mass, strength, cycle time, cost or compliance. Where the requirement cannot yet be demonstrated, record it as an open risk with an owner and due date.
This discipline helps teams avoid false economies. A material that saves grams but adds tool rework, unstable dimensions, extra inspection or a late qualification can increase total programme cost. Conversely, a geometry-led solution may reduce mass without changing resin, but it still needs moldability, appearance and validation review. The appropriate choice depends on the complete part-and-process system.
Practical takeaway
Before you move
to the next review.
- The team has defined mass, stiffness, impact, temperature, exposure, appearance and customer-specific requirements before selecting a resin.
- The comparison uses exact commercial grades with stated fiber, mineral, foam, recycled-content and conditioning assumptions.
- The supplier has identified effects on shrinkage, warpage, weld lines, tooling wear, drying, gate design and process window.
- Approval gates cover DFM, samples, dimensional capability, functional testing, traceability and production-intent validation.
- Purchase documentation names the approved grade, source, change-notification terms, inspection records and open deviations.
FAQ
Common questions
What is the lightest plastic for injection molding?
There is no universal best or lightest choice. A low-density commodity resin, foamed grade or reinforced design may reduce mass, but the correct option depends on stiffness, impact, temperature, chemical exposure, geometry, processing, volume and customer specifications. Screen density first, then approve against part-level requirements.
Does glass-filled nylon always make an injection-molded part lighter?
No. Glass fiber can increase stiffness and may enable a thinner or more efficient geometry, but the resin can also have higher density than an unfilled alternative. Fiber orientation, weld lines, moisture, warpage, surface requirements and tool wear must be evaluated for the specific part.
How should buyers validate a lightweight material change?
Use a staged approval plan: confirm the exact grade and supply source, review DFM and flow risks, mold production-intent samples, measure critical dimensions, run the agreed functional and environmental tests, and document deviations before production release. A datasheet alone is not part validation.
Can a thinner wall reduce cost and cycle time as well as weight?
It may, but no result is universal. Thin-wall geometry can increase filling, packing, cooling, warpage, appearance or tooling difficulty. Any claimed cost or cycle benefit should be demonstrated with the proposed resin, tool, process window, volume and inspection plan.
References
Source material
- [1] ISO 294-4:2018, Plastics — Injection moulding of test specimens of thermoplastic materials — Part 4: Determination of moulding shrinkage
- [2] ASTM D638-22, Standard Test Method for Tensile Properties of Plastics
- [3] ASTM D3641-21, Standard Practice for Injection Molding Test Specimens of Thermoplastic Molding and Extrusion Materials
- [4] Autodesk University, Fiber Orientation for Warpage Prediction and Structural Performance
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.