
Long-glass-fiber-reinforced thermoplastics can be considered when an OEM wants a molded structural part with a lower density than a metal alternative or a better stiffness-to-mass balance than an unfilled polymer. They are not a universal lightweighting solution. The outcome depends on the resin family, fiber loading and length retention, geometry, flow direction, processing window, service environment, annual volume, tooling concept and the customer’s released requirements. A thinner or lighter part can lose impact margin, fatigue life, dimensional stability or assembly robustness if the load path is not redesigned and validated. For overseas procurement, engineering and quality teams, the key decision is therefore not whether long glass fiber is “strong,” but whether a named grade and molded design can meet the required functions with evidence that matches the application.
Requirement: define the baseline mass, load cases, temperature and chemical environment, interfaces, appearance limits, safety or compliance requirements, sample condition and approval authority. Recommendation: ask suppliers to compare the current design and long-glass-fiber proposal on the same boundary conditions, with assumptions, unknowns and evidence gates clearly separated.
01
What does long-glass-fiber injection molding change in a structural part?
Long-glass-fiber compounds contain continuous or relatively long reinforcement in the pellets that is distributed and oriented during filling. Compared with an unreinforced grade, the molded material may provide higher stiffness or strength in selected directions, but the part response remains geometry- and process-dependent. Fiber breakage during compounding or molding, orientation through the flow path, weld-line formation, local section changes and temperature or moisture exposure can all affect the result. Datasheet values are useful for screening; they are not a part approval or a promise of a particular mass reduction.
Lightweighting should start with the load path rather than a blanket wall-thickness reduction. Ribs, closed sections, cored bosses, local pads and controlled transitions can place material where it carries load while avoiding unnecessary bulk. A supplier should show the proposed nominal and local wall map, fiber-flow direction, gates, weld-line locations, draft and ejection strategy, predicted shrinkage and warpage risks, and any features that become difficult to inspect or assemble. Engineering must decide whether the resulting directional behavior is acceptable for the actual load cases.
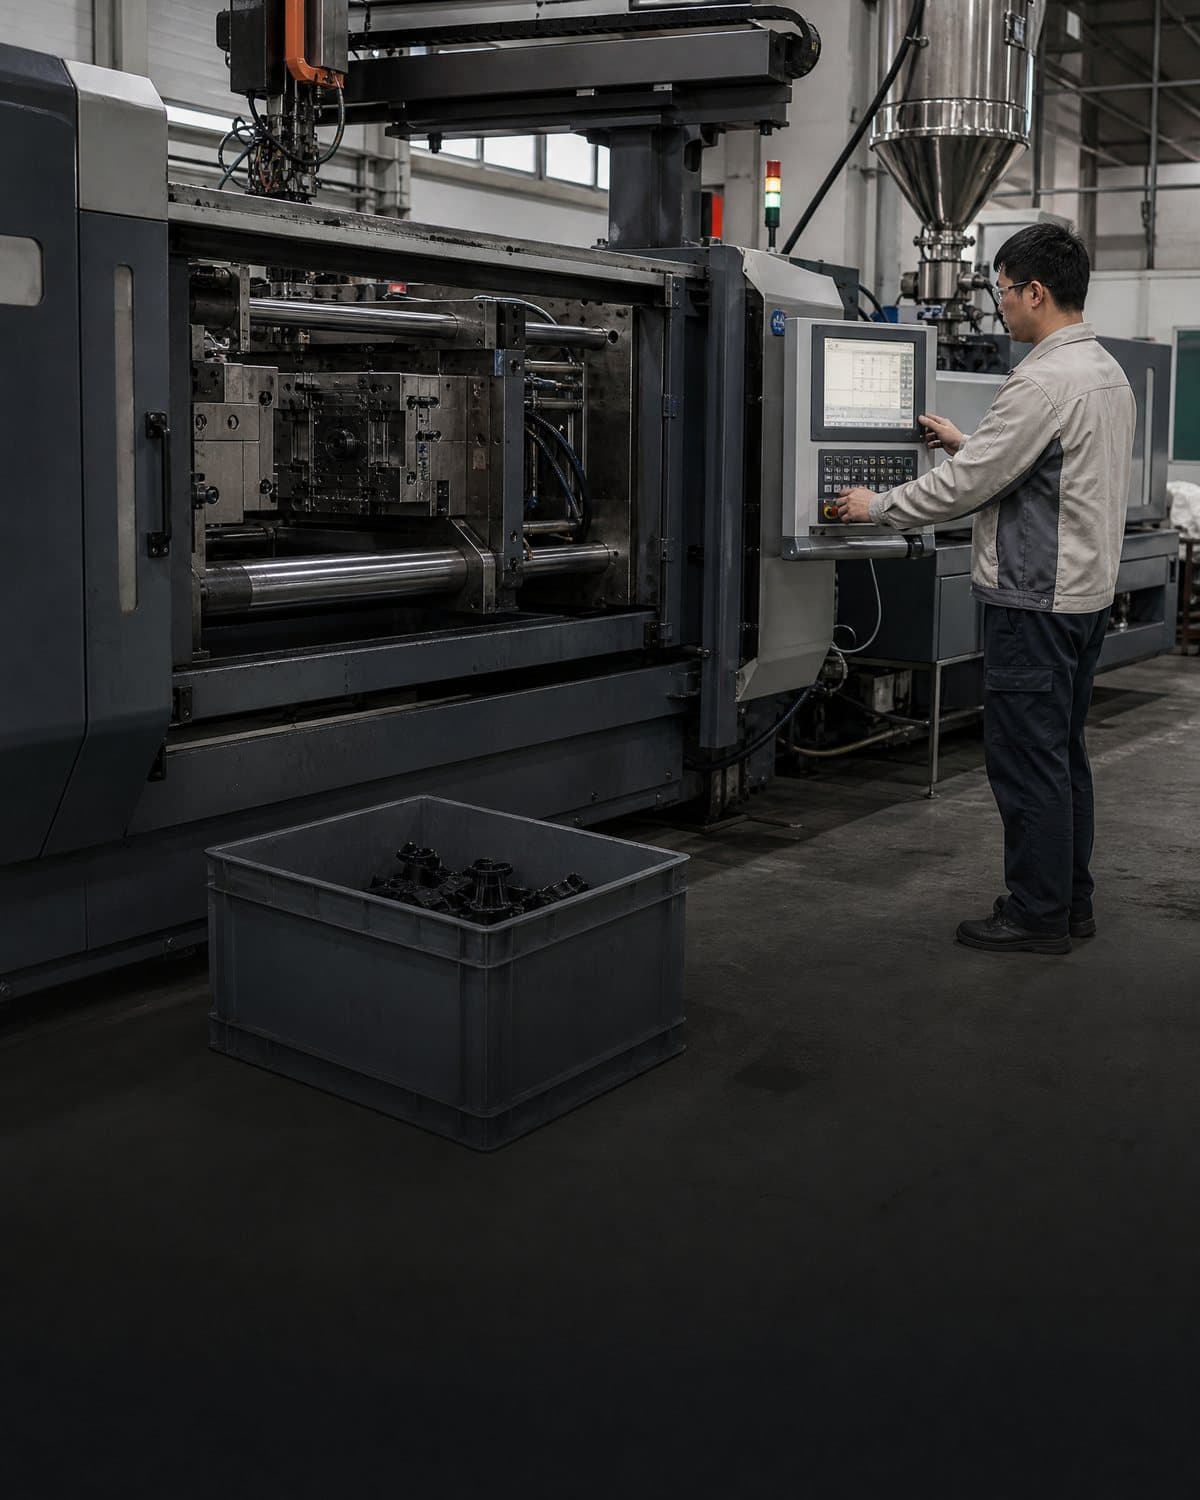
A long-fiber design can also alter the design envelope. The compound may need higher injection pressure, suitable gate and runner dimensions, wear-aware tool materials, controlled drying where specified, and a process window that preserves repeatability. These are recommendations for review, not universal settings. The exact material supplier, grade, fiber content, machine, mold and customer specification must control the final decision.
02
How should buyers compare long-glass-fiber options with metal or short-fiber alternatives?
Compare a controlled baseline with a named proposal, not material labels. The baseline should include part mass, stiffness or deflection requirement, impact and fatigue expectations, fastener or insert loads, dimensional interfaces, temperature and chemical exposure, appearance, service life, annual volume and all customer-specific requirements. A long-glass-fiber part may be a good fit for a bracket, carrier, support, seat or equipment structure in one load case and a poor fit for a thin, impact-dominated, highly cosmetic or electrically sensitive component in another.
The following screen helps procurement structure the RFQ. It is a decision aid, not a ranking of universal performance or cost.
Ask each supplier to state what the quotation assumes: resin source and grade, fiber percentage, colorant or additive package, regrind policy, cavity count, tool steel, gate and runner concept, machine range, secondary operations, inspection scope, yield basis, packaging and change-notification triggers. A lower unit price or lighter estimate is not comparable if one proposal excludes tooling wear, drying controls, validation, scrap or a different material grade.
| Route | Potential fit | Buyer must verify | Typical trade-offs to review |
|---|---|---|---|
| Long-glass-fiber thermoplastic | Mass-sensitive structural features where directional stiffness and molded integration may help | Exact grade, fiber loading, retained fiber length, load direction, environment and molded-part tests | Anisotropy, weld-line sensitivity, warpage, tool wear, surface appearance and material handling |
| Short-glass-fiber thermoplastic | Complex molded geometry needing a more established flow and reinforcement option | Grade data, orientation effects, local strength and dimensional behavior | Potentially lower reinforcement efficiency in selected load paths; still directional and process-sensitive |
| Unfilled engineering thermoplastic | Parts prioritizing impact, appearance, flexibility or simpler reinforcement behavior | Deflection, creep, temperature, chemical exposure and wall design | May require more section or ribs to meet stiffness, affecting mass and packaging |
| Metal baseline | High load, temperature, impact, conductivity or established certification requirements | Mass target, corrosion, joining, fatigue, forming or machining route and total cost | Higher density and possible assembly or corrosion burden; conversion is not automatically viable |
03
What are the main effects on stiffness, impact, shrinkage and warpage?
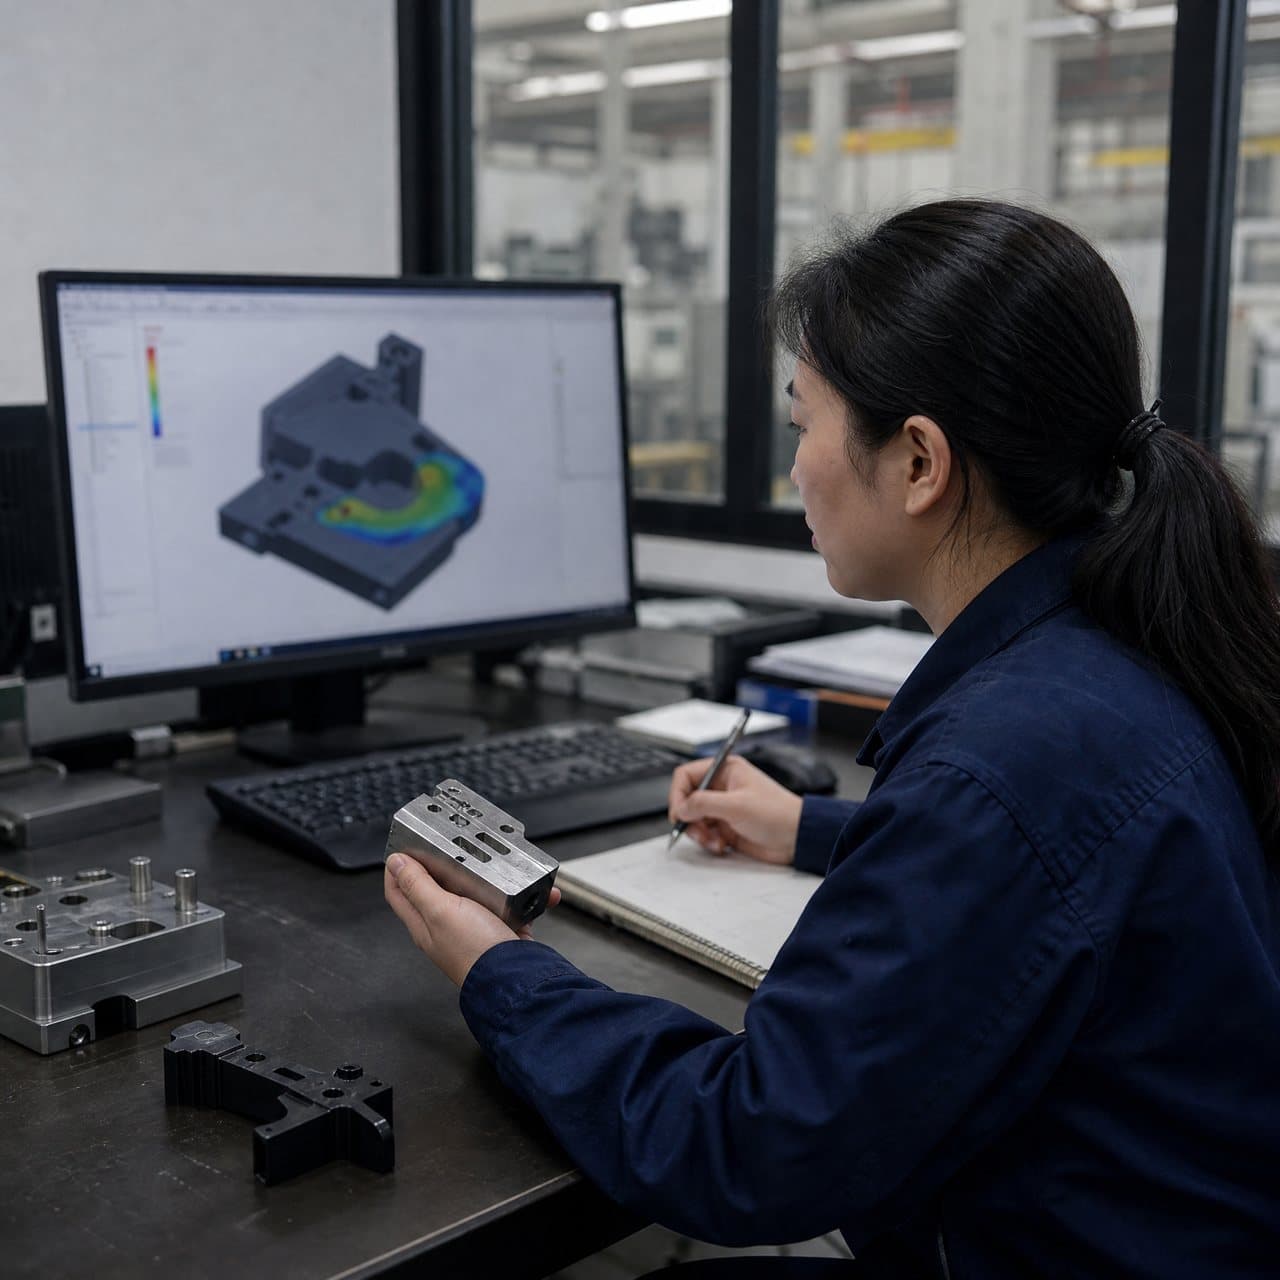
Stiffness is often direction-dependent because fibers tend to align with flow. The highest calculated modulus in a datasheet does not prove the same modulus across a rib, transverse wall, weld line or locally reoriented flow front. For structural validation, define load direction, supports, rate, temperature, conditioning, displacement or strain limits and failure criteria. Use analysis only with documented material models and assumptions, then correlate it with representative molded parts.
Impact and fatigue require separate attention. Reinforcement can improve selected load-bearing properties while reducing ductility or changing crack initiation and propagation behavior. A part that passes a room-temperature static test may behave differently after humidity, thermal cycling, chemicals, vibration, repeated assembly or a low-temperature impact. The customer should define which conditions are mandatory; the supplier should identify where the proposed grade and geometry are unproven.
Fiber orientation also changes shrinkage. Flow-direction and transverse shrinkage can differ, and non-uniform cooling, ribs, bosses, inserts, thickness changes and restrained interfaces can create warpage or residual stress. The tooling review should connect gate location, venting, packing, cooling and datum strategy to the drawing’s functional dimensions. Do not approve a generic tolerance claim for a new structural design; agree critical-to-function characteristics, measurement conditions, conditioning and cavity-specific evidence instead.
| Design variable | Lightweighting effect | Buyer verification |
|---|---|---|
| Fiber loading | Can raise stiffness at lower wall mass but may increase anisotropy | Request resin grade, fiber content and orientation assumptions |
| Wall thickness | May reduce mass but can challenge filling and impact targets | Review fill analysis, gates and sample test plan |
| Rib layout | Adds stiffness locally without solid thick sections | Check rib-to-wall ratio, sink risk and moldability review |
04
How do long-glass-fiber parts affect tooling, process control and quality?
Long-glass-fiber compounds can be abrasive and may place additional demands on gates, runners, shutoffs, ejectors and cavity surfaces. Tool material or surface treatment should be proposed against the exact compound and production volume, not selected from a generic “glass-filled” rule. The supplier should identify expected wear locations, maintenance intervals or inspection points, and what tool condition could affect dimensions or appearance. This is a sourcing and life-cycle issue, not only a tooling specification.
The process plan should identify the approved resin grade, lot traceability, moisture or drying controls where applicable, melt and mold-temperature ranges, fill and pack strategy, pressure or shot-size limits, cooling intent, start-up and purge controls, and reaction to deviations. These ranges are process-development inputs, not promises of cycle time or yield. Quality should ask how the supplier will distinguish a material change, fiber-content change, cavity issue, process drift or measurement variation from a design problem.
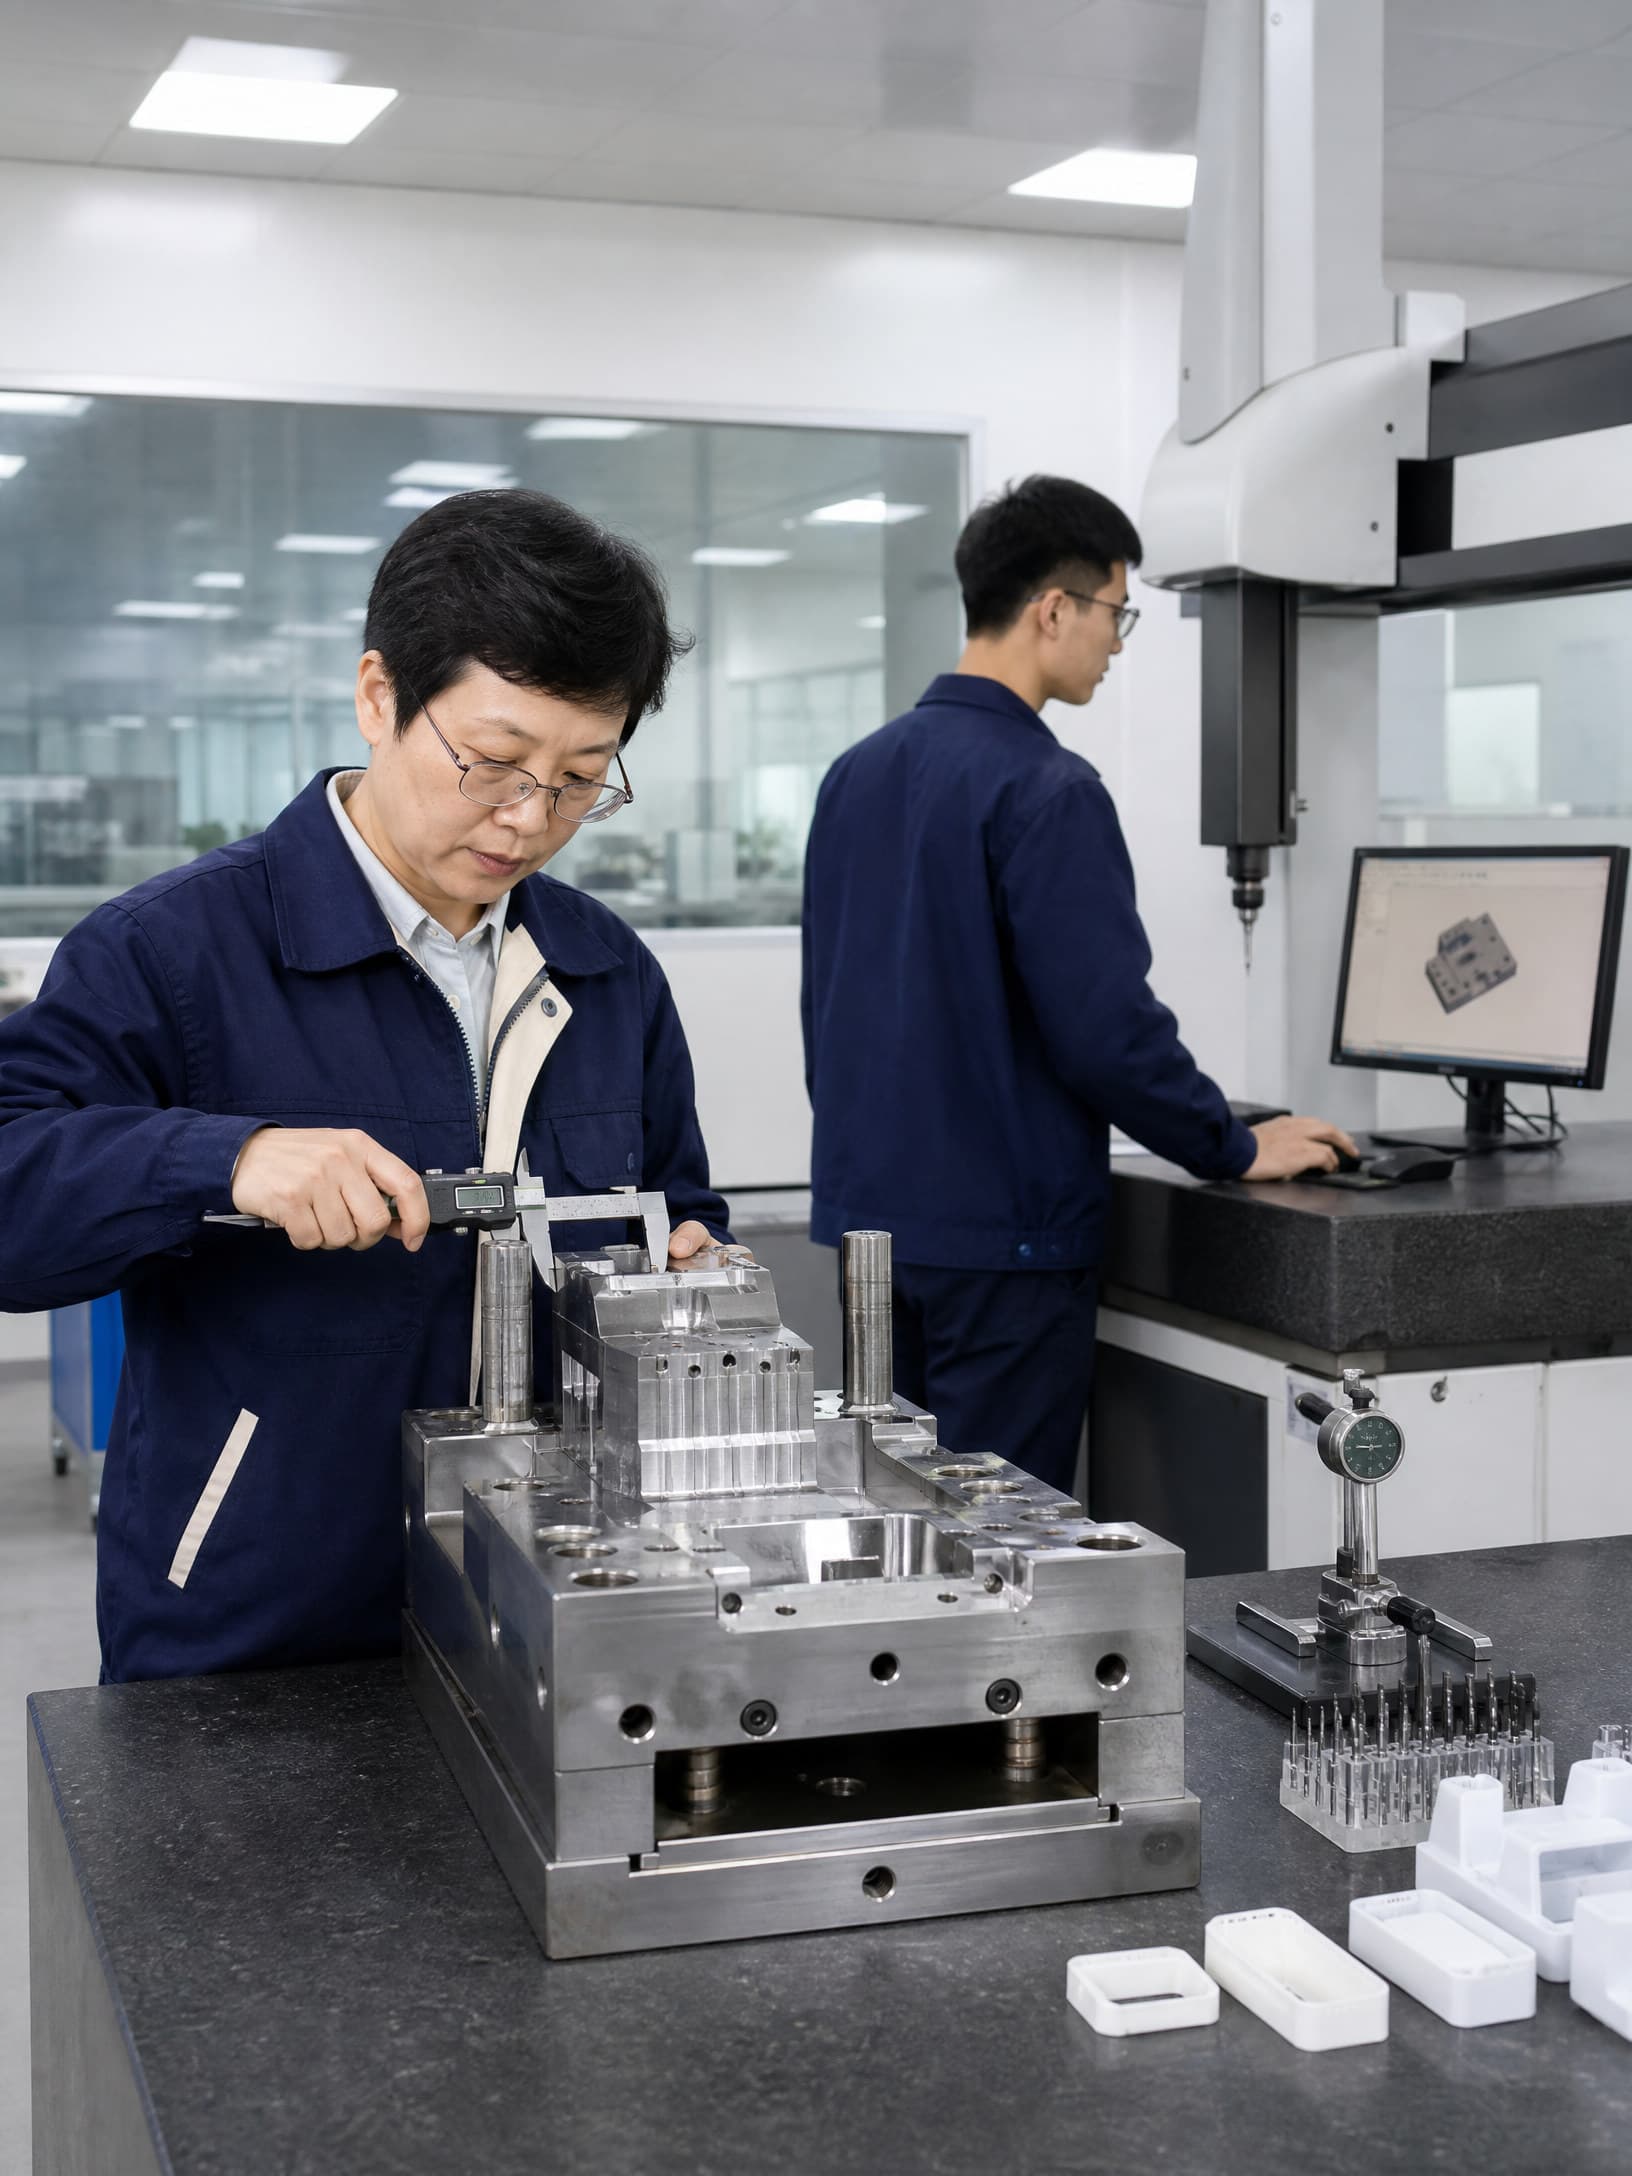
For sampling, require cavity and machine identification, material lot, color or additive details, process record, part mass method, conditioning, dimensional results, visual review, functional tests and deviations. If the part carries safety, regulatory, pressure, electrical or other controlled requirements, add the customer’s applicable qualification and compliance evidence. A supplier’s general certification or a simulation image does not replace part-specific approval.
05
Which approval gates and supplier evidence should an OEM require?
Gate 0 is a requirements freeze: baseline part revision, mass measurement, load cases, interfaces, service environment, appearance, volume, target cost, approved material constraints and change authority. Gate 1 is concept and DFM approval: the supplier submits the named grade, proposed fiber loading, section and rib strategy, flow and gate concept, tool material rationale, risks, simulation assumptions and validation plan. No steel should be released on a mass target alone.
Gate 2 is tool-trial review. Inspect fill, short-shot behavior, weld lines, flash, ejection, part mass, dimensions, warpage, appearance and assembly on identified cavities. Gate 3 is functional validation using representative molded parts, agreed fixtures and conditioning. Test static stiffness or deflection, impact, fatigue, fastener or insert performance, thermal or chemical exposure, vibration or other loads only where required by the product risk and customer specification. Gate 4 is production release after deviations, control plan, traceability, inspection method, packaging and change-notification rules are approved.
At RFQ and before release, request: current technical data for the exact grade; safety data and material traceability; DFM and mold-flow assumptions; tool steel or coating rationale; cavity layout; process window; measurement-system and inspection plan; sample and validation reports; failure analysis route; tool-maintenance plan; and a commercial breakdown separating tooling, engineering, material, molding, scrap, testing and logistics. Require written approval for resin or source changes, fiber loading, colorant, regrind policy, mold transfer, gate or vent changes, cavity repair, process location and inspection method.
Practical takeaway
Before you move
to the next review.
- Freeze the baseline part revision, mass method, load cases, interfaces, service environment, volume and customer approval authority.
- Request a named long-glass-fiber grade with fiber loading, resin source, processing assumptions, traceability and current technical data.
- Review flow direction, weld lines, ribs, section transitions, shrinkage, warpage, tool wear, draft, ejection and critical-to-function dimensions before tooling.
- Compare total delivered scope against metal, short-fiber and unfilled alternatives, including tooling, validation, scrap, maintenance, inspection and logistics.
- Approve production only after representative molded-part tests, deviations, control plan, change-notification rules and customer-specific compliance evidence are closed.
FAQ
Common questions
Can long-glass-fiber injection molding always reduce structural-part weight?
No. It may enable a better stiffness-to-mass design in selected load paths, but weight outcome depends on resin, fiber loading, geometry, orientation, environment, tooling, process capability and customer requirements. A validated baseline comparison is required.
Is a long-glass-fiber datasheet enough to approve an injection-molded structural part?
No. Datasheet properties are screening inputs. Approval should use the exact grade and molded geometry, documented processing and conditioning, representative dimensions, and product-specific static, impact, fatigue or environmental evidence required by the application.
What tooling risks should buyers discuss for long-glass-fiber compounds?
Discuss abrasive wear at gates and moving features, tool steel or coating rationale, gate and runner design, fiber orientation, ejection, cooling, shrinkage, warpage, maintenance and cavity-to-cavity measurement control. The correct solution depends on the compound, geometry and volume.
When should an OEM approve a long-glass-fiber replacement for a metal part?
Only after the customer’s requirements and approval authority accept the proposed material and design, the supplier closes DFM and tooling risks, and representative molded parts pass the agreed structural, environmental, dimensional, assembly and compliance validation.
References
Source material
- [1] ISO 20457 — Plastics moulded parts: tolerances and acceptance conditions
- [2] ASTM D638 — Standard Test Method for Tensile Properties of Plastics
- [3] ASTM D790 — Standard Test Methods for Flexural Properties of Unreinforced and Reinforced Plastics
- [4] SABIC — LNP long glass fiber reinforced thermoplastic materials overview
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.