
Yes, many hollow plastic parts can be made with injection molding, but a hollow section is not automatically a lower-risk or lower-cost design. Feasibility depends on the resin grade and fiber loading, required stiffness and impact performance, wall distribution, openings, draft, undercuts, expected environment, annual volume, machine and process capability, and the customer's specifications. The tooling route may be a conventional core-and-cavity mold that forms a cavity, a collapsible or unscrewing core for restricted openings, a removable or sacrificial core, or a specialized process such as gas-assisted injection molding. Each route changes tooling scope, validation evidence and production risk.
For an overseas OEM, the procurement question is not simply whether a supplier can make a hollow shape. It is whether the proposed geometry and tooling concept can deliver the required load path, dimensions, appearance, assembly and service life with a documented, transferable process. Treat lightweighting as a design trade-off: removing material can reduce mass, but it can also reduce bending stiffness, alter impact response, increase sensitivity to buckling or weld lines, and make shrinkage, cooling and warpage harder to control.
Requirement: define the finished part's load cases, interfaces, minimum openings, critical dimensions and environment. Recommendation: compare at least one conventional core-and-cavity route with any specialized hollowing route using part-level evidence before tooling release.
01
When is a hollow plastic part feasible for injection molding?
A hollow design is usually worth screening when the product needs an enclosed or partially enclosed volume, a tubular load path, a duct, a handle, a float, a reservoir-like form, or a housing with a controlled interior. The feasible architecture must still provide a practical way to form, support and release the internal surface. Identify the opening size, internal depth, core access, parting strategy, draft, ejection direction, sealing faces, assembly interfaces and any trapped air or drainage concern before asking for a tooling quotation.
Do not define feasibility by wall thickness alone. A thinner shell may save mass but can lose stiffness in bending or local compression. A taller or deeper section can sometimes restore section stiffness without adding much material, while ribs, beads, gussets or local bosses may be needed around fasteners and interfaces. Those features can create thick-to-thin transitions, weld lines and local cooling differences. Use the actual load cases and mounting conditions to decide whether the proposed hollow form is structurally adequate; a generic lightweighting percentage is not a design approval.
The exact resin matters. Unfilled and reinforced grades can differ in flow, shrinkage, anisotropy, impact response and dimensional stability. Fiber loading may improve stiffness in one direction while increasing directional shrinkage or making weld-line performance more important. Temperature, chemicals, moisture, UV exposure, cyclic loads, pressure and customer-specific compliance requirements must be assessed against the named grade and molded geometry, not against a polymer family name.
02
Compare tooling and process routes before selecting the hollow architecture
The following comparison is a sourcing screen, not a universal ranking. Ask the supplier to map each route to the released CAD, resin, volume, critical features, expected tool life, maintenance plan and validation scope. A lower initial tool quote can carry more complex maintenance, longer approval work or more difficult process control.
A conventional tool may be the most direct route when a core can enter and withdraw through an opening or when the part can be split into molded shells and assembled. A collapsible core, unscrewing core or side-action system may form a more enclosed interior, but moving mechanisms add design, fitting, wear, lubrication, inspection and repair considerations. Removable or sacrificial cores may suit selected geometries or development volumes, but cycle, material recovery, dimensional control and downstream handling require project-specific confirmation. Gas-assisted or other specialized processes can reduce melt in a defined region, yet they need specialized equipment, process development and evidence that the hollow region, skin, stiffness, appearance and interfaces meet requirements.
| Route | Potential fit | Main buyer checks before approval |
|---|---|---|
| Conventional core-and-cavity mold | An opening or split-line strategy allows the internal core to be inserted and released with practical draft. | Core access, ejection force, draft, parting-line location, internal surface finish, venting, cooling, sealing and any required assembly operation. |
| Collapsible, unscrewing or side-action core | The part has a restricted opening, internal thread, undercut or enclosed feature that cannot release by straight pull. | Mechanism reliability, tool maintenance, stroke and clearance, wear components, cycle assumptions, inspection access, spare scope and tool-transfer plan. |
| Removable or sacrificial core | The geometry or development stage justifies a core that is removed, dissolved, melted or otherwise handled after molding. | Core material and compatibility, removal method, residue, dimensional repeatability, operator controls, cycle impact, waste route and production-volume economics. |
| Gas-assisted or other specialized hollowing process | A defined region may benefit from a gas-formed core or reduced melt mass while retaining a suitable outer skin. | Equipment and supplier experience, gas entry and venting, skin thickness, pressure and stiffness evidence, appearance, safety controls, process window and qualification plan. |
| Molded shells joined in a secondary operation | The interior is easier to form as two or more open components than as one enclosed molding. | Weld, adhesive, spin, vibration or heat-staking method; joint strength and leak criteria; alignment; added labor; cosmetic line; and traceability of the assembled part. |
03
Control lightweighting effects on stiffness, impact, shrinkage and warpage
Weight reduction changes more than part mass. For a shell loaded in bending, stiffness is strongly affected by geometry and section depth, not only by the amount of resin. Local thinning can increase deflection, vibration, denting or buckling; a hollow form can also concentrate stress at corners, openings, clips, bosses and fastener locations. Require the design team to identify load paths, support points, allowable deflection, impact zones and failure modes. Where analysis is used, record the resin grade, fiber orientation assumptions, boundary conditions, wall map and load cases, then confirm the result with representative molded parts.
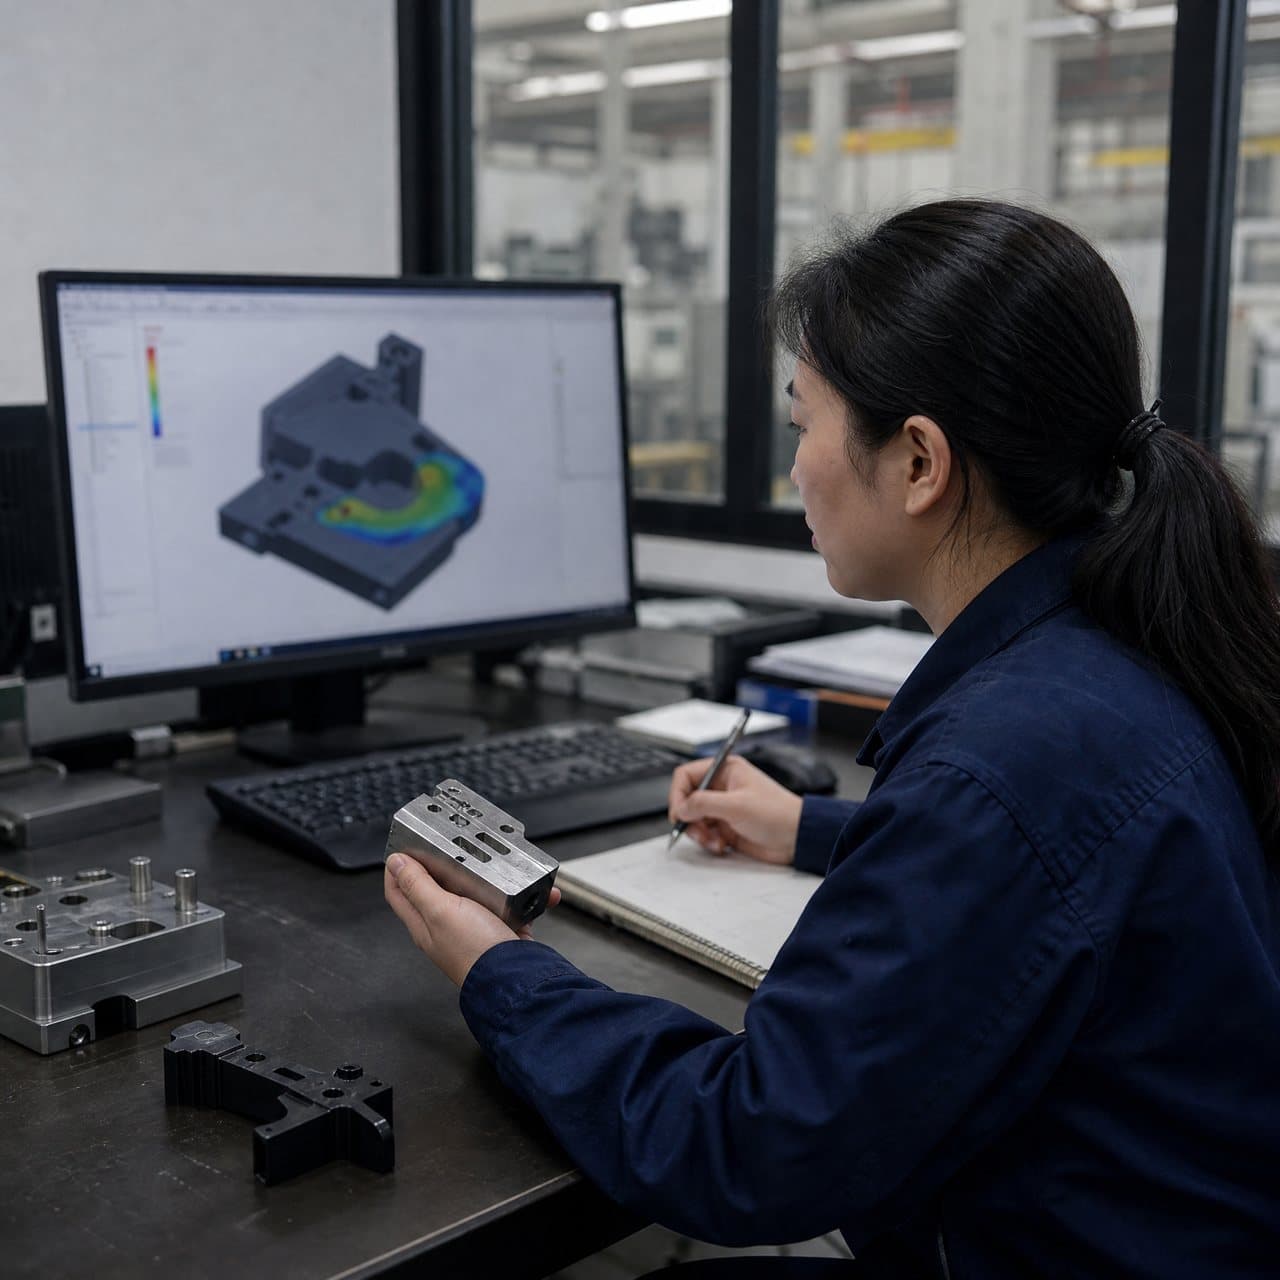
Hollow regions can complicate filling, packing, cooling and ejection. Flow fronts may meet at weld lines around cores, openings or inserts. Uneven sections can produce differential shrinkage and warpage, while a deep or poorly cooled core can retain heat and delay safe ejection. ASTM D955 notes that mold and melt temperature, fill time and packing conditions affect measured shrinkage, and that standard-specimen results do not predict absolute values for every real part geometry.[1] Use simulation as directional evidence where justified, but do not treat a software result as proof of production dimensions. Autodesk describes injection molding simulation as a way to examine filling, packing, cooling, deflection, tool design and material choices; the assumptions and physical validation remain part-specific.[2]
Ask for a risk map covering wall transitions, core tips, weld lines, gates, vents, ejection points, cooling blind spots and cosmetic faces. Require a proposed process window and a dimensional plan that distinguishes as-molded measurements from conditioned or assembled measurements. If the customer has pressure, leak, impact, stiffness, fatigue or drop requirements, define the test method, sample condition, sample size and acceptance decision before T1 or first-article trials.
04
Select geometry and validation evidence that match the application
Start the RFQ with the controlled 3D model and drawing revision, target mass or mass range if relevant, nominal and minimum wall intent, openings, internal features, datums, critical interfaces, cosmetic zones, load cases, temperature and chemical exposure, assembly method, annual demand and destination-market requirements. Separate mandatory requirements from preferences. For example, a leak-tight cavity, a connector fit, a pressure boundary or a defined impact result is a requirement; a preferred gate location or visual texture may be a recommendation until the product owner approves it.
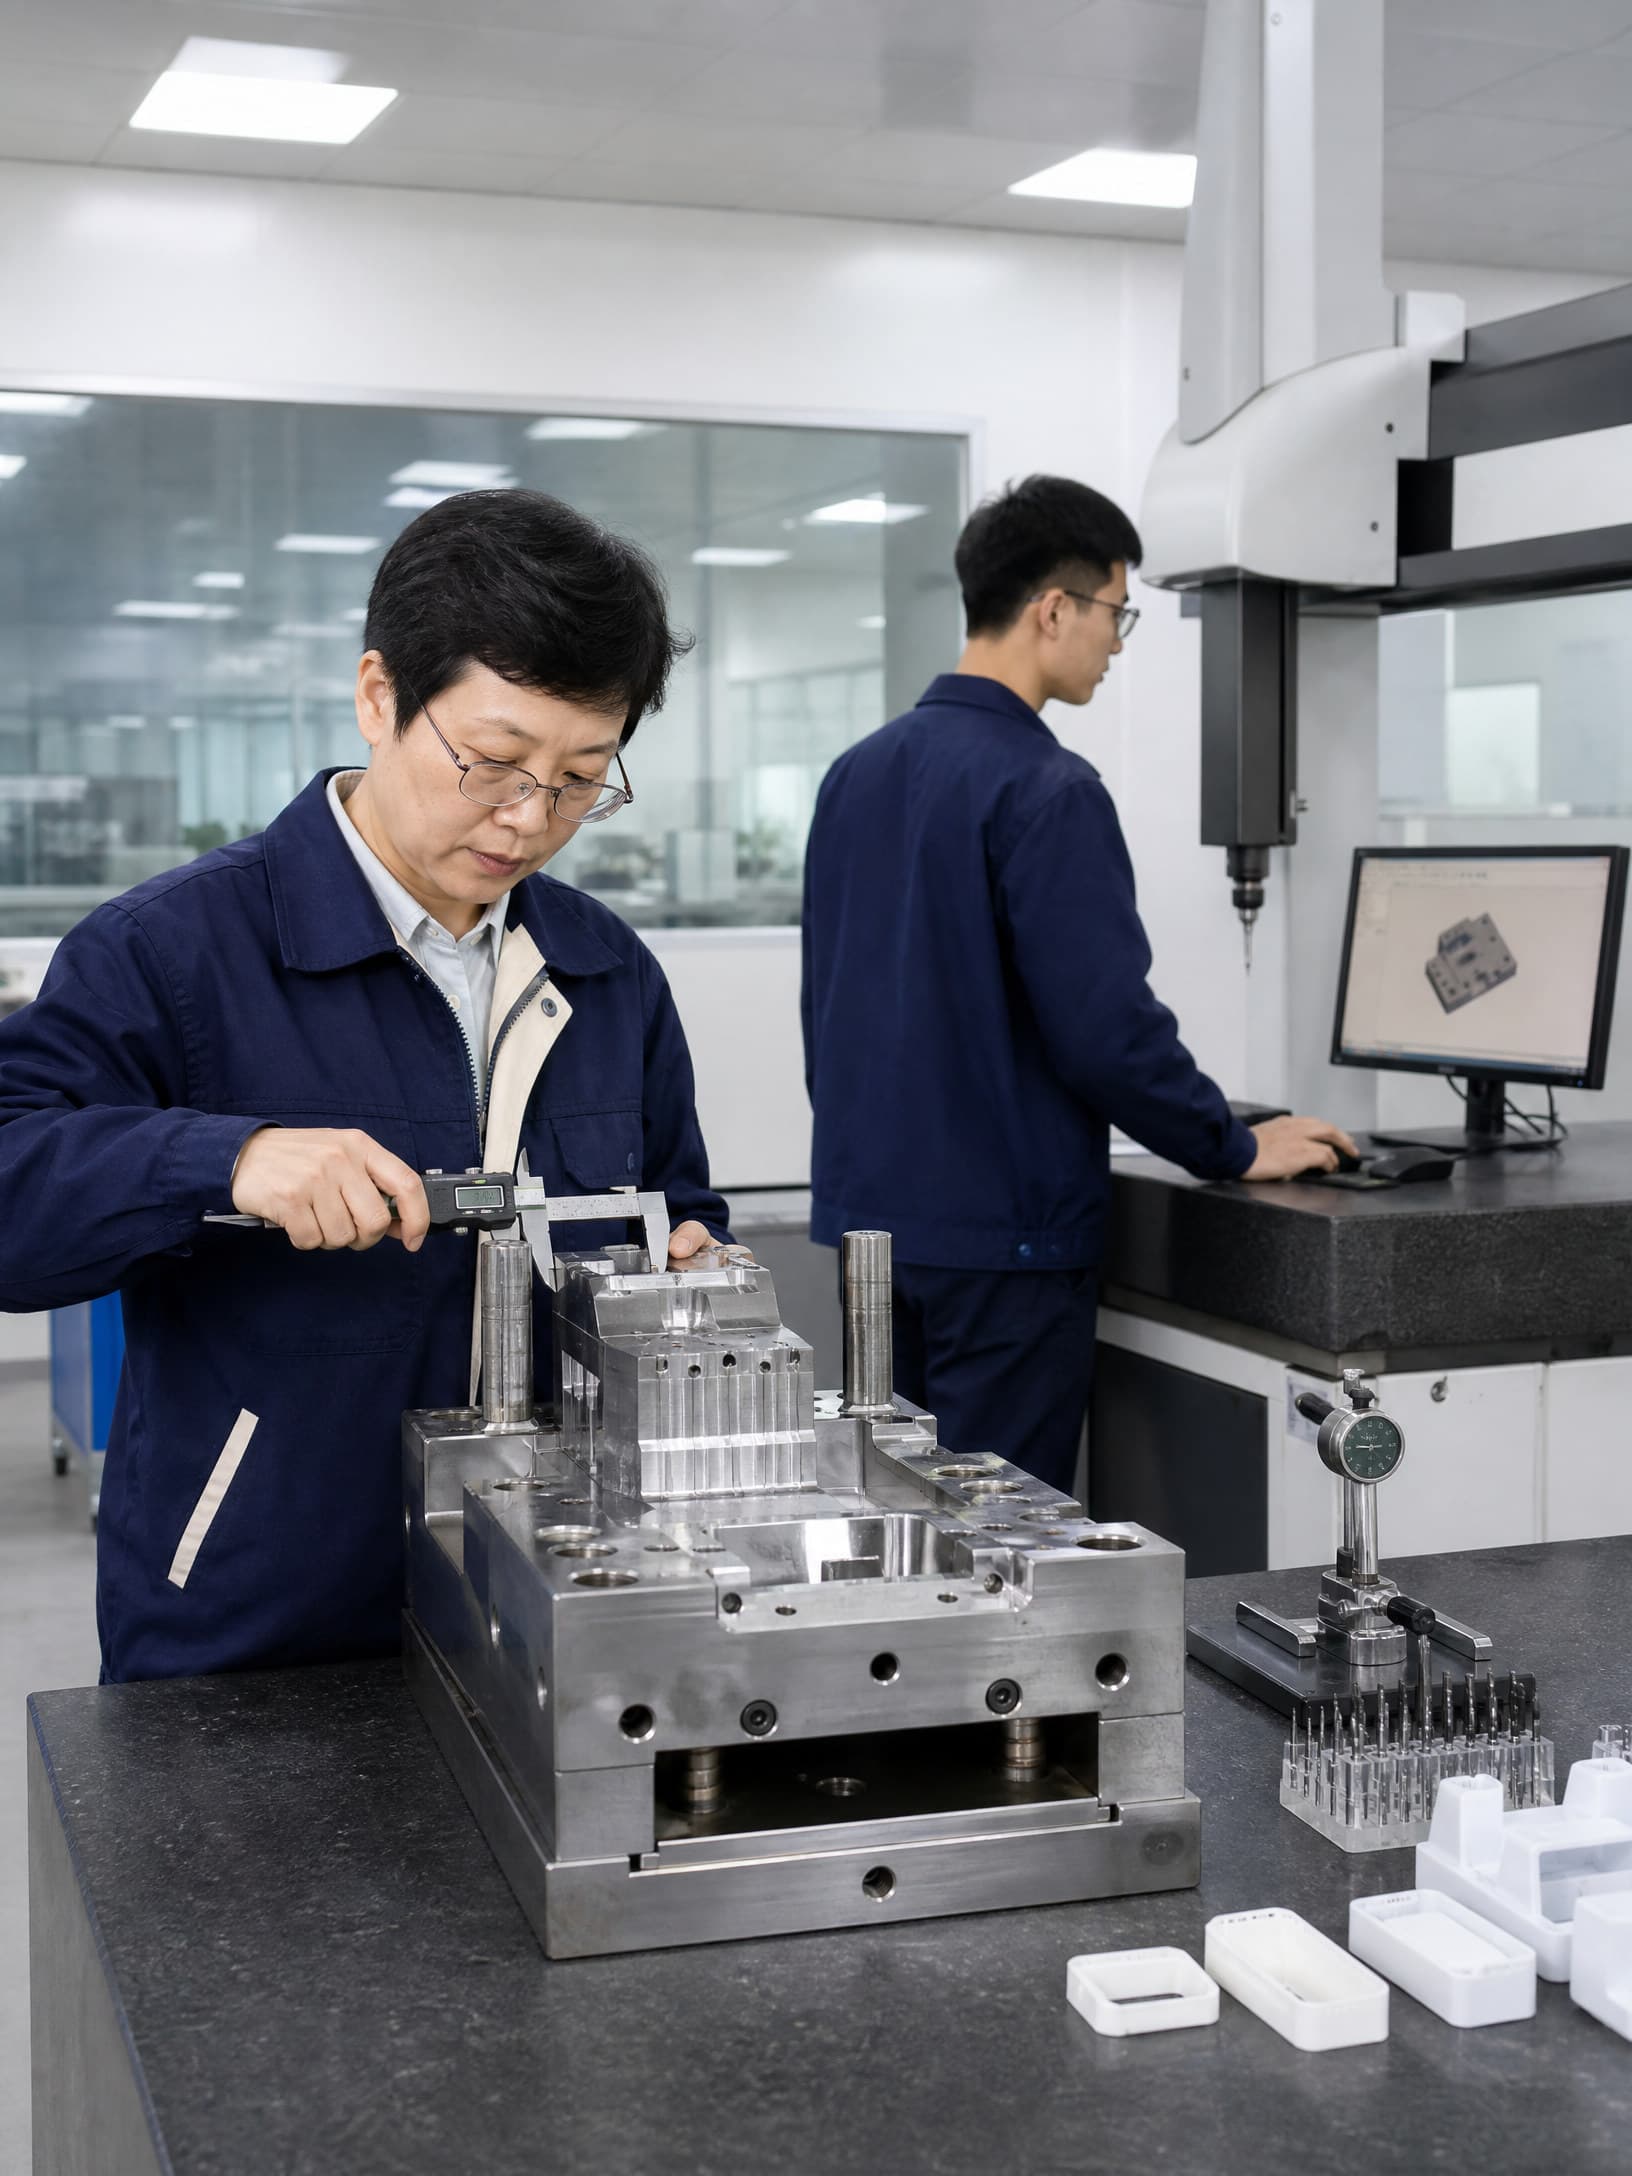
Request supplier evidence that is tied to the proposed configuration: resin manufacturer and exact grade, color and filler content; material data revision; flow and shrinkage assumptions; DFM review; core and cavity concept; mold-flow or equivalent analysis when justified; tool steel and moving-component scope; cooling and venting approach; first-article inspection plan; functional tests; and change-control commitments. A data sheet, a simulation screenshot or a sample from another tool does not establish performance for the released part.
Use approval gates. Gate 1 confirms the requirements, load cases, material direction and open assumptions. Gate 2 releases the geometry and tooling concept after disposition of core access, release, parting lines, weld lines, cooling, ejection and secondary operations. Gate 3 reviews traceable trial parts by cavity, resin lot or run, tool revision and process context. Gate 4 releases production only after dimensional, appearance, assembly and application-specific tests are accepted or formally deviated. The product owner, quality team and customer should define who can approve each gate.
05
Make the procurement decision on total risk, not hollow-shape novelty
Compare suppliers using the same information pack and require each quotation to list inclusions, exclusions, assumptions, tooling ownership, spare parts, maintenance, trial scope, inspection evidence, packaging, export responsibilities and change-notification terms. Ask how the supplier will demonstrate that the tool can be serviced and transferred. For complex cores, slides, collapsible mechanisms or specialized gas equipment, request a component-level risk register and a clear response if the first concept cannot meet the part requirement.
Do not accept universal promises about weight reduction, strength, cost, cycle time, tool life or compliance. The outcome depends on resin, fiber loading, geometry, process settings, environment, volume, equipment, tooling design and customer specifications. A specialized route may reduce material in one region but increase tool complexity, validation effort or process sensitivity. Conversely, a two-shell architecture may add an assembly step while making internal geometry and inspection more accessible. Evaluate the complete delivered part and supply chain.
Before purchase-order release, retain the approved CAD and drawing, material and color specification, tooling concept, evidence list, acceptance criteria, ownership terms, maintenance and transfer requirements, and authorized change route. Require written review before changing resin, filler, colorant, core mechanism, gate, vent, cooling, machine, process window, secondary operation or subcontractor when the change could affect approved performance. This record gives procurement, engineering and quality a defensible basis for approving or rejecting a hollowing proposal.
Practical takeaway
Before you move
to the next review.
- Define the part's load cases, allowable deflection, impact zones, openings, interfaces, environment, target volume and customer requirements before requesting a tooling quote.
- Ask the supplier to compare a conventional core-and-cavity route with any collapsible, removable, sacrificial, gas-assisted or shell-assembly alternative that could fit the geometry.
- Require the exact resin grade, filler loading, color, wall-section assumptions and evidence limits; do not approve a polymer family or generic weight-saving claim.
- Set dimensional, appearance, assembly and application-specific validation criteria, including sample condition, traceability, test method and approval owner.
- Put tooling ownership, maintenance, spare mechanisms, transfer information and written change-control triggers into the quotation and purchase-order review.
FAQ
Common questions
Can injection molding make a completely hollow plastic part?
Sometimes, but not through one universal mold design. A practical opening, split-shell architecture, moving core, removable or sacrificial core, or specialized process may be needed. Feasibility depends on the internal geometry, release direction, resin, wall distribution, volume, equipment and required performance. The supplier should demonstrate the proposed route with a part-specific DFM review and validation plan.
Does hollowing a plastic part always reduce weight?
No. Hollowing can reduce material in a defined region, but added ribs, bosses, local reinforcements, joint features, inserts or assembly flanges can offset the reduction. The resulting stiffness, impact response, buckling resistance, dimensions and process yield must be checked against the actual design. Do not approve a weight target without a controlled mass measurement and performance evidence.
Which tooling option is best for hollow injection molded parts?
There is no universal best option. A conventional core-and-cavity tool may be the simplest when the core can release through an opening. Collapsible or unscrewing cores can address restricted openings or internal threads but add mechanism and maintenance risk. Removable cores, gas-assisted molding or joined shells may suit other geometries. Compare the complete tool, process, validation and lifecycle cost for the specific part.
What evidence should an OEM request before approving a hollow-part mold?
Request a controlled DFM review, named resin and filler, core and cavity concept, flow or process analysis where justified, cooling and venting rationale, ejection plan, tooling risk register, first-article inspection plan, functional tests and change-control commitments. Evidence should be traceable to the tool revision, material, cavity or run and the released part requirements.
References
Source material
- [1] ASTM International — ASTM D955-21, Standard Test Method of Measuring Shrinkage from Mold Dimensions of Thermoplastics
- [2] Autodesk — Moldflow: Injection and Compression Molding Simulation Software
- [3] ISO — ISO 294-1:2017, Plastics — Determination of moulding shrinkage
- [4] NIST — Dimensional Metrology
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.