
Gas-assist injection molding can reduce resin in selected thick sections by using pressurized nitrogen to form an internal hollow path while the part is molded. That does not make every component lighter, cheaper, stronger or faster to produce. For an overseas OEM, the buying decision is whether the process can meet the required stiffness, impact, dimensional, cosmetic, durability and compliance targets at the intended resin grade, geometry, volume and tool concept. The right comparison is therefore not gas assist versus conventional molding in the abstract. It is a controlled comparison of validated part designs and manufacturing assumptions.
Decision rule: approve a gas-assist concept only after the supplier shows how the gas path, resin grade, wall sections, tooling and process window will deliver the specified part-level requirements.
01
What gas-assist molding changes—and what it does not guarantee
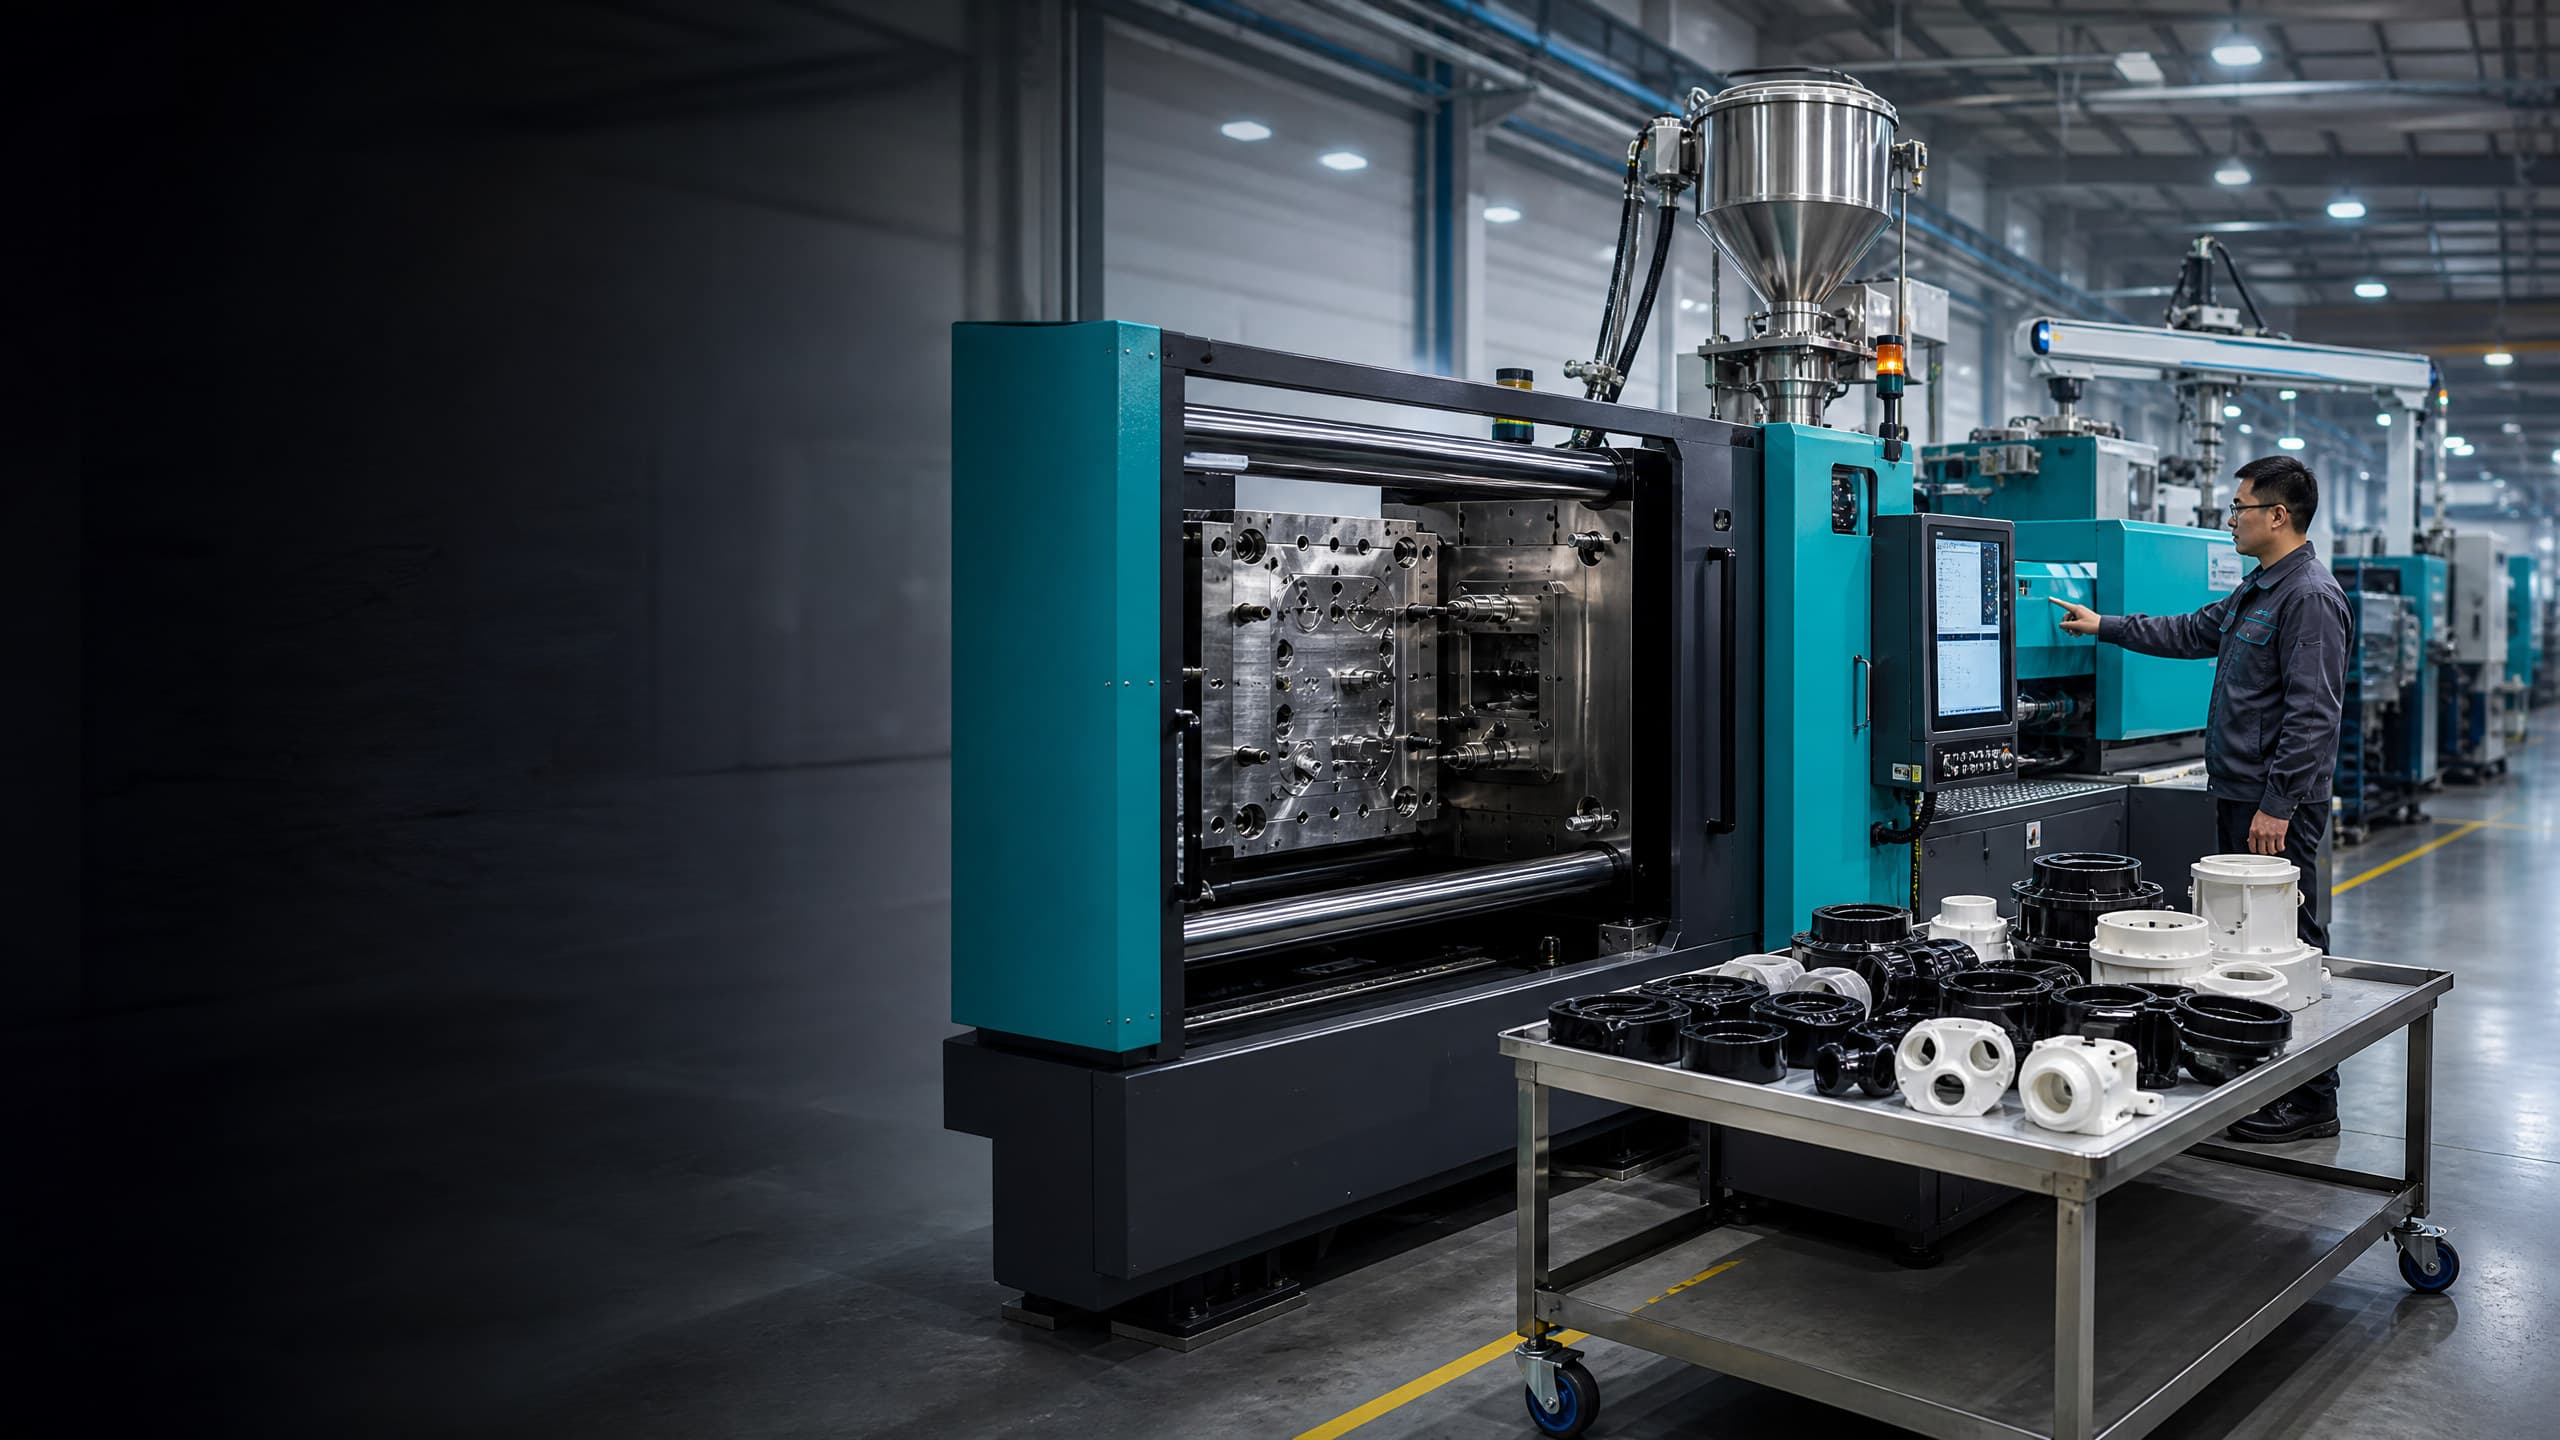
In a typical short-shot process, molten resin partially fills the cavity and nitrogen is then introduced through a gas pin, runner or nozzle route. The gas displaces resin through designed channels and can remain under pressure while the part cools. This can create a hollow section, support packing in selected areas and reduce sink-related risk when the geometry and process are suitable.[1] [2]
The potential weight reduction comes from removing resin, not from making the remaining polymer intrinsically stronger. A hollow beam can retain useful bending stiffness because material is placed away from its neutral axis, but local buckling, impact damage, fastener pull-out, weld lines, joints and end transitions may govern performance. The finished result depends on resin family and grade, filler or fiber loading, geometry, gas penetration, processing, environment, production volume and customer specifications. Require part-level evidence rather than accepting a percentage claim copied from another application.
Lightweighting can also change the design balance. Less mass may reduce inertia, but a thinner or hollow section can reduce local crush resistance, acoustic behavior or thermal mass. Gas assist may reduce residual stress and sink marks in some designs, yet it can introduce risks such as gas fingering, blow-through, incomplete filling, uneven hollow-wall thickness and variable end-of-channel behavior. These are engineering questions to resolve, not reasons to assume the process will fail.
02
When is gas assist a good fit for a buyer's part?
The process is most worth screening when the design contains thick ribs, bosses, handles, rails, beams, frames or other connected sections where conventional molding would require excess resin, high pack pressure, visible sink control measures or a separate coring operation. The gas route needs a predictable flow path. Abrupt thickness changes, isolated thick features, very thin sections, sealed-off pockets and complex branched geometry may require redesign or may be poor candidates.
Use requirements to define fit. Requirements should state loads, deflection limits, impact conditions, fatigue or cycle expectations, operating temperature, chemical exposure, appearance zones, allowable hollow regions, interfaces, target mass, annual volume and any customer or regulatory specification. Recommendations can then address candidate resin, gas-entry method, channel layout, wall transitions, venting and tooling. Do not convert a recommendation such as “use a thick gas channel” into a universal dimensional rule without a part-specific review.
A supplier should compare at least one conventional baseline with the gas-assist concept. The comparison should identify resin mass, part mass, stiffness and strength test methods, dimensional results, warpage, appearance, cycle assumptions, tooling changes, gas equipment requirements, scrap risk and unit-cost assumptions. A lower quoted part price is not meaningful if it excludes specialized controls, additional trials, inspection or a new tool concept.
| Buyer question | Evidence to request | Approval implication |
|---|---|---|
| Can the design carry the required load after hollowing? | FEA assumptions, section map, molded-part stiffness and impact results at the proposed resin and process. | Do not approve geometry from resin data alone; release only against defined part-level criteria. |
| Will the gas reach the intended areas consistently? | Gas-path simulation or engineering rationale, gas-entry locations, venting plan and trial evidence. | Require a documented response for dead ends, branches and transition zones. |
| Will dimensions and appearance remain acceptable? | Warpage study, cavity or part measurement plan, surface photos, sink and gas-mark criteria. | Set CTQs and cosmetic acceptance before tool release. |
| Is the business case real at the planned volume? | Baseline and gas-assist tooling quotes, cycle assumptions, equipment scope, scrap and maintenance assumptions. | Compare total cost of ownership, not resin cost alone. |
| Can production changes be controlled? | Material traceability, process-window proposal, cavity identification and change-notification plan. | Make grade, tool, gas-control and process changes approval-controlled. |
03
How lightweighting affects stiffness, impact, shrinkage and warpage
Stiffness is a system result. Section depth, hollow-wall thickness, ribs, end closures, fiber orientation, weld lines, supports and attachment points can matter as much as nominal mass. A reinforced resin may increase stiffness in one direction while increasing anisotropic shrinkage and warpage. A non-reinforced resin may offer different impact behavior or surface quality. Ask the supplier to identify the load path and the locations where gas penetration could reduce section or create a discontinuity.
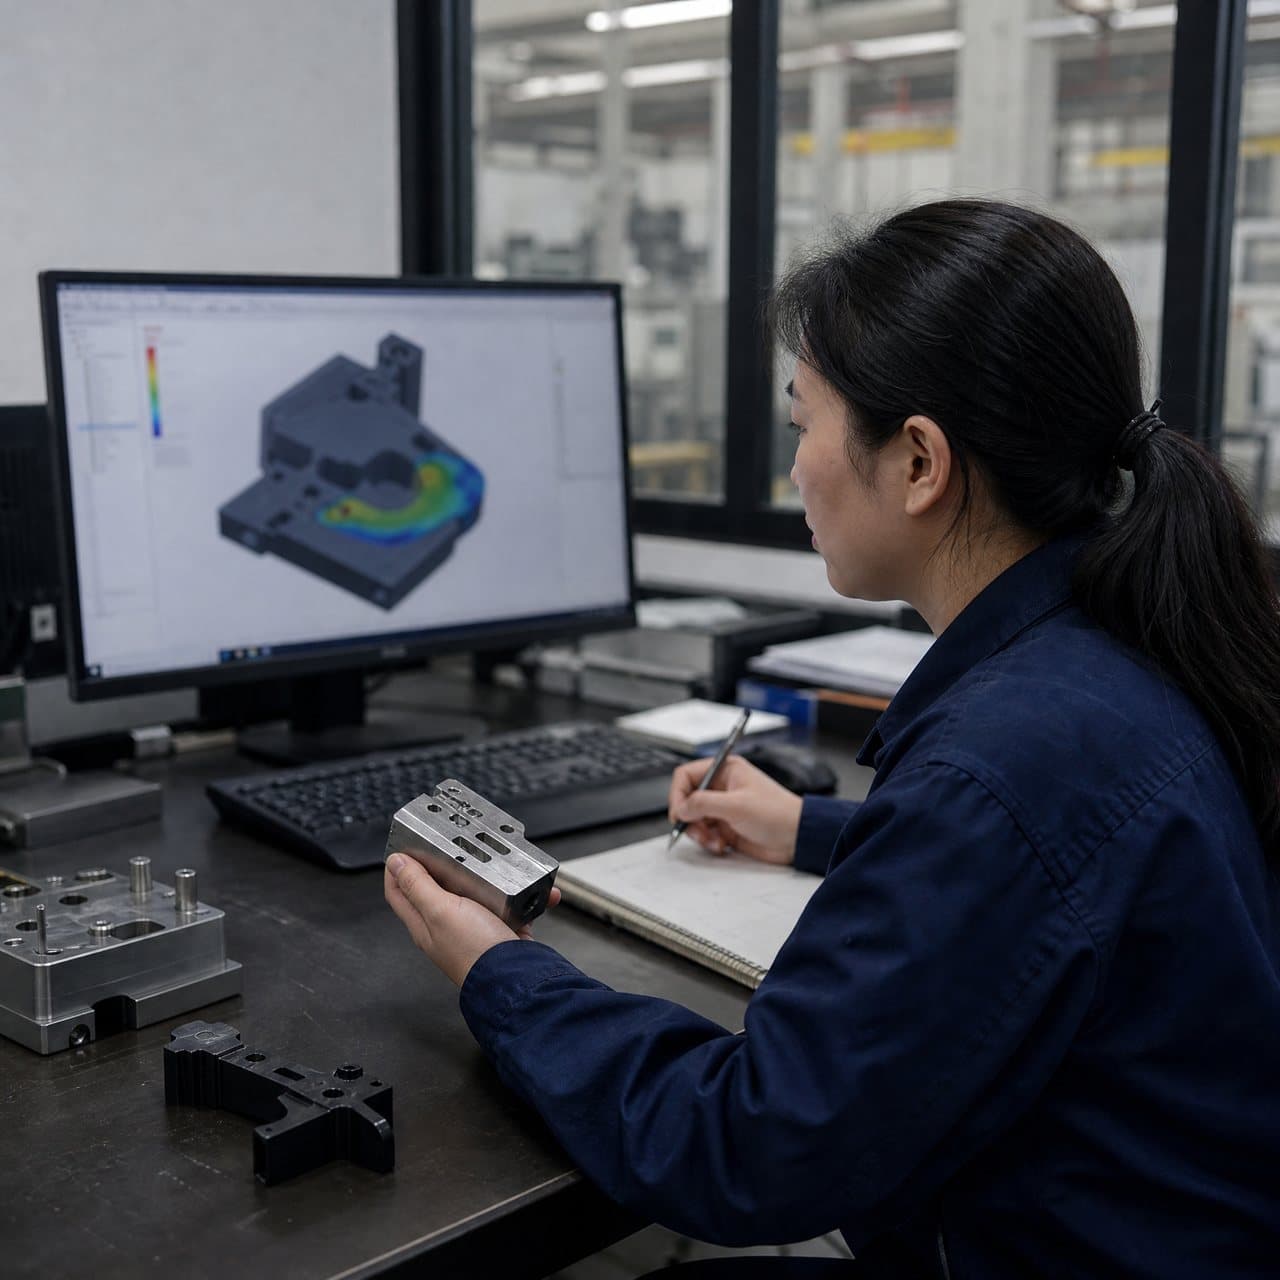
Shrinkage and warpage should be assessed with the selected grade, color, filler or fiber content, mold temperature, cooling layout and gas-pressure profile. Gas pressure can compensate for volumetric shrinkage in some regions, and internal gas cooling may affect residual stress, but neither effect is universal. Warpage can remain at transitions, unbalanced walls, fiber-oriented regions, inserts, gates or cooling-imbalanced areas. Use simulation as a design aid and verify the molded parts with a defined measurement method.[1]
Impact and durability validation should represent the assembled product and environment. Test the gas-assist part against the conventional baseline where that comparison informs the decision, including low-temperature impact where relevant, repeated loading, fastener or insert loads, drop or abuse conditions and conditioning or chemical exposure. The product owner must define pass/fail limits; a supplier should not infer them from a generic material data sheet.
04
Tooling, resin and process questions to resolve before an RFQ decision
Gas assist changes the mold conversation. The tool may need gas pins or a nozzle route, controlled vents, suitable seals, channel-friendly cooling and access for maintenance. The parting line, gate, ejectors, overflow or vent trim, texture and cosmetic surfaces must be reviewed together. Ask whether the proposed layout is compatible with the machine, gas controller, mold protection, cavity count and anticipated production rate. Tooling recommendations remain geometry- and volume-dependent.
Name the exact resin manufacturer and grade direction, including reinforcement, color, recycled content, flame or other customer requirements. Resin viscosity, melt stability, drying or conditioning needs, fiber loading and shrinkage behavior influence gas penetration and dimensional results. Ask for the current technical data, processing guidance, relevant wall-section evidence and known limitations. Do not approve a polymer family or “equivalent” grade without written evaluation.
At RFQ, require the supplier to state the assumed shot method, resin dose, nitrogen source and control method, gas pressure and timing strategy, venting, cooling, expected cycle, trial plan, scrap assumptions, inspection equipment, sample quantity and responsibilities. Distinguish requirements from recommendations in the quote. If the supplier proposes geometry changes, request marked-up CAD, the reason for each change and the effect on weight, stiffness, tooling, appearance, assembly and cost.
05
Use staged approval gates instead of approving a process promise
Gate 1 is requirements alignment. The OEM approves the controlled CAD and drawing revision, target mass or mass range, load cases, interfaces, cosmetic zones, environment, resin direction, volume scenario, compliance context and acceptance criteria. Open items should be listed as open. A supplier's recommendation is not a substitute for the product owner's requirement.
Gate 2 is DFM and tooling release. Review the gas-path concept, resin entry, gas entry, vents, overflow or trim, cooling, ejection, weld lines, hollow-wall thickness, transitions, tolerances and inspection datums. Approve the tool only after the main risks have an owner and a disposition. If CAE is used, record the material data, assumptions, boundary conditions and version so the analysis can be compared with trials.[1]
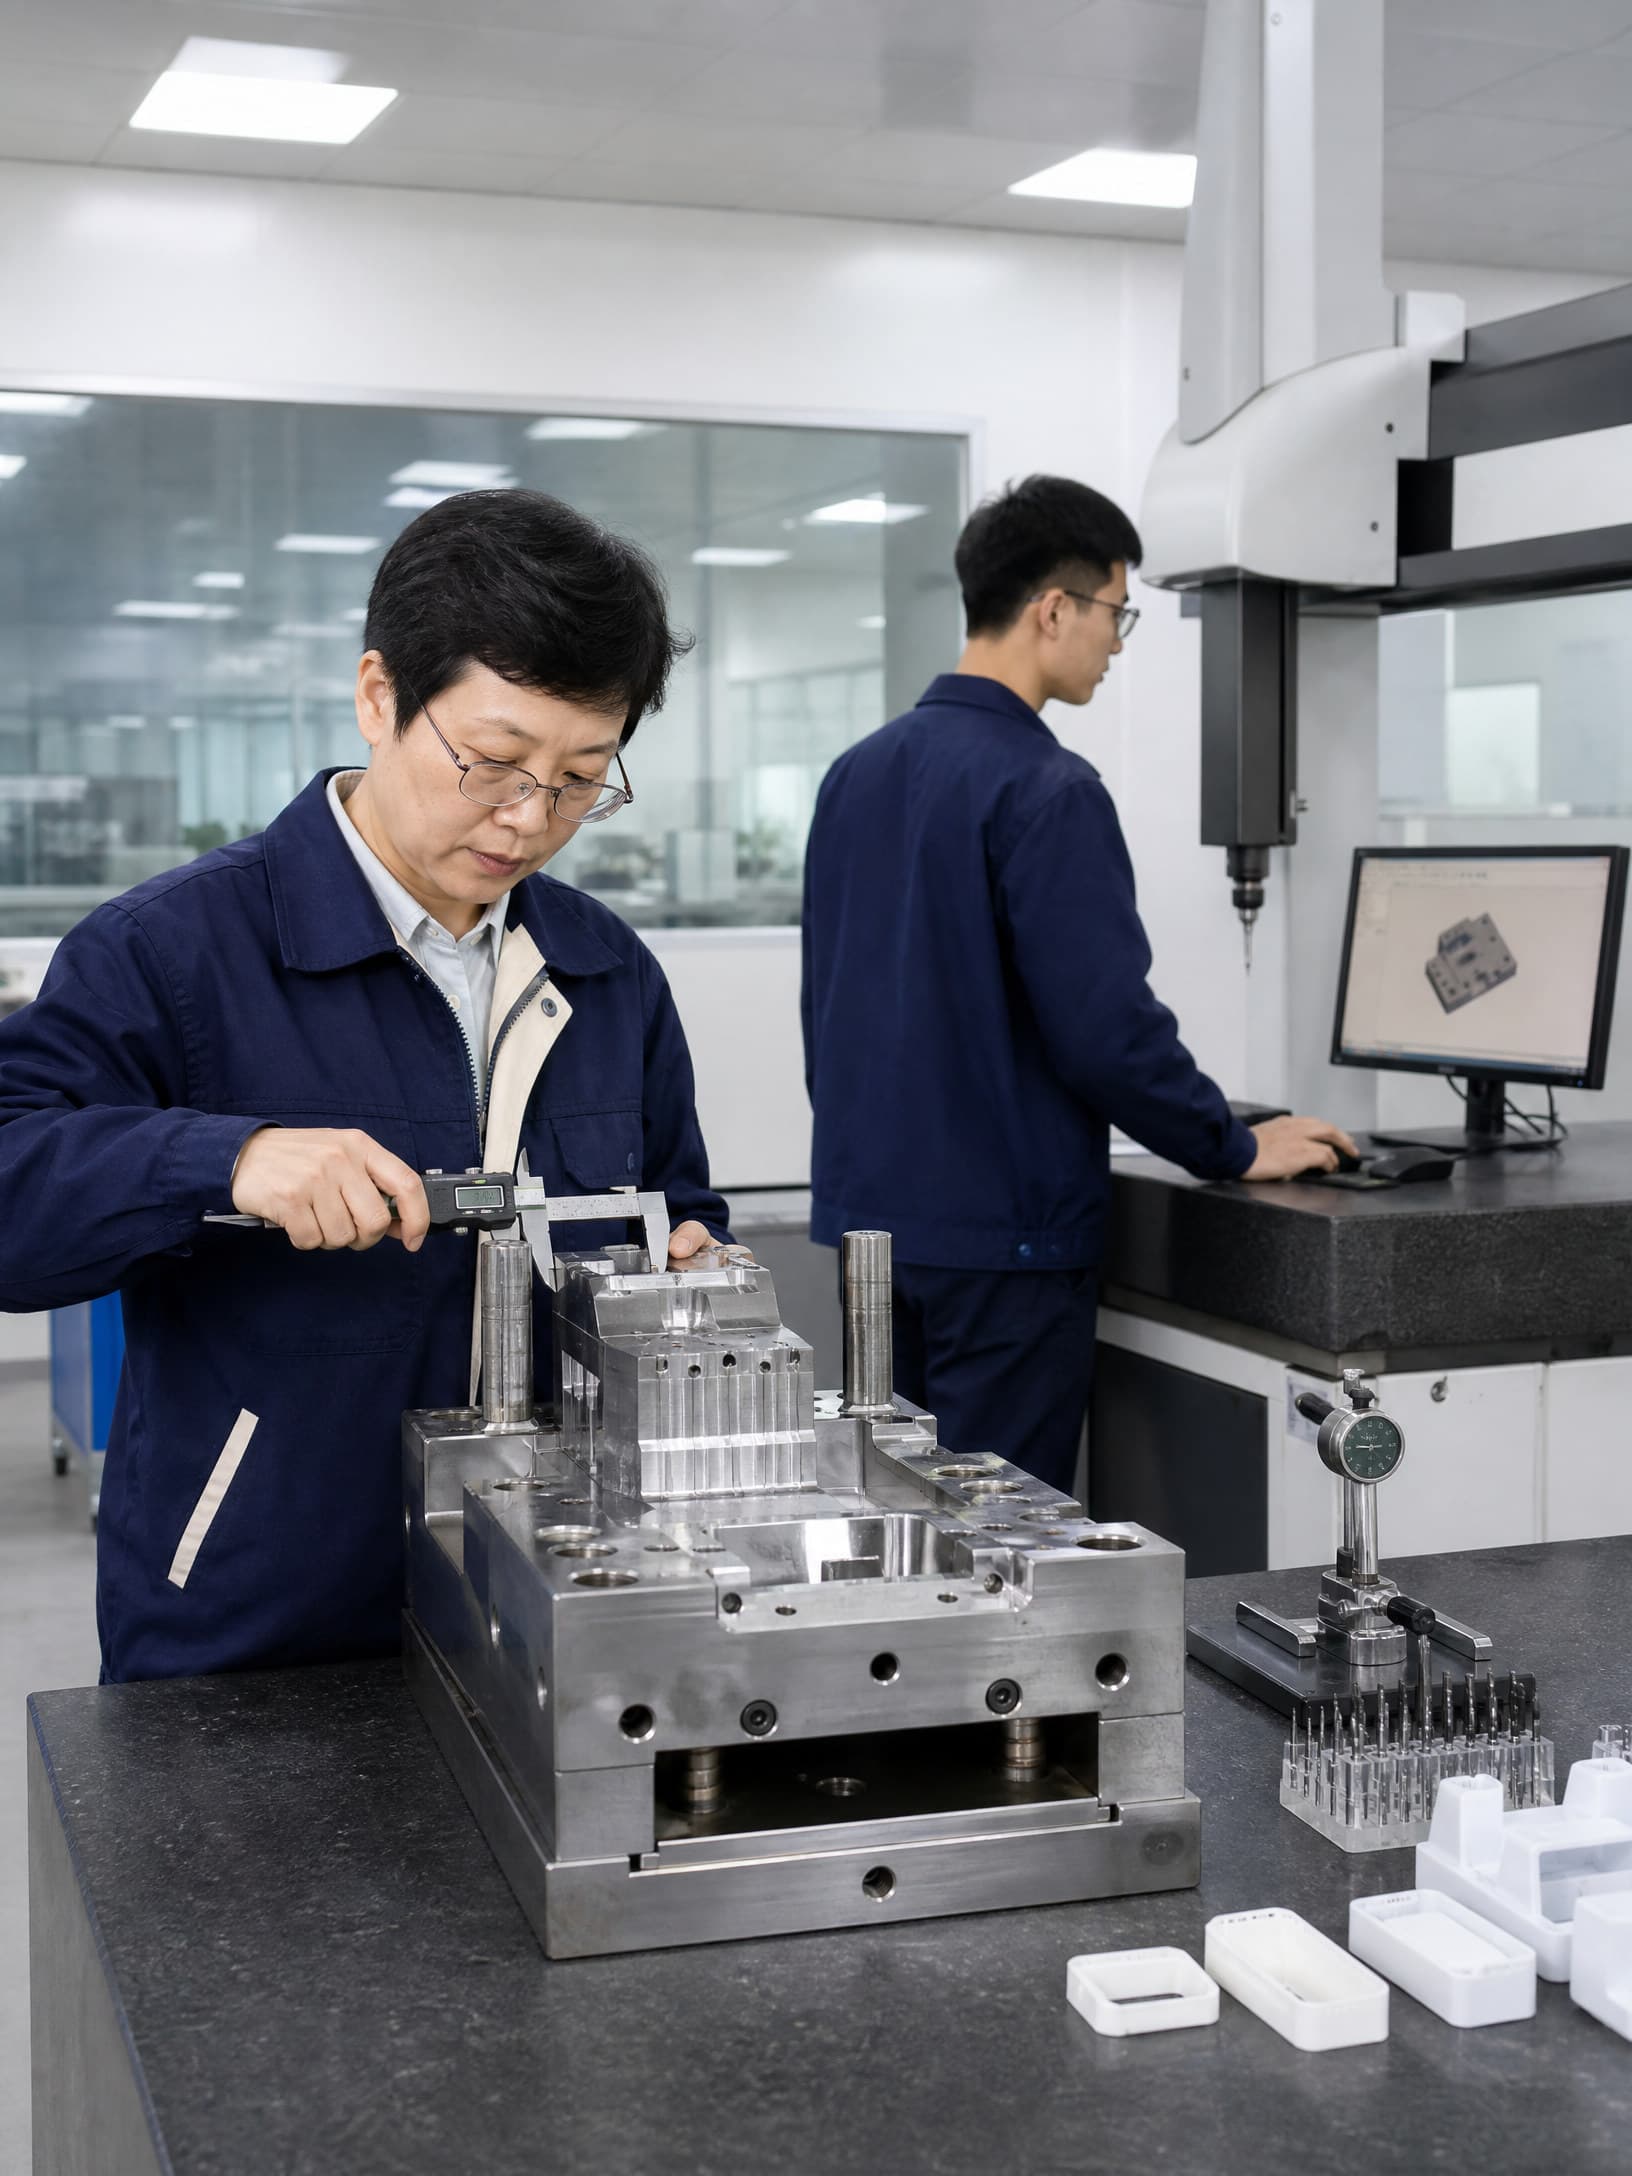
Gate 3 is traceable first-article and validation approval. Parts should be linked to the tool, cavity, resin grade, color, machine, process window and trial date. Measure critical dimensions and mass, inspect surfaces and section evidence where practical, and run the agreed stiffness, impact, durability, environmental and assembly tests. Gate 4 is production release and change control. Define notification triggers for resin, supplier, colorant, fiber loading, tool repair, gas controller, machine, cavity, geometry or process-window changes.
Practical takeaway
Before you move
to the next review.
- Define load, stiffness, impact, durability, environment, appearance, mass, volume and customer-specification requirements before selecting gas assist.
- Ask for a conventional baseline and a gas-assist concept with stated resin, geometry, tooling, cycle, scrap and total-cost assumptions.
- Require gas-path, hollow-wall, venting, cooling, warpage and transition-risk evidence for the controlled part revision.
- Approve the exact resin grade, reinforcement, color and processing controls; do not accept a polymer family or equivalent-grade claim alone.
- Use documented gates for requirements, DFM/tool release, traceable first articles, validation and post-release change control.
FAQ
Common questions
Does gas-assist injection molding always reduce part weight?
No. It can reduce resin in suitable thick or channel-forming regions, but the achievable result depends on resin, geometry, gas penetration, wall requirements, tooling, process control, volume and customer specifications. The target should be confirmed by comparing molded parts, not by applying a universal percentage.
Will a lighter gas-assist part be as strong as a solid molded part?
Not automatically. A well-placed hollow section can preserve useful stiffness, but local impact, buckling, fatigue, weld lines, attachments and end transitions may change. Define the load cases and validate the actual molded and assembled part against the required limits.
Is gas assist cheaper than conventional injection molding?
It may reduce resin use or enable a different tool and machine strategy, but specialized gas equipment, controls, tooling, trials, inspection and scrap can change the economics. Request a scope-normalized total-cost comparison at the planned volume and ramp.
What should an OEM request from a gas-assist supplier before tooling?
Request the exact resin and grade, gas-path and tool concept, shot and gas-control assumptions, CAE or engineering rationale, DFM risks, baseline comparison, validation plan, inspection method, traceability plan, commercial exclusions and change-control commitments. Approval should follow documented gates rather than a verbal weight-saving claim.
References
Source material
- [1] Asahi Kasei Plastics, Part 8: Application to Gas-assisted injection molding
- [2] Bauer Performance Technology Group, The Gas Assist Process
- [3] Xometry, Gas-Assisted Injection Molding
- [4] SABIC, Injection Molding Design Guide
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.