
Injection-molded ribs can increase bending stiffness or support a mounting feature without making an entire plastic component solid and heavy. For an overseas OEM, however, a rib is not a universal strength multiplier: its value depends on the load direction, resin modulus, fiber loading, wall and root geometry, flow history, temperature, impact requirement, assembly interfaces and customer specification. A rib that improves a bench stiffness result may also create sink, weld-line sensitivity, anisotropic shrinkage, warpage or difficult ejection if it is added without a complete design review.
The buying decision is therefore not simply whether a part has ribs. It is whether the proposed rib layout delivers the required function at an acceptable mass, appearance, dimensional and manufacturing risk, and whether the supplier can prove that result on the released configuration.
Requirement: define the load case, stiffness or deflection limit, impact environment, mass target and interfaces. Recommendation: use rib networks, coring and gradual transitions as candidate solutions, then approve them through part-level analysis and testing.
01
What a rib changes—and what it cannot guarantee
A rib increases the effective section depth and can move material away from a neutral axis, which may improve bending stiffness more efficiently than adding material uniformly to a broad wall. It can also stabilize a cover, support a fastener boss, reduce panel oil-canning or transfer a local load toward a mounting point. These are design mechanisms, not guaranteed outcomes. The result depends on rib height, thickness, length, orientation, spacing, root radius, attachment to the parent wall and the direction and duration of the applied load.
Separate requirements from recommendations at the start. The drawing or product specification should state allowable deflection, strength or fatigue target, impact condition, mass range, critical interfaces, cosmetic zones, temperature and chemical exposure, and any customer or regulatory requirements. Engineering may then recommend a rib layout, a cored section, a gusset, a thicker local wall or a different resin. The selected option must be checked at the assembled-part level because fasteners, inserts, seals, neighboring parts and boundary conditions can dominate the response.
Lightweighting can also reduce material usage, but buyers should not promise a fixed weight, cost or cycle-time reduction before the geometry, resin, tooling, annual volume and process window are known. A ribbed design may require more complex slides, lifters, venting or ejection, and a fiber-reinforced grade may improve modulus in one direction while increasing flow-direction shrinkage and warpage risk. Confirm the trade-off with analysis, samples and a production-representative process.
02
Select rib geometry with molding, shrinkage and appearance in mind
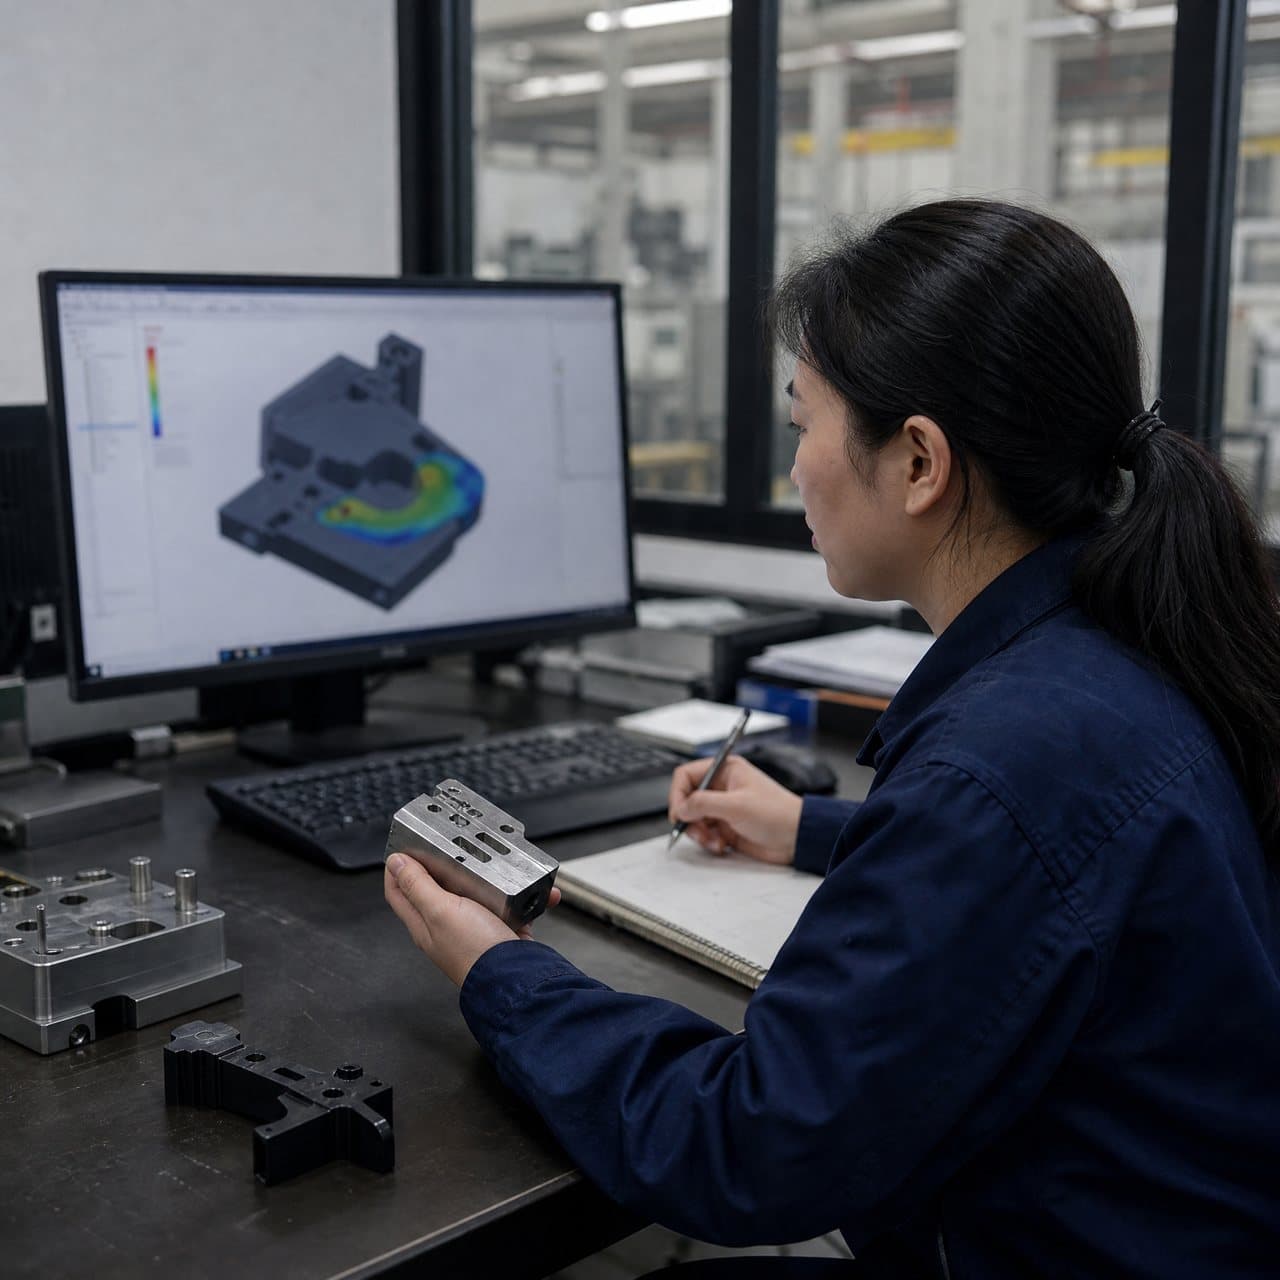
Start with a reasonably uniform parent wall and transition into the rib with a controlled root rather than a sharp corner or a large mass concentration. A common design recommendation is to keep rib thickness below the adjacent nominal wall—often around 40% to 60% as an initial range—to reduce sink and void risk, but this is not a release rule. The useful value depends on resin grade, color, texture, flow length, cooling, packing, rib height and the functional load. Request a resin-specific DFM review instead of applying a generic ratio automatically.
Rib height, draft, spacing and orientation should be reviewed together. Tall or closely spaced ribs can restrict filling, trap air, complicate ejection and amplify local cooling differences. Draft and suitable root and tip radii support release and reduce stress concentration, but the appropriate values depend on texture, tool direction and the selected tool concept. Where a local intersection is thick, coring, a lighter gusset arrangement or a smooth transition may preserve the required function with less shrinkage mass.
The visible opposite surface matters. A rib can telegraph a sink mark, read-through or gloss change on a cosmetic face even when the rib itself is hidden. Gate position, weld lines, packing and cooling can also change the result. Agree cosmetic zones, viewing conditions and acceptance samples before steel release; do not assume that a technically strong rib is acceptable on every surface.
| Design decision | Potential benefit | Main risk to investigate | Buyer evidence request |
|---|---|---|---|
| Thin, drafted rib connected to a uniform wall | Adds local section depth with limited added mass | Insufficient stiffness, short shot, weld line or ejection drag if too tall or thin | Section map, fill/ejection review and functional deflection result |
| Gusset or triangulated rib network | Supports a boss or load path without a broad solid pad | Local mass at intersections, sink, stress concentration and difficult venting | Root-transition detail, sink-risk assessment and sample inspection |
| Cored thick area with separate ribs | Reduces concentrated material while retaining an external envelope | Loss of strength, tooling access limits, knit lines or thin-wall filling demand | CAD section review, tool concept and part-level load validation |
| Glass- or mineral-filled resin | May increase modulus or dimensional capability for a defined direction | Anisotropy, fiber-related warpage, abrasive tooling and surface change | Exact grade, fiber content, flow orientation assumptions and conditioned test data |
03
Match resin and process choices to the real structural load
Resin selection should follow the load case and environment, not the word structural alone. Unfilled and reinforced thermoplastics have different modulus, impact behavior, creep, moisture response, shrinkage and processing windows. A reinforced grade may be attractive for stiffness or heat resistance, yet its properties can differ substantially parallel and transverse to flow. For a part exposed to sustained load, temperature cycling, impact, vibration or chemicals, request data relevant to the intended condition rather than relying only on room-temperature short-term values.
The molding process affects rib performance. Flow around a rib, through an opening or past a boss can create weld lines and orientation changes. Gate location, fill speed, packing, venting, mold temperature, cooling balance and resin drying or conditioning may influence voids, shrinkage, surface appearance and dimensions. The process recommendation must be tied to the exact grade, geometry, machine, cavity strategy and approved process window; a supplier should not present one universal setting or tolerance as a guarantee.
For procurement, ask for the proposed resin manufacturer and exact grade, color, reinforcement level, current technical data, relevant conditioning state, recycled-content or substitution policy where applicable, and the limits of the evidence. If the part is safety-related or load-bearing, define who owns the structural analysis, environmental conditioning, fatigue or impact test, and final release decision.
04
Control tooling, dimensional stability and validation gates
Tooling must accommodate the rib network as well as the nominal outer shape. Review parting direction, draft, shutoffs, slides or lifters, core cooling, vent locations, ejection forces, gate and runner balance, insert strategy and tool steel access. Ribs may increase the projected area or create local pressure and cooling demands, while deep narrow features can complicate polish, texture and maintenance. A mold-flow or equivalent engineering study can help compare concepts, but its predictions depend on the input material data, mesh, assumptions and boundary conditions.
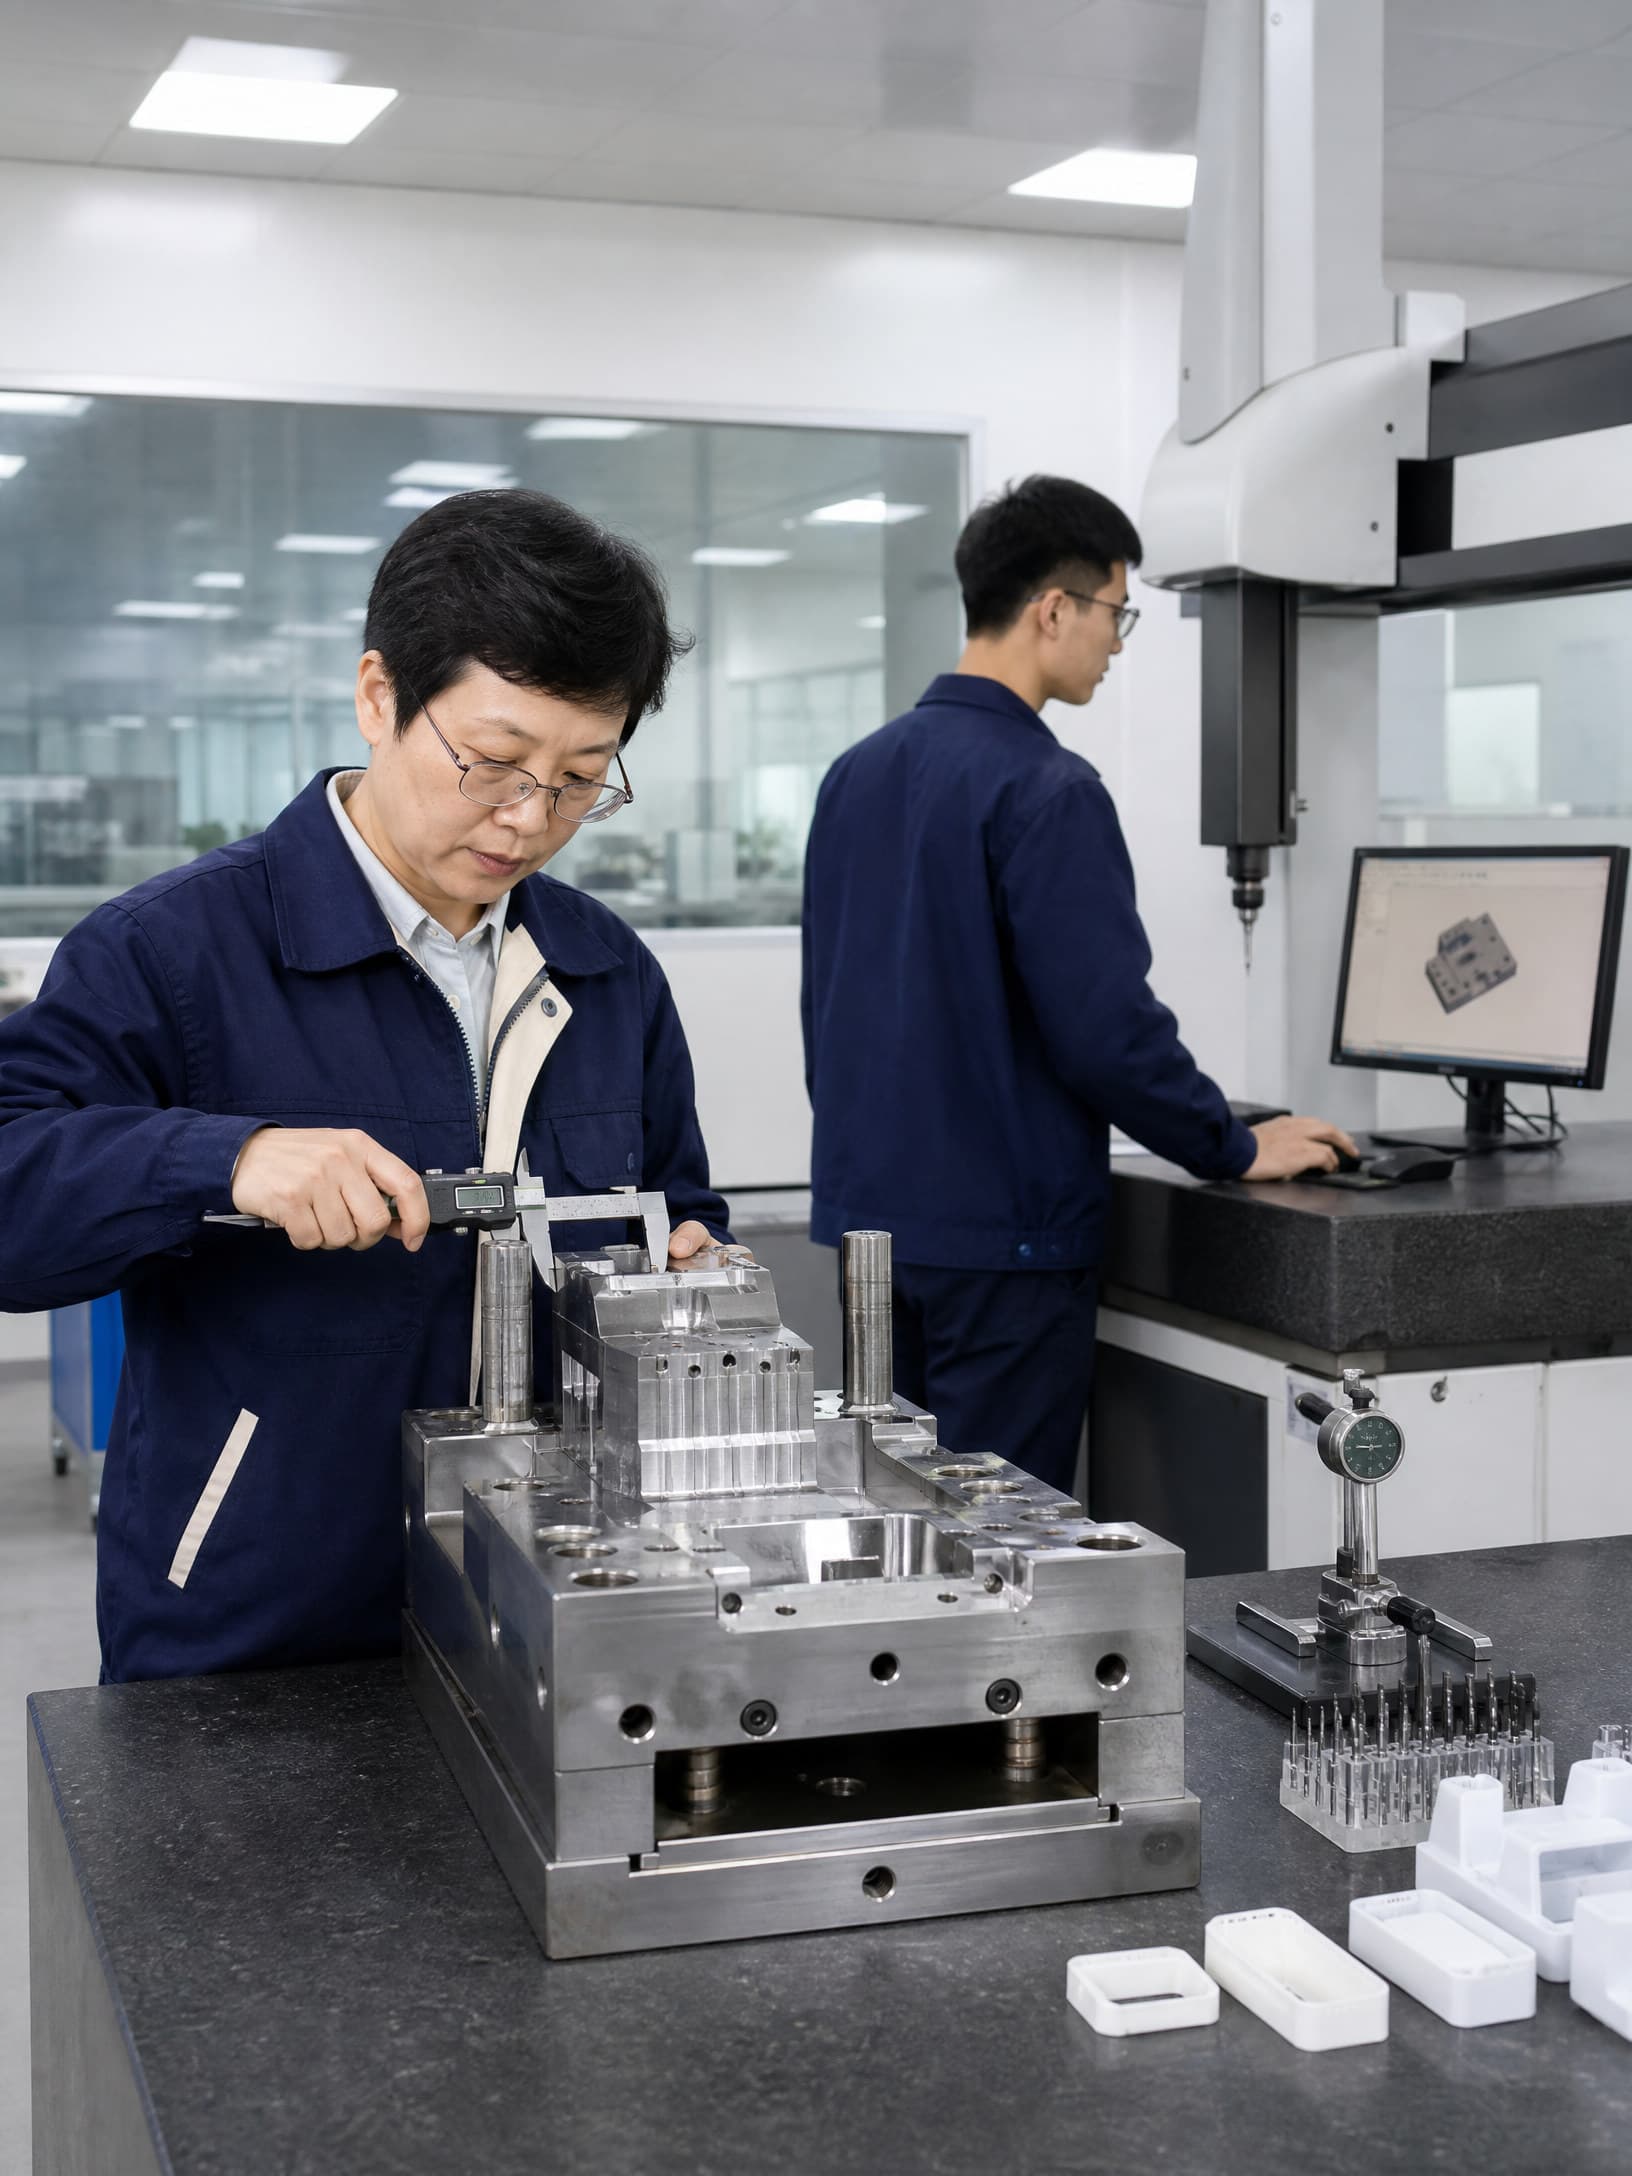
Shrinkage and warpage should be treated as a system outcome. Resin type, fiber orientation, wall transitions, rib placement, packing, cooling, ejection and post-molding conditioning can all contribute. Establish datum strategy and critical-to-function dimensions before tooling. Measure the actual part from a traceable cavity and material lot under an agreed condition; do not approve a ribbed design solely from a simulation image or an isolated material plaque.
Use approval gates. Gate 1 confirms requirements, load cases, mass target, resin direction and critical interfaces. Gate 2 releases DFM and tooling only after rib geometry, ejection, gate, venting, cooling and warpage risks have documented dispositions. Gate 3 reviews traceable first articles, dimensional results, appearance, assembly and functional or structural tests. Gate 4 authorizes production after the customer accepts the evidence and any deviations. Changes to grade, fiber content, color, CAD, tool, cavity, machine, process window or assembly should trigger documented impact review before shipment.
05
Make supplier comparison evidence-based for an overseas OEM
A useful RFQ package includes the controlled CAD and drawing revision, load direction and boundary conditions, deflection or strength criteria, mass target, cosmetic zones, target annual volume, service environment, assembly details, preferred or prohibited materials and required markets. Ask each supplier to identify assumptions and exceptions rather than hiding them inside a price or lead-time estimate. Tooling concept, cavity count, proposed gate strategy and validation scope should be compared on the same product definition.
Request evidence that can be audited: exact resin and data-sheet revision; material certificates or lot traceability as applicable; DFM mark-up; rib and wall-section map; analysis assumptions; sample plan; measurement method; process-window proposal; dimensional and appearance reports; functional test results; and a change-notification commitment. Ask how the supplier will segregate approved material, cavities and revisions, and how nonconforming or substituted material will be controlled.
Compare suppliers on risk transparency, not on a claimed universal weight saving, lowest unit price or fastest cycle. A credible proposal explains where a rib improves the load path, where it introduces molding risk, what is still unknown and how the team will close that gap. Final suitability remains dependent on resin, fiber loading, geometry, processing, environment, volume and customer specifications; the OEM product owner must make the release decision.
Practical takeaway
Before you move
to the next review.
- Define the load case, allowable deflection or strength target, impact and fatigue conditions, environment, mass target and critical interfaces before approving a rib concept.
- Review rib thickness, height, draft, root radius, spacing, intersections and opposite cosmetic surfaces with the exact resin grade and tool direction.
- Request grade-specific evidence covering modulus, creep, impact, shrinkage, fiber orientation, conditioning and chemical or temperature exposure where relevant.
- Require documented DFM, tooling, flow, cooling, ejection, dimensional and warpage reviews before tool release; treat generic rib ratios as starting guidance only.
- Set approval gates for requirements, DFM/tooling, traceable first articles and customer release, with change control for material, geometry, tool, process and assembly changes.
FAQ
Common questions
Do injection-molded ribs always reduce the weight of a structural plastic part?
No. Ribs can improve stiffness more efficiently than uniformly thickening a wall, but the final mass depends on the baseline geometry, load case, resin, rib network, tooling and required safety margin. A rib may also require local gussets, draft or thicker intersections. Confirm any weight change from released CAD and measured parts rather than assuming a universal saving.
What is a good rib thickness-to-wall ratio for injection molding?
A ratio around 40% to 60% of the adjacent wall is often used as an initial design discussion, particularly to reduce sink risk, but it is not a universal approval rule. The appropriate ratio depends on resin grade, color, texture, flow, packing, cooling, rib height, root geometry and load. Use the supplier's grade-specific DFM review and inspect the actual molded part.
Are glass-filled plastics always better for lightweight structural ribs?
No. Reinforcement can increase modulus or strength in a defined direction, but it can also increase anisotropic shrinkage, warpage, surface effects, tool wear and sensitivity to flow orientation. Moisture and temperature can also change performance for some resin families. Select the exact grade against the complete load and environment, then validate the molded and conditioned part.
What should an OEM ask an injection molding supplier before approving ribbed parts?
Ask for the exact material grade and reinforcement, DFM section map, tooling and gate concept, flow or warpage assumptions, ejection and cooling review, traceability plan, first-article measurements, appearance criteria and functional or structural test evidence. Agree approval gates and require written impact review for material, CAD, tool, cavity, process or assembly changes.
References
Source material
- [1] BASF — Design and Processing Guidelines for Ultramid (polyamide) materials
- [2] Covestro — Injection molding design guidance for thermoplastics
- [3] SABIC — LEXAN resin design and processing guidance
- [4] ISO — ISO 294-4 Plastics: determination of molding shrinkage
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.