
Coring out a locally thick plastic section can reduce unnecessary resin mass and lower the risk of sink marks, but it is not a universal lightweighting solution. The removed volume may have been contributing to stiffness, impact resistance, fastening support, heat management or dimensional stability. A cored design also changes flow length, packing, cooling, shrinkage, warpage, ejection and tool-steel requirements. The outcome depends on resin, fiber loading, geometry, processing, environment, production volume and customer specifications.
For overseas OEM, procurement, quality and engineering teams, treat coring as a controlled geometry change. Establish why the section is thick, define what function must remain, and ask each supplier to show how the proposed core affects the part, mold and evidence plan. A lower calculated mass or a smoother cosmetic surface is not production approval by itself.
Requirement: preserve the released load path, interfaces, appearance limits and applicable compliance requirements unless the responsible owner approves a change. Recommendation: use coring, gradual transitions and support features only after the supplier explains the expected effect on mass, stiffness, sink, voids, shrinkage, warpage, tooling and validation.
01
What does coring out a plastic part actually change?
Coring removes material from a bulky region, usually from the side opposite a visible or functional face, so the section becomes more nearly uniform. The aim is often to replace a thick mass with a shell, pocket, rib, gusset or other controlled load path. This can help reduce localized cooling and shrinkage differences that appear as sink marks or internal voids. Autodesk describes sink marks and voids as localized shrinkage problems at thick sections when the cavity is not sufficiently compensated during packing [1].
Coring is not the same as simply making every wall thinner. A local core can preserve a functional outer wall while removing nonessential volume, but the remaining walls and transitions still determine stiffness, impact response and dimensional behavior. A deep pocket can also create long flow paths, trapped air, difficult ejection, thin steel conditions or a new knit-line location. Ask the supplier to mark the proposed core, the intended load path, the draw direction, draft, radii, venting and ejection strategy on a controlled section view.
The requirement is the part function and acceptance method. The recommendation is the particular core shape, wall relationship or reinforcing feature. Keep those separate in the RFQ so a supplier does not present a preferred mold concept as though it were a customer requirement.
02
How should buyers balance weight, sink marks and structural performance?
A thick region may exist to carry bending, support a fastener, resist impact, locate a mating part, manage heat or prevent local deflection. Removing it can reduce weight but also reduce section modulus and stiffness. A rib or gusset may restore directional support, yet it adds a wall transition and can transfer sink or read-through to a show surface. Fiber-filled grades may raise stiffness in a flow direction while increasing orientation sensitivity and anisotropic shrinkage. None of these effects can be approved from a generic percentage rule.
Use the same baseline revision, resin direction, boundary conditions and mass measurement method when comparing a solid baseline with a cored alternative. The table below is a screening aid for procurement and design review, not a guarantee for a particular resin or geometry.
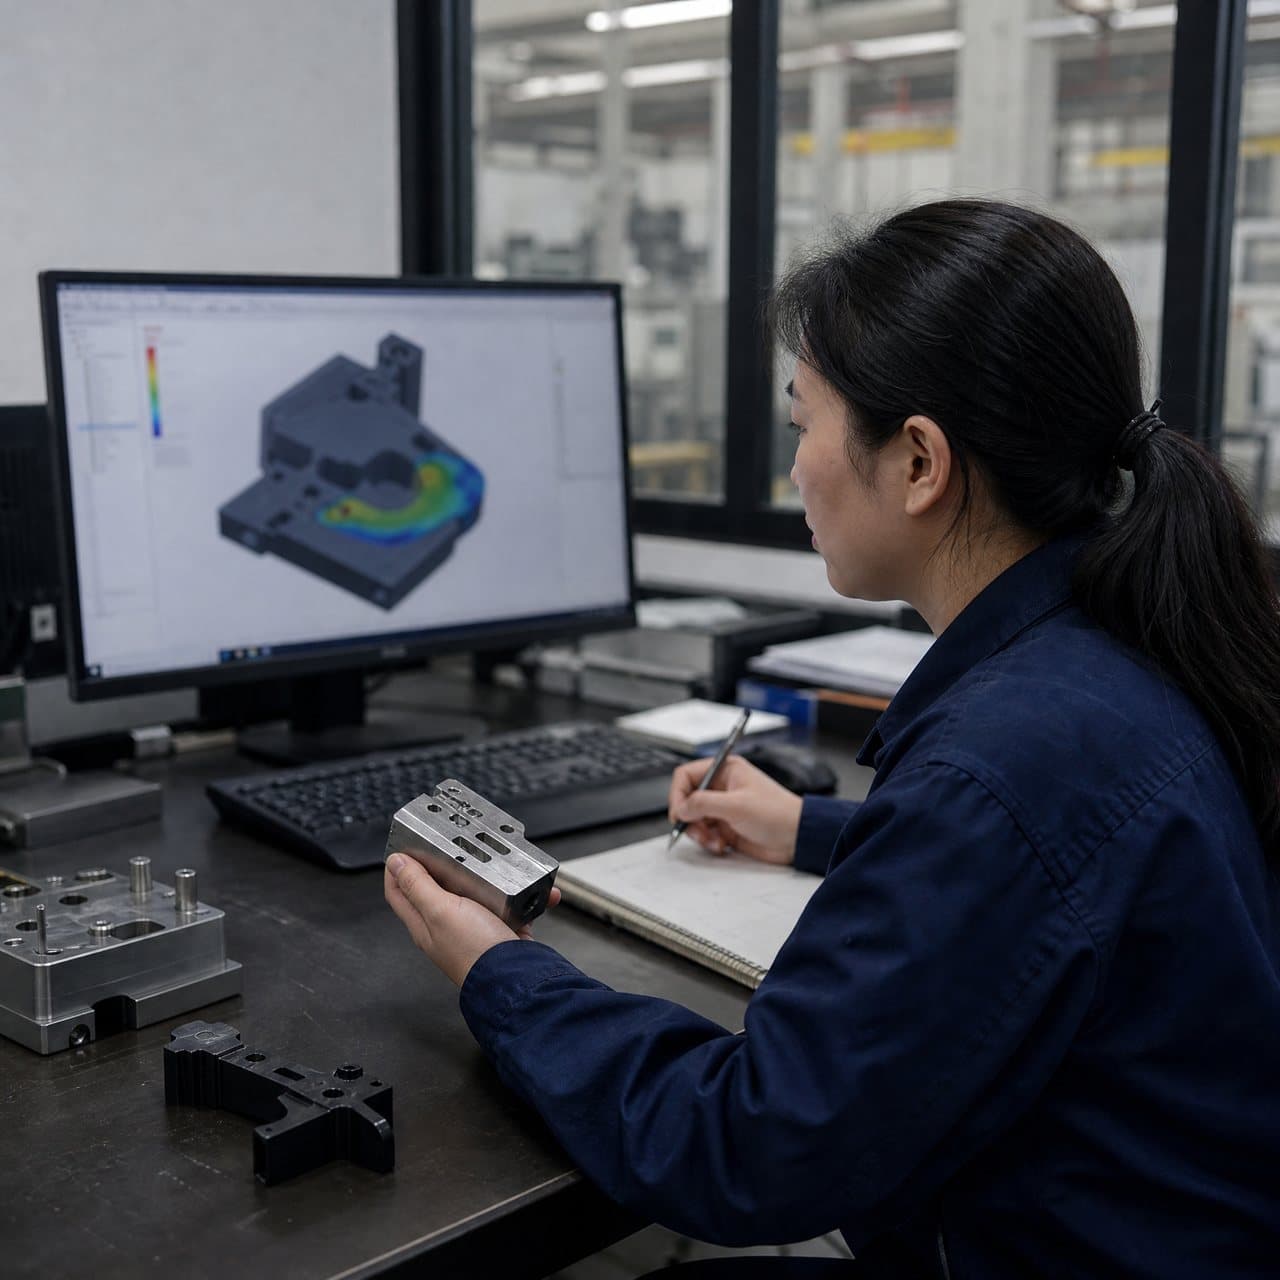
A supplier should distinguish analysis from physical evidence. A flow or structural simulation can expose likely risks, but its conclusions depend on the material data, mesh, gate, cooling, constraints and process assumptions. Require a part-specific trial and validation plan when the cored feature affects a critical interface, load case, appearance zone or regulated application.
| Decision area | Potential benefit of coring | Risk or trade-off to investigate | Evidence to request |
|---|---|---|---|
| Mass | May remove nonfunctional bulk and reduce molded volume. | Ribs, bosses, pads, runners, trim or a thicker perimeter can offset the modeled saving. | Before-and-after CAD mass plus actual molded mass, with resin grade, conditioning and measurement method stated. |
| Sink marks and voids | Can reduce thick-section shrinkage and improve wall uniformity. | A remaining thick boss, rib root, corner or isolated pocket can still sink or form a void. | Section map, sink-risk review, packing and cooling assumptions, and agreed visual or internal inspection method. |
| Stiffness and impact | Can retain an outer skin while placing support near the load path. | Reduced section or an abrupt core transition may lower deflection or impact margin and concentrate stress. | Defined load cases, fixtures, temperature, deflection or impact criteria, and part-level analysis or testing. |
| Shrinkage and warpage | More even sections may reduce differential cooling in some designs. | Flow direction, fiber orientation, uneven cooling and asymmetric walls can still distort the part. | Gate, vent and cooling concept; material assumptions; predicted deformation; measurement datums and method. |
| Tooling and production | A core may reduce steel volume or simplify a bulky cavity region before tool release. | Deep cores can need slides, lifters, inserts, extra draft, stronger steel, revised ejection or new inspection access. | Tool layout, pull direction, draft, ejection, steel conditions, tool-change scope, lead-time and cost exclusions. |
03
Which geometry and material inputs must be frozen before coring?
Freeze the functional baseline before requesting a weight target. The brief should identify the released part and drawing revision, nominal and permitted mass basis, load and impact cases, mounting or sealing interfaces, show surfaces, dimensional datums, temperature range, chemical or moisture exposure, expected volume and any customer-controlled material or compliance requirement. State whether the proposed core may change internal volume, thermal behavior, acoustic behavior or assembly clearance.
Name the exact resin grade direction rather than only a polymer family. Density is relevant to mass, but the grade also controls flow, stiffness, impact, creep, shrinkage, weld-line behavior, drying and environmental response. Fiber loading, recycled content, colorants and additives may change the result. Request the current technical data sheet, processing guidance, allowable substitutes, lot traceability route and any conditioning needed for comparison. Material data from a test specimen does not prove the cored molded part will perform in every direction or environment.
Ask the supplier to identify core depth, nominal remaining walls, transition radii, boss and rib relationships, draft, gate location, vents, cooling circuits and ejection points. Treat numerical wall or rib ratios as starting recommendations only; the acceptable geometry depends on resin, flow length, tool construction, surface requirements and process capability. Where a customer specification sets a dimension, appearance limit or performance threshold, that requirement governs over a generic design guide.
04
What supplier evidence should support a cored-part tool decision?
At the feasibility gate, require controlled before-and-after CAD, annotated sections, mass calculations, material assumptions, load-path explanation, DFM findings, proposed gate and cooling concept, draft and ejection review, and a risk register. The supplier should state whether the change needs new steel, a replaceable insert, a slide or lifter, a machine-capacity change, a new fixture or a revised inspection plan. Separate one-time engineering and tooling effects from recurring material, molding, scrap and quality costs.
Before tool steel release, engineering and quality should approve the part revision, resin route, critical interfaces, cosmetic zones, analysis assumptions, trial quantity, measurement methods and acceptance criteria. If simulation is supplied, request the exact material data source, gate and process assumptions, boundary conditions, result units and limitations. A simulation result is decision support, not proof of production capability.
At trial and production approval, obtain material identification and lot records, tool and cavity identification where relevant, actual mass, dimensional results, visual review, functional checks and any agreed sink, void, impact, stiffness or environmental testing. Record sample conditioning and process context. If a feature is hidden, agree how it will be inspected; a calibrated instrument or a supplier declaration does not by itself establish fitness for the customer’s application.
05
How can procurement set approval gates and prevent uncontrolled changes?
Use four practical gates. Gate 1 freezes the baseline, requirements, material direction and measurement condition. Gate 2 selects a coring concept after DFM, load-path and risk review. Gate 3 authorizes tool steel, inserts, material substitution or process changes only after commercial scope, timing and validation are accepted. Gate 4 releases production only after trial evidence meets the approved criteria or documented deviations are dispositioned by the named authority.
Normalize quotations before comparing them. Ask every supplier to state part revision, resin and color, cavity count, runner arrangement, mass basis, tool modifications, machine assumptions, secondary operations, inspection scope, expected volume, validation deliverables and exclusions. A lower price or mass can reflect a different material, omitted steel work, a narrower quality plan or a different interpretation of the part boundary.
Put change control in the purchase specification or quality agreement where the feature matters. Define triggers such as a core dimension, rib or boss change, resin or filler change, gate or cooling change, tool relocation, process-window change or alternate supplier. Reopen the engineering review when a change could affect stiffness, impact, sink, voids, shrinkage, warpage, fit, appearance, compliance or customer approval.
Practical takeaway
Before you move
to the next review.
- Freeze the baseline part revision, mass measurement condition, load path, interfaces, appearance zones, resin direction, environment and customer approval authority before proposing a core.
- Request a marked-up before-and-after section showing core depth, remaining walls, radii, ribs, bosses, draft, vents, gates, cooling and ejection assumptions.
- Compare mass, stiffness, impact, sink, voids, shrinkage, warpage, tooling, inspection and commercial scope at the same resin, revision and boundary conditions.
- Require supplier evidence at feasibility, tool-release, trial and production gates, including material identity, assumptions, actual mass, dimensions, function and open-risk disposition.
- Add change-notice triggers for core geometry, material or filler, gate, cooling, tool steel, process window, cavity, supplier and inspection changes that could affect approval.
FAQ
Common questions
Does coring out a plastic part always reduce sink marks?
No. Coring can reduce a localized thick section and therefore may reduce sink or void risk, but the remaining boss, rib root, corner, core transition, packing condition and cooling balance may still create defects. The result depends on resin, geometry, gate and process. Require a part-specific DFM or process review and agreed molded-part evidence.
Can coring make an injection-molded part weaker?
It can. The removed material may have contributed to bending stiffness, impact resistance, fastening support or dimensional stability. A rib or gusset may restore support in one direction but introduce stress concentration or orientation effects. Define the actual load, environment and acceptance criteria, then verify the cored geometry through appropriate analysis or testing.
Is a cored design always cheaper or faster to mold?
No. A cored section may reduce resin volume, but it can require slides, lifters, inserts, additional draft, different cooling, more inspection or a longer development plan. Material cost, cycle time, tooling cost and yield depend on the resin, geometry, machine, tool architecture, volume and process window. Compare normalized supplier quotations rather than assuming a benefit.
What should an OEM approve before a supplier cores an existing mold?
Approve the controlled CAD and drawing change, load-path rationale, exact material route, mass basis, sink and void risk review, tooling and ejection concept, commercial and timing impact, validation plan, inspection method and change authority. Do not authorize steel modification from a visual concept or an unsupported percentage weight-saving claim.
References
Source material
- [1] Autodesk Moldflow, “Troubleshooting sink marks and voids.”
- [2] Protolabs, “Injection Molding Guide: Process, Design Tips, & Materials.”
- [3] Covestro, “Part and Mold Design: Thermoplastics.”
- [4] ISO, “ISO 20457:2026 Plastics moulded parts — Tolerances and acceptance conditions.”
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.