
A lighter injection-molded part is not automatically a better part. Removing mass can reduce energy absorption, local stiffness, section support and tolerance to notches or weld lines, even when a resin data sheet shows acceptable impact strength. For overseas OEM, procurement, quality, engineering and product teams, the useful decision is to define the drop event and functional boundary first, then compare resin, geometry, tooling and validation options against the same evidence plan.
The outcome depends on the exact resin grade, filler or fiber loading, color and conditioning; wall and rib geometry; gate and flow direction; molding process; service temperature and environment; production volume; tool state; and customer specifications. This guide focuses on impact-strength trade-offs and drop-test planning. It does not replace the product owner’s design authority, applicable standards or application-specific qualification.
Requirement: preserve the released product function and acceptance criteria unless their owner approves a change. Recommendation: ask suppliers to quantify the mass change and explain how impact, stiffness, shrinkage, warpage, tooling and validation will be rechecked on representative molded parts.
01
1. Define the drop event before removing material
A drop test is only meaningful when the product team defines what is being dropped, from where, onto what surface and in what condition. Record the assembled configuration, mass, center of gravity where relevant, orientation, drop height or velocity, target temperature, humidity or conditioning, payload or battery state, packaging state, number and sequence of drops, and the post-test inspection window. State whether the requirement is no fracture, retained function, no leakage, no loss of sealing, controlled cosmetic damage, or a more specific result. A housing dropped empty onto a laboratory steel plate is not the same event as a loaded product falling during service or shipment.
Separate requirements from recommendations. The buyer or product owner must own the functional failure definition, customer specification, target markets and approval authority. The molder can recommend a resin, rib layout, corner radius, gate position, process window or trial sequence, but those recommendations should remain conditional until the product boundary and test method are accepted. If the customer specifies a test standard, use that standard and its required configuration; do not silently substitute a convenient internal test.
ASTM D5276 describes free-fall testing of loaded containers, so it may be relevant to packaging or shipping-unit questions, but it is not a universal product drop-test method. For an individual molded component, define a product-specific fixture, impact surface and failure assessment with the customer or engineering owner. The test method, specimen condition and pass/fail rule should be frozen before comparing supplier claims.
02
2. Understand how lightweighting changes impact and stiffness
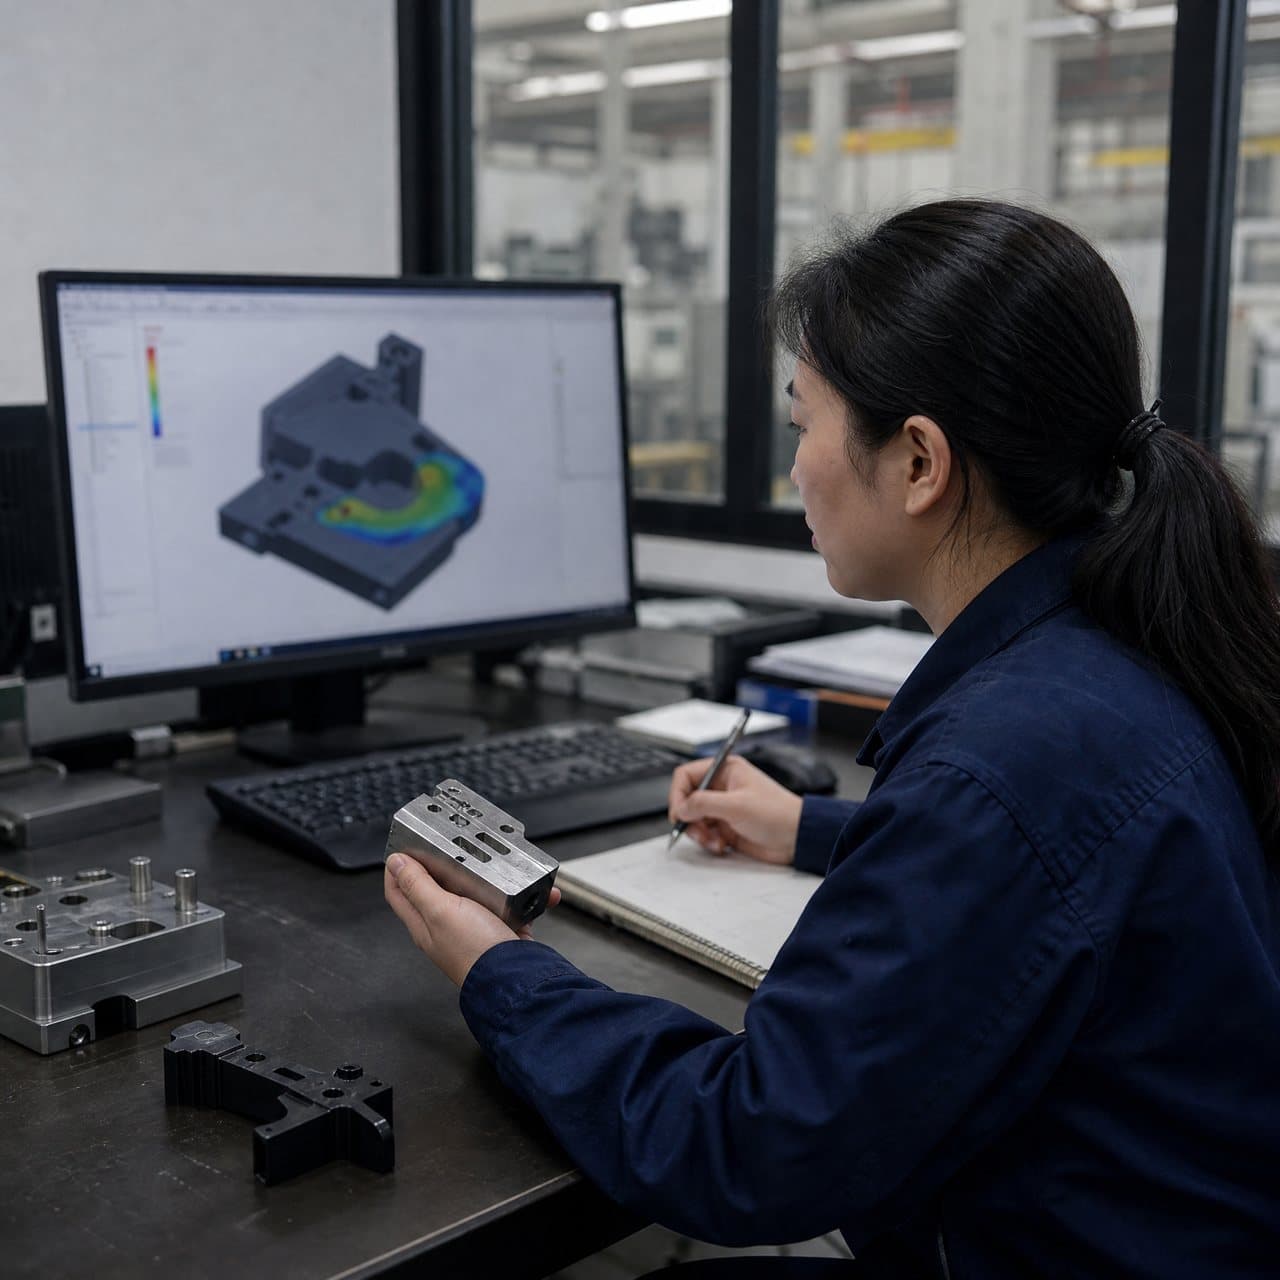
Impact performance is a system response, not a single resin number. A thinner wall may lower mass and bending stiffness, increase local deflection, and move stress into corners, bosses, snaps or fasteners. Removing a rib can change the load path. A sharp transition, weld line, gate vestige, knit line or molded-in stress can become a crack initiator. A part that survives one orientation may fail in another because impact energy reaches a different feature.
Reinforcement can improve stiffness in a selected direction, but fiber or mineral loading can also increase anisotropy, alter surface appearance, change flow and shrinkage, and make weld-line or transverse impact behavior different from the data-sheet specimen. Impact-modified grades can be useful candidates, but the actual result still depends on wall thickness, temperature, moisture, color package, processing history and geometry. Do not rank materials by density, nominal Izod value or tensile strength alone.
Use a baseline comparison. Measure the current part mass under a stated condition, document the existing failure mode, and compare the proposed design at the same load case and test boundary. A lower mass is a design result, not evidence of success. Engineering analysis can screen concepts, but it should identify assumptions and be followed by representative molded-part testing where impact is a release criterion.
| Lightweighting lever | Potential impact or dimensional effect | Evidence to request before approval |
|---|---|---|
| Reduce nominal wall | Lower mass and local stiffness; higher deflection, fill sensitivity or crack risk may occur. | Before/after section map, flow and cooling review, stiffness result, molded-part drop evidence and dimensional review. |
| Replace solid mass with ribs or coring | Can preserve a load path, but rib roots, corners, sink, weld lines and stress concentration need review. | Marked CAD sections, rib direction and radii, tool concept, failure-mode analysis and first-off inspection. |
| Change to an impact-modified or reinforced grade | May change impact, stiffness, flow, shrinkage, warpage, surface and tool wear behavior. | Exact grade and color, conditioning data, processing guidance, material traceability and application-relevant tests. |
| Remove or consolidate features | May change attachment, assembly, sealing, protection or the way impact energy is transferred. | Interface and assembly review, customer disposition, drop sequence, functional test and revised inspection plan. |
03
3. Select material evidence that relates to the finished part
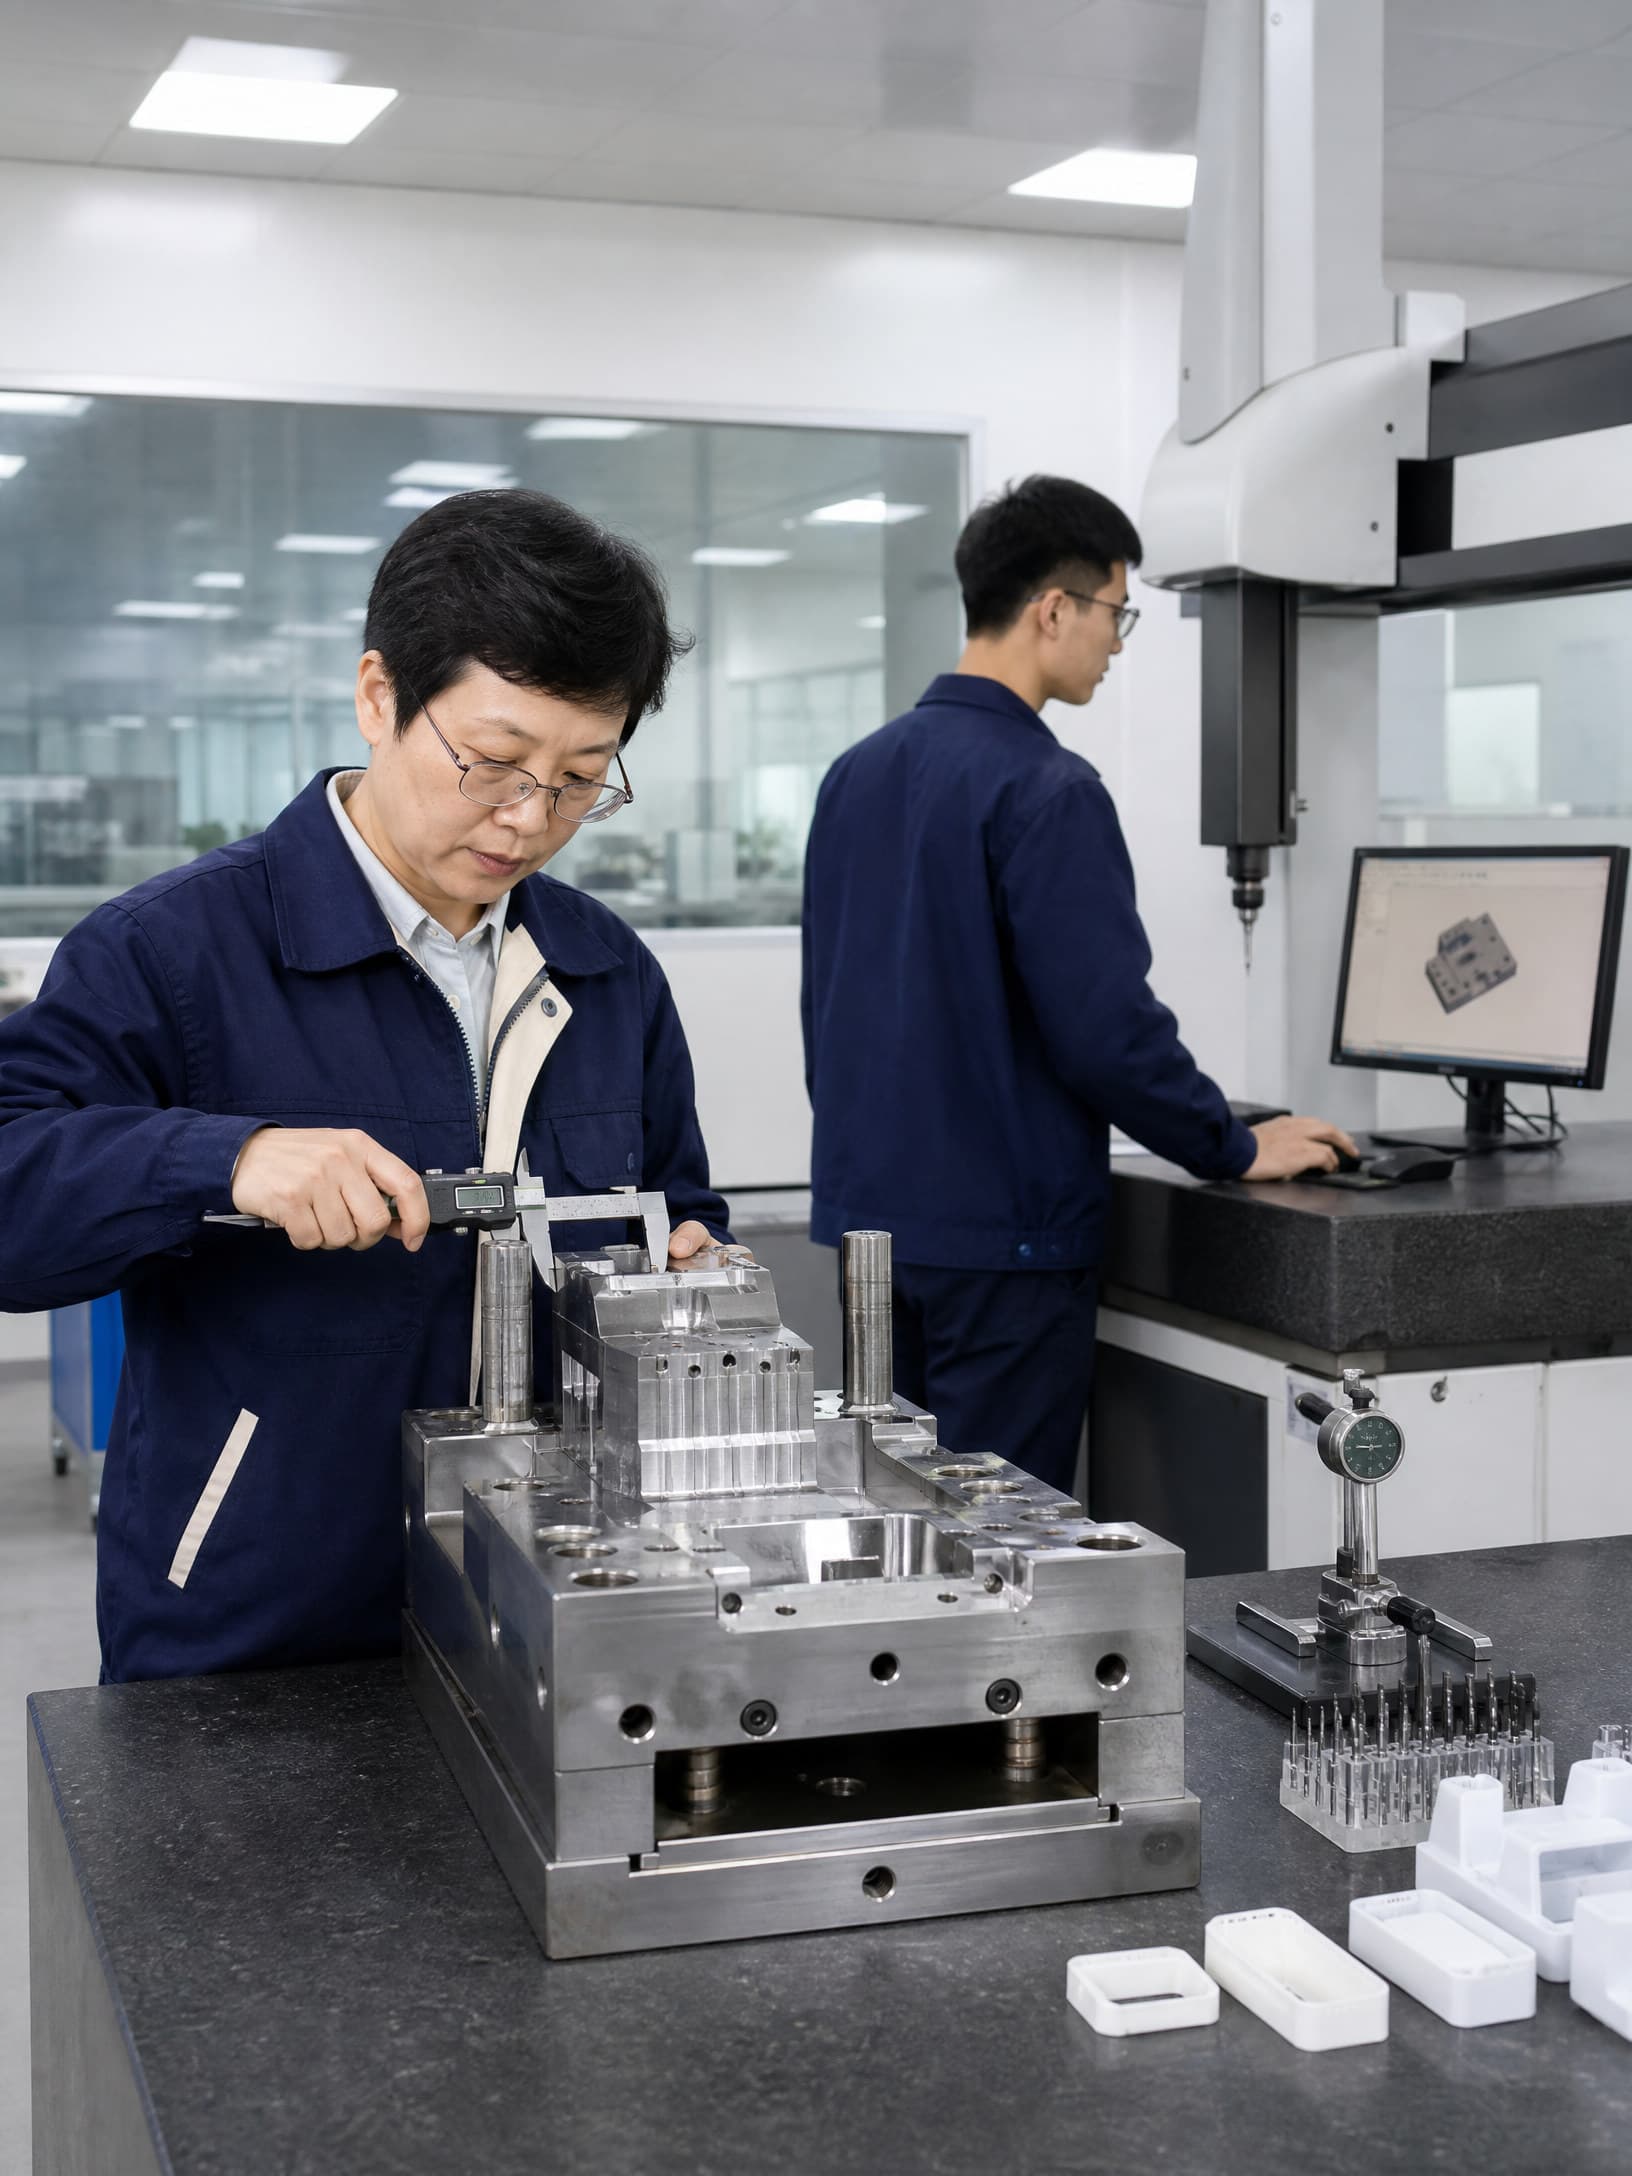
ASTM D256 measures Izod pendulum impact resistance of standardized, notched specimens under specified conditions. ASTM notes that processing, mold design, specimen thickness, notch quality and environmental conditioning can affect results, and that rankings may change under different conditions. Treat a data-sheet value as a screening input, not a direct prediction of a molded housing, bracket or cover. ISO 6603-2 likewise states that puncture-impact results are comparable only when specimen preparation, dimensions, surfaces and test conditions are the same, and that finished-product impact behavior cannot be predicted directly from the test.
Ask the supplier and resin producer for the exact commercial grade, reinforcement or filler level, color, lot identification method, current technical data, conditioning instructions and the limits of the reported test. Request data at relevant temperatures and moisture states where the application warrants it. If a weld line, gate region, molded insert or thin section is a known risk, test a representative feature or part rather than relying only on a plaque or bar.
Material approval should also cover manufacturing consequences. Confirm drying or conditioning controls where applicable, melt and mold-temperature direction, flow length, gate and vent concept, expected fiber orientation, shrinkage direction, cooling balance, ejection risk and permitted substitutions. A material change can affect tool steel, wear, cavity fill, warpage, inspection and customer qualification. No universal strength, weight saving, cost or cycle-time result should be promised without the defined grade, geometry, process, environment, volume and specification.
04
4. Build a drop-test plan that separates screening from release
Use a staged test plan. Early screening can compare design concepts with a small, controlled sample set, but it should not be presented as production qualification. The screening report should identify the part revision, material and lot, molding conditions if known, conditioning, sample count, drop orientations, height, impact surface, payload and observed failure mode. Photograph or otherwise document cracks, whitening, permanent deformation, separation, loose inserts, loss of fit and functional changes.
For a release test, define sample selection and traceability. Decide whether samples represent one or more cavities, the production-intent tool, the approved resin and color, the intended process window, assembled mating parts and the expected service condition. Include dimensional checks before and after testing, functional or sealing checks, and a rule for retest or failure disposition. If the product is safety-relevant, regulated or customer-controlled, the customer’s validation procedure takes precedence over this guide.
Use analysis and supplier trials to focus the test, not to avoid it. A drop simulation may help identify high-strain zones or compare orientations, but its material model, contact assumptions, fixtures, mesh, temperature and failure criterion must be visible. Require the supplier to distinguish predicted behavior from measured behavior. The approval record should state what the evidence proves, what it does not prove, and which open risk remains with the product owner.
05
5. Control tooling, sourcing and approval gates
Lightweighting can require more than a CAD edit. A revised wall or rib may change gate location, venting, cooling, ejection, insert support, parting line, mold steel, cavity balance or inspection fixtures. A new resin or fiber loading may increase wear or alter shrinkage and warpage. Ask each bidder to separate one-time engineering and tooling effects from recurring material, molding, scrap, inspection, packaging and logistics effects. Compare the same scope, volume assumptions and evidence obligations before using price or quoted mass as a selection criterion.
Request supplier evidence in gates. Gate 1 should confirm the baseline revision, requirements, test boundary, material direction and mass measurement method. Gate 2 should approve the preferred concept, DFM response, risk register, material evidence and tooling impact. Gate 3 should authorize steel changes, new inserts or material substitution only after the cost, timing and validation plan are accepted. Gate 4 should release production only after traceable first-off or qualification results, actual mass, dimensions, functional checks, drop-test findings and deviations are reviewed by named owners.
Put change control into the purchase and quality documents. Define notification triggers for resin grade, filler or color, supplier, tool, cavity, gate, process window, machine, geometry, assembly method and test method. Ask for material certificates or lot records where required, cavity identification when relevant, inspection reports tied to the drawing revision, and a reaction plan for failed drops. The supplier can provide evidence and recommendations; the product owner retains responsibility for final application approval.
Practical takeaway
Before you move
to the next review.
- Freeze the baseline part revision, mass measurement condition, resin grade, assembly state, service environment and functional failure definition before lightweighting begins.
- Define drop height or velocity, orientation, impact surface, payload, conditioning, sequence, sample traceability, inspection window and pass/fail criteria with the customer or product owner.
- Ask suppliers for before-and-after sections, load-path rationale, material grade and conditioning evidence, DFM and tooling impact, assumptions, risks and a representative molded-part validation plan.
- Compare candidates using the same geometry boundary, material evidence, test conditions, volume, tool state, commercial scope and approval obligations; do not rank by density or a single impact value.
- Set gates for concept approval, tool or material change, production-intent samples and final release, with documented deviation, retest and change-notification rules.
FAQ
Common questions
Can a thinner injection-molded wall pass the same drop test as the original part?
It may, but thickness alone does not determine the outcome. The revised wall changes stiffness, deflection, flow, cooling, stress concentration, weld-line behavior and possibly the load path. Compare the specific grade, geometry, orientation, temperature, payload and impact surface, then verify representative molded parts against the approved acceptance criteria.
Is a high Izod impact value proof that a lightweight part will survive a drop?
No. Izod is a standardized notched-specimen test under defined conditions. Specimen thickness, notch, processing, conditioning and test method affect the result, and the value does not directly predict a finished product with ribs, corners, weld lines, fasteners or a different impact direction. Use it for material screening and add part-level evidence.
Should glass fiber be added to make a lightweight injection-molded part stronger?
Not automatically. Fiber can increase stiffness in a preferred direction, but it can also change anisotropy, shrinkage, warpage, surface appearance, weld-line response, tool wear and impact behavior across directions. Approve a named grade and loading only after reviewing the service loads, flow orientation, appearance, environment and representative-part tests.
What should an OEM request from a supplier before approving a drop-test plan?
Request the controlled part and material revisions, test configuration, conditioning, drop orientations and sequence, impact surface, payload, sample and cavity traceability, inspection method, pass/fail criteria, failure documentation, retest rule, tooling or process assumptions and the distinction between screening and release evidence. Confirm who owns final approval and how changes trigger revalidation.
References
Source material
- [1] ASTM International, ASTM D256-26 — Standard Test Methods for Determining the Izod Pendulum Impact Resistance of Plastics
- [2] ISO, ISO 6603-2:2023 — Plastics: Determination of puncture impact behaviour of rigid plastics, Part 2
- [3] ASTM International, ASTM D5276-19 — Standard Test Method for Drop Test of Loaded Containers by Free Fall
- [4] ASTM International, ASTM D955 — Standard Test Methods for Measuring Shrinkage from Molding Compounds
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.