
Lightweighting an automotive component is not simply a matter of reducing wall thickness or replacing metal with plastic. The buyer must preserve the required load path, impact behaviour, interfaces, appearance and service life while selecting a resin and molding process that can be controlled at the planned volume. Resin family, fiber loading, geometry, processing window, temperature, moisture, chemical exposure, forecast and customer specifications all influence the answer. This guide gives OEM, procurement, quality, engineering and product teams a practical way to compare concepts, request supplier evidence and move from design intent to an approved molded part.
Treat weight reduction as a controlled engineering change: define the mass target and functional limits first, then approve resin, geometry, tooling and validation evidence at explicit gates. No material or design route guarantees universal weight, strength, cost or cycle-time savings.
01
What makes an injection molded automotive component a credible lightweighting candidate?
The strongest candidates usually have a clear function that can be delivered through molded geometry: a bracket, cover, duct, carrier, housing or trim-support component with defined interfaces. A part may be suitable when its loads, temperatures, chemicals, vibration and impact events are understood and when the proposed resin can meet them with an appropriate safety margin. It is not enough that the plastic version has a lower nominal density. The comparison should include the complete part and assembly, including inserts, fasteners, shielding, coatings, clips and any secondary operations.
Begin with a controlled baseline. Record the current part mass, envelope, attachment points, critical dimensions, stiffness or deflection limits, impact or abuse cases, temperature range, fluid exposure, noise or vibration requirements and expected service life. State which requirements are mandatory and which are recommendations. A concept should not pass to detailed tooling because it is lighter in CAD alone; it should pass because the proposed material-geometry combination has a credible path to satisfy the approved requirements.
Ask the supplier for a concept comparison that identifies assumptions rather than presenting a single promised result. Useful evidence includes mass by component, section views showing the load path, resin grade and reinforcement content, preliminary fill and cooling analysis, likely gate locations, identified risks and the tests proposed to close them. The customer specification and drawing remain the approval authority when they differ from a general design rule.
02
Balance stiffness, impact and environment before selecting the resin
Lower density can support mass reduction, but automotive performance depends on more than density. Stiffness is affected by resin modulus, temperature, moisture, fiber orientation, section geometry and support conditions. A reinforced grade may increase stiffness in the fiber direction while creating directional behaviour that must be considered in the load path. Impact performance can also vary with temperature, notch shape, weld lines, molding history and aging. These are reasons to specify the exact commercial grade and reinforcement level rather than asking for a generic nylon, polypropylene or polycarbonate.
The service environment should be translated into testable requirements. Identify hot and cold exposure, humidity, water or glycol, oils, cleaners, salts, UV, vibration and sustained loads as applicable. For semi-crystalline resins, cooling and crystallization influence dimensions and performance; for moisture-sensitive resins, drying and material handling can affect molding and properties. Supplier recommendations can inform the shortlist, but the final material choice should be supported by grade data, representative molded specimens and the customer’s application tests.
The table below is a screening aid, not a material ranking. It shows what a buyer should compare and what evidence should be requested before treating a lightweight concept as viable.
Material and concept comparison
| Decision area | What to compare | Evidence to request | Approval caution |
|---|---|---|---|
| Mass and stiffness | Part mass, section modulus, deflection under the specified load and temperature | Material grade data, sectioned CAD, simulation assumptions and measured deflection plan | A lower mass target does not prove equivalent stiffness; validate the actual geometry and supports. |
| Impact and durability | Impact locations, notch sensitivity, fatigue or vibration duty and temperature range | Test method, conditioned specimens, failure criteria and representative molded samples | Room-temperature coupon results may not represent a finished part across the service envelope. |
| Fiber or mineral loading | Reinforcement percentage, orientation, anisotropy, surface appearance and abrasion risk | Exact grade datasheet, flow-direction assumptions, gate proposal and tool-steel recommendation | Reinforcement can change shrinkage and warpage behaviour and may increase tool wear. |
| Chemical and environmental fit | Fluids, humidity, UV, heat aging and sustained load exposure | Compatibility data, conditioning plan and post-exposure dimensional or functional results | Generic chemical-resistance statements are not approval evidence for a customer-specific fluid mix. |
03
Use geometry and process together to protect the weight target
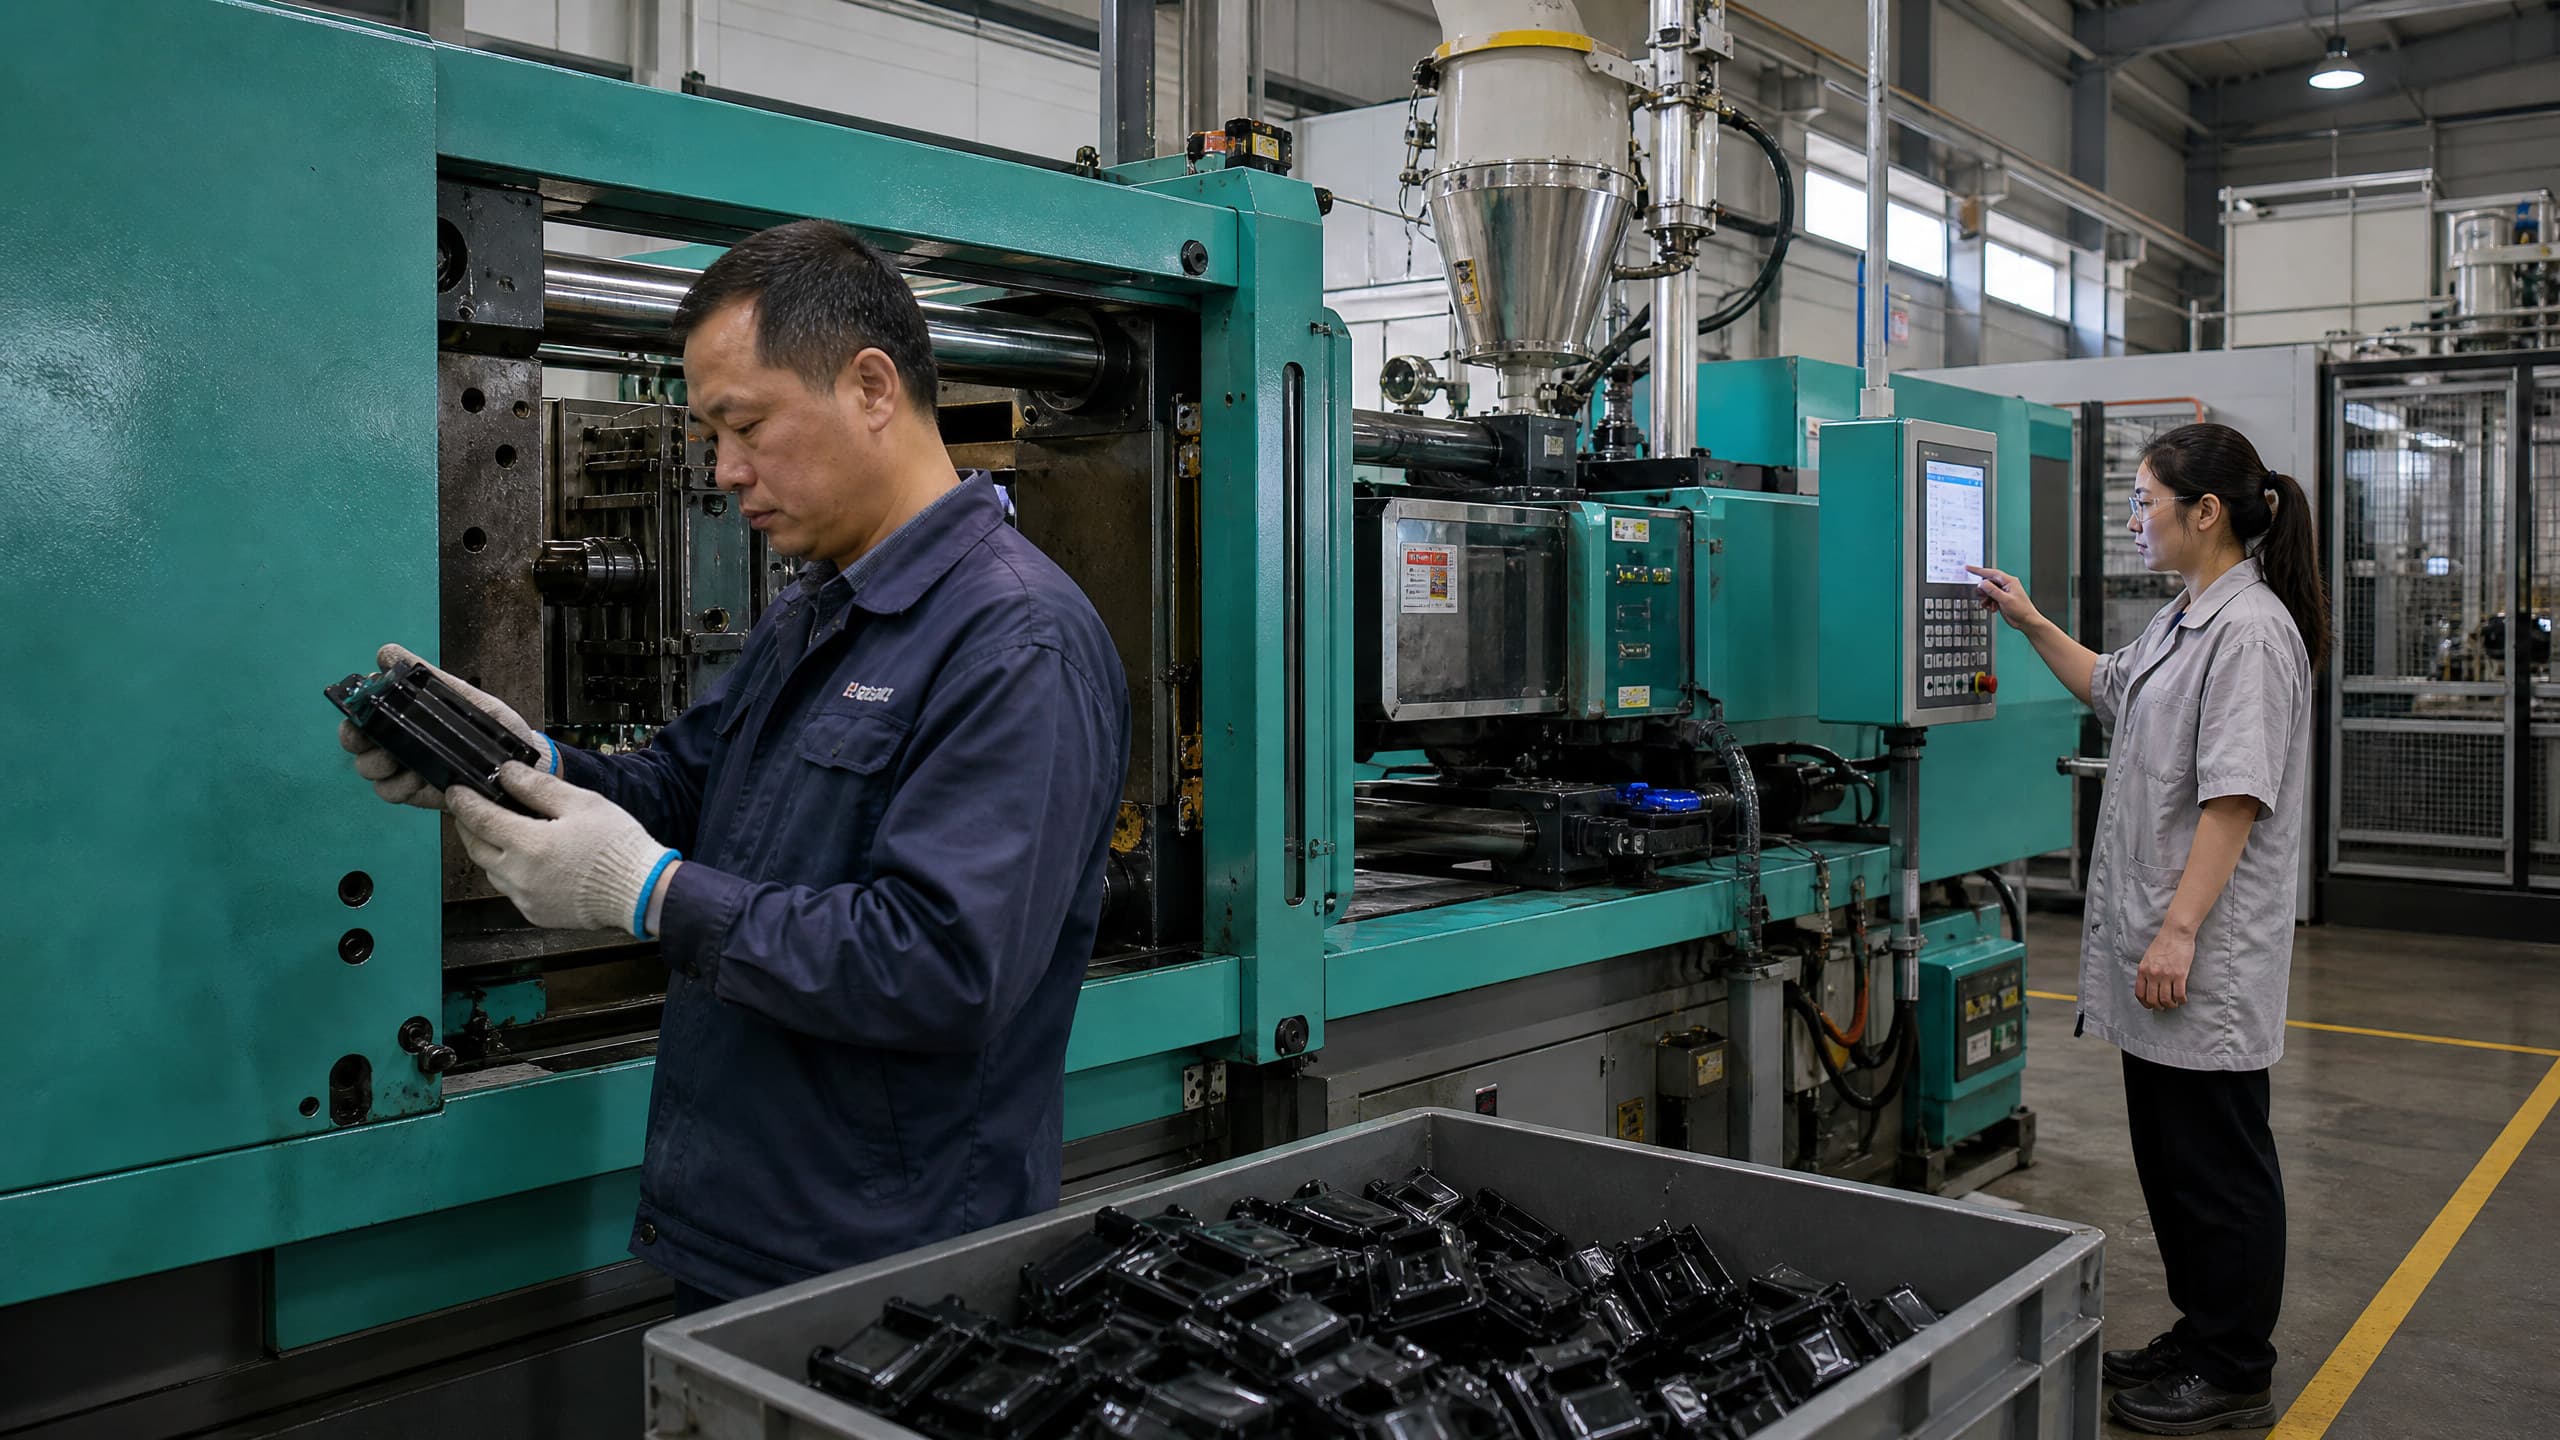
Weight reduction normally moves material into places where it contributes more effectively to stiffness, such as ribs, beads, flanges or closed sections. Those features still need draft, radius, ejection access, suitable wall transitions and a flow path that the mold can fill. Thin sections may reduce mass but can narrow the process window, increase pressure demand or make weld lines and short shots more sensitive. Thick junctions can preserve a load path while increasing sink, void or local cooling risk. The correct geometry is therefore a compromise between structural function and moldability, not a universal wall-thickness number.
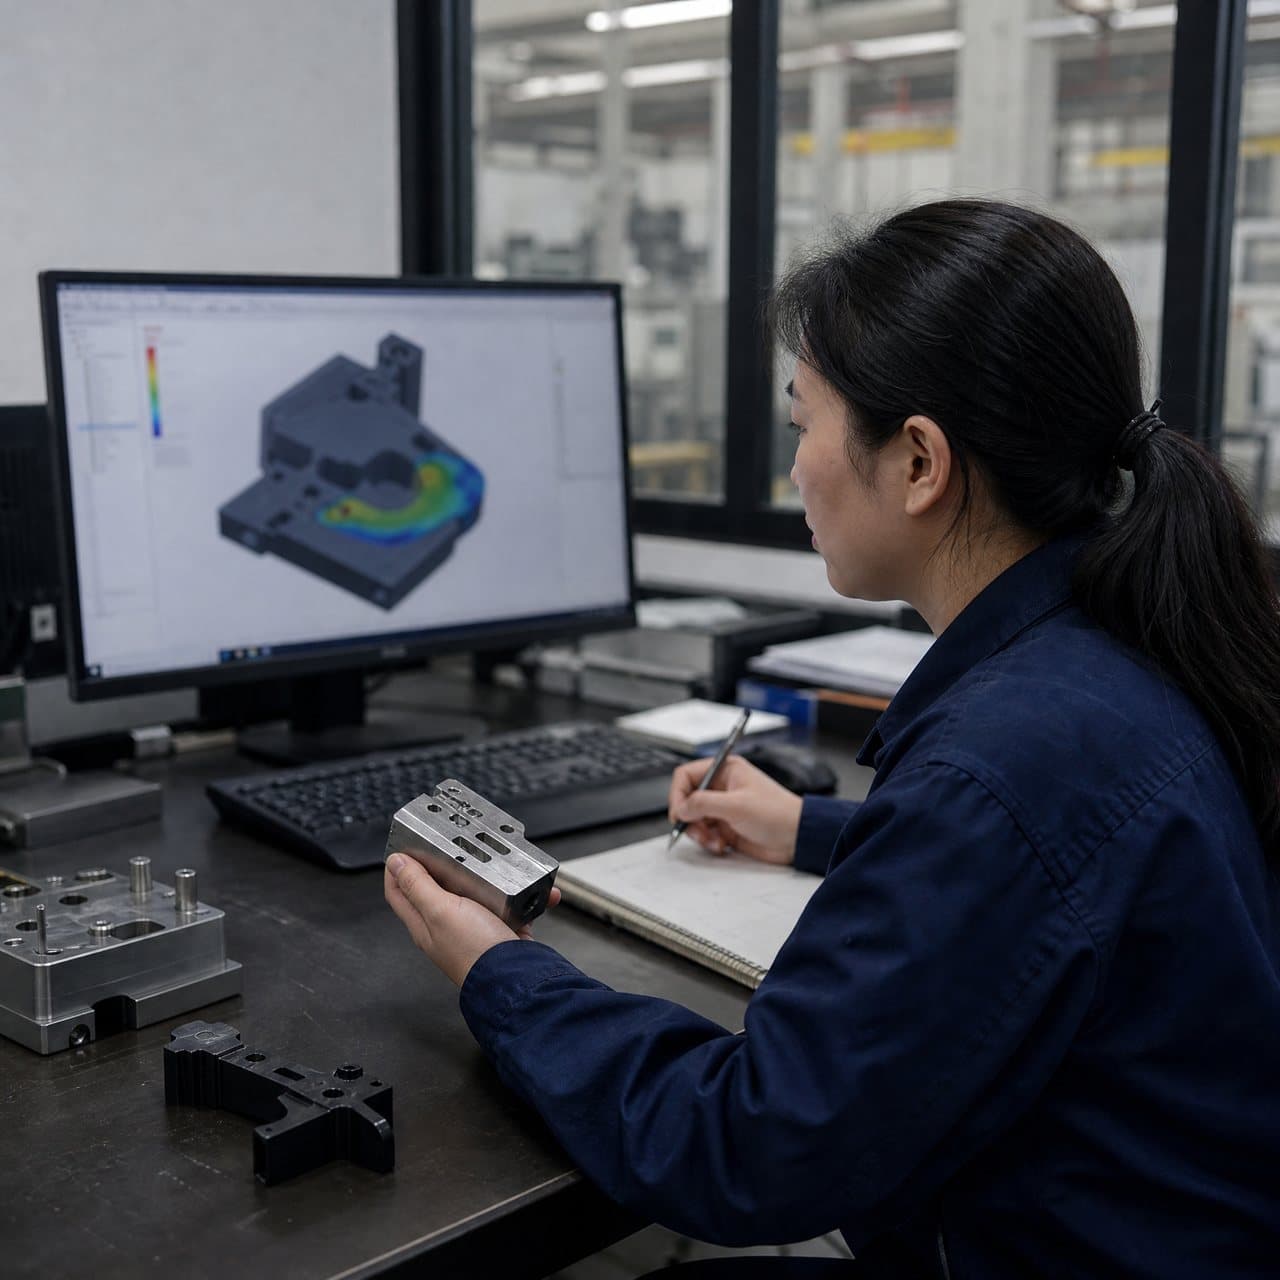
Gate position, runner balance, venting and cooling affect fiber orientation, weld lines, shrinkage and warpage. Directional shrinkage can move a mounting hole or change a mating face even when the nominal CAD mass is correct. For a reinforced or semi-crystalline resin, request a documented flow-analysis review that connects predicted orientation and cooling behaviour to the critical-to-quality features. Simulation is a risk-reduction tool; it does not replace parts molded in the production-intent tool.
Tooling decisions should follow the approved part and volume scenario. A lightweight component may require slides, lifters, conformal or carefully positioned cooling, hardened areas for abrasive grades, controlled ejection or a different cavity strategy. Ask the toolmaker to separate requirements from recommendations and to identify what changes if the resin grade, fiber content, cavity count, annual volume or cosmetic zones change. The quotation should show one-time tool work, trial corrections and maintenance assumptions separately from recurring part price.
04
Validate the molded component through staged evidence and approval gates
Validation should start before tool release with a risk review that links each requirement to a proposed analysis, inspection or test. The gate sequence may include design and material freeze, DFM and mold-flow review, tool-design approval, first tool trial, dimensional and appearance review, functional testing, capability or repeatability evidence, and production-part approval. The exact documents depend on the OEM or customer process, but the decision logic should be written into the project specification rather than inferred from a supplier’s standard package.
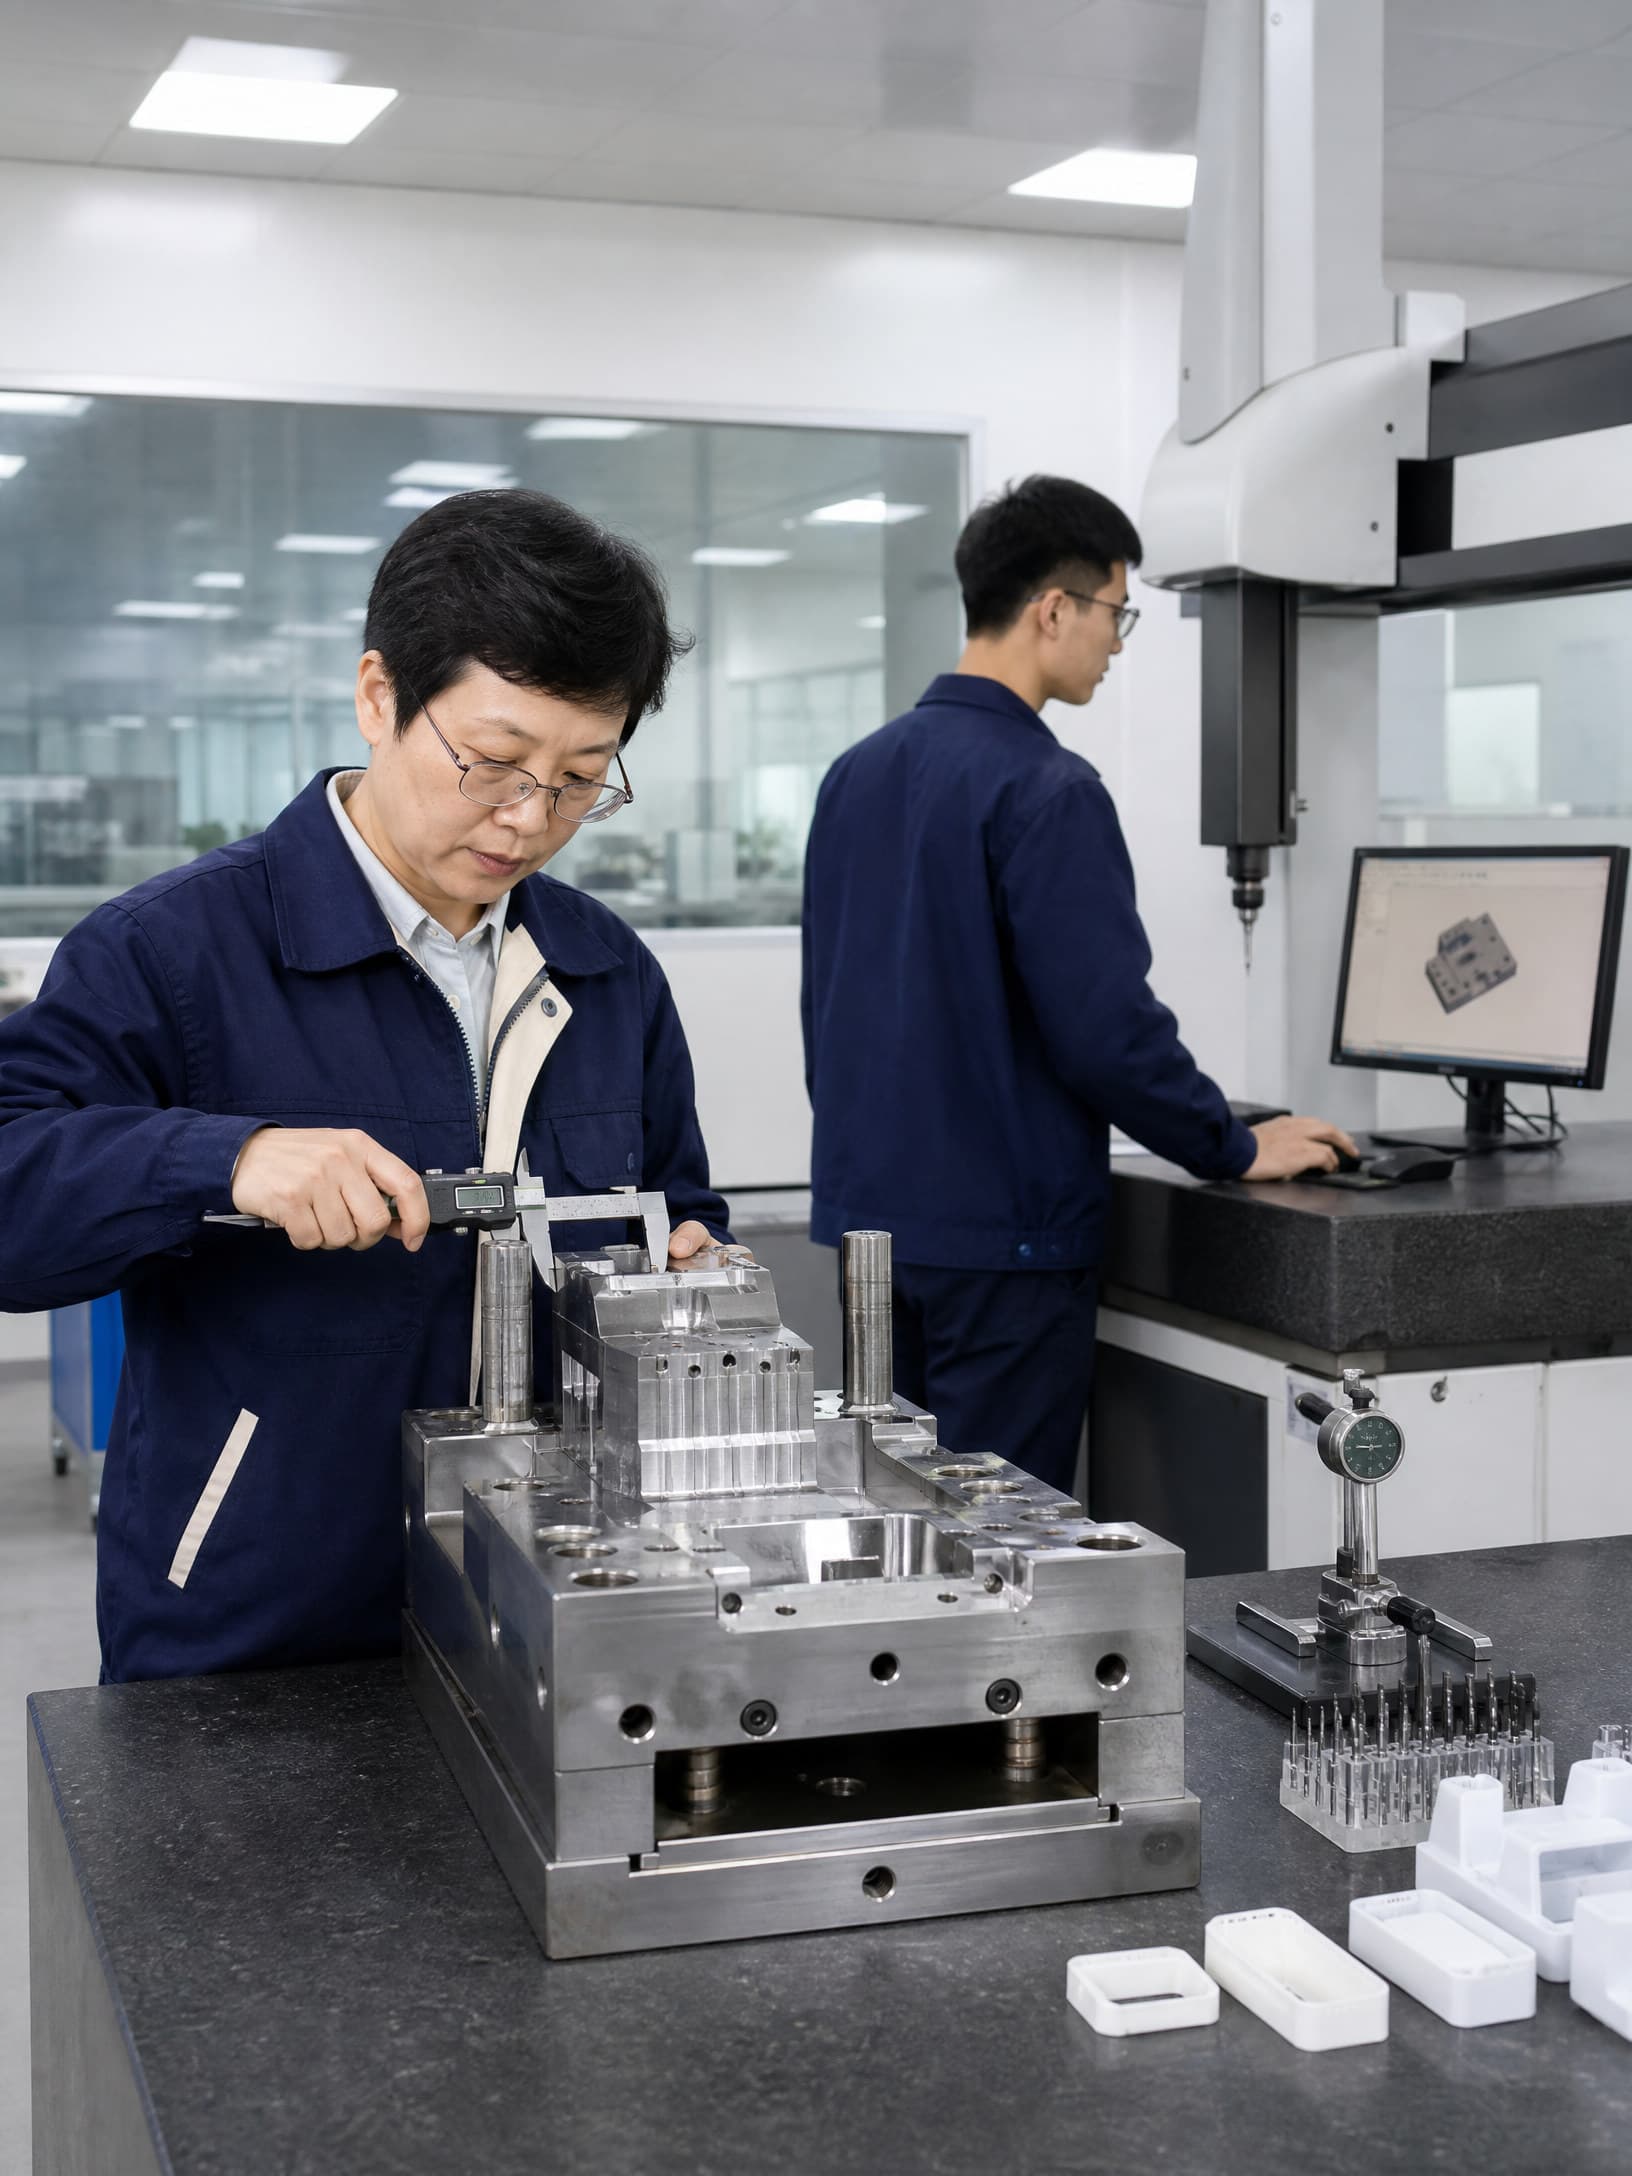
For the first production-intent parts, verify mass, critical dimensions, datums, mounting interfaces, stiffness or deflection, impact or abuse performance, environmental conditioning and any sealing, acoustic or assembly function that matters to the application. Record resin manufacturer and grade, lot traceability, drying or conditioning where relevant, process window, mold revision, cavity identity and inspection method. If a test uses coupons instead of the finished component, state the limitation and define the part-level evidence still required.
Quality teams should require a controlled nonconformance and change process. A substitution of resin, additive, colorant, fiber content, mold steel, gate, cooling circuit, machine or process window can change mass, shrinkage, orientation or performance. The supplier should notify the customer, assess the change against affected requirements and obtain the agreed re-approval before production release. A signed sample or a simulation report alone is not a blanket waiver of future production controls.
05
Make the sourcing decision on evidence, risk and total program fit
Procurement should compare suppliers against the same controlled CAD revision, annual demand, release pattern, resin grade, cavity concept, inspection scope, packaging and delivery basis. Request a mass range rather than an unsupported single value, and ask how part mass is measured, how runner or insert mass is treated and what tolerance applies. Compare tool investment, expected maintenance, trial plan, material availability, approved alternates and the commercial effect of a design or grade change. A lower quote may reflect a different tool life, inspection scope or material assumption rather than a better technical solution.
Supplier evidence should be specific enough for an approval decision: resin datasheet and certificate of analysis or conformity as agreed, material traceability plan, DFM and mold-flow findings, tool concept, control plan, measurement-system approach, first-article or dimensional report, test reports, capability evidence where required, and a documented deviation list. Ask the supplier to identify what is measured on every lot, what is sampled, which characteristics are cavity-specific and how records are retained. Do not request certifications or customer claims that have not been defined or verified for the actual site and program.
A practical award sequence is to approve the requirement set first, then the material and concept, then the tool design, then production-intent samples, and finally the controlled production process. Keep the lightweighting target visible at each gate alongside stiffness, impact, dimensional stability, appearance, cost and supply risk. The final decision should be based on demonstrated application fit and agreed acceptance criteria, not on a generic promise that injection molding will always be lighter, cheaper or faster than the incumbent route.
Practical takeaway
Before you move
to the next review.
- Document the baseline mass, complete assembly scope, load cases, interfaces, environment, service life and customer-specific acceptance criteria.
- Approve the exact resin grade, reinforcement level, color or additive package and any permitted alternates before tool design is released.
- Request supplier evidence linking geometry, flow, fiber orientation, cooling, shrinkage and warpage risks to critical-to-quality features.
- Define staged gates for DFM, tool design, first trial, dimensional and functional validation, production approval and controlled change management.
- Compare quotations on identical technical and commercial assumptions, including tooling, inspection, traceability, maintenance, volume and delivery basis.
FAQ
Common questions
Can injection molding always reduce the weight of an automotive component?
No. A molded polymer part may have lower density than a metal design, but the finished mass depends on required stiffness, impact performance, geometry, inserts, reinforcement, wall sections and service environment. A credible weight reduction must be demonstrated against the complete assembly and the approved functional requirements.
Does adding glass fiber automatically make a lightweight molded part stronger?
Not automatically. Glass fiber can increase stiffness or strength in relevant directions, but orientation, loading, weld lines, moisture, temperature, geometry and processing affect the finished component. It can also introduce directional shrinkage, warpage, surface effects and additional tool wear. Validate the exact grade and part.
What validation evidence should an OEM request for a lightweight injection molded part?
Request evidence mapped to the approved requirements: material and lot traceability, DFM and flow review, dimensional results, mass, functional or stiffness tests, impact or environmental testing where applicable, process controls, capability or repeatability evidence and the agreed production-part approval package. The exact tests and acceptance limits should come from the customer specification and application risk.
When should a buyer reject a supplier’s lightweighting proposal?
Escalate or reject it when the proposal lacks an exact material grade, hides assumptions about loads or environment, changes interfaces without approval, relies only on simulation or coupons, cannot explain shrinkage and warpage risk, omits tool or inspection consequences, or offers a mass target without a defined measurement method and production-intent validation plan.
References
Source material
- [1] ISO 19069-1:2015, Plastics — Polypropylene moulding and extrusion materials — Part 1: Designation system and basis for specifications
- [2] ISO 19069-2:2016, Plastics — Polypropylene moulding and extrusion materials — Part 2: Preparation of test specimens and determination of properties
- [3] SAE International, Automotive Plastics and Composites technical resources
- [4] AIAG, Production Part Approval Process (PPAP) reference
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.