
Overmolded grips and seals combine a rigid substrate with a softer or more compliant material to add handling comfort, retention, vibration isolation, sealing or environmental protection. For an overseas OEM buyer, the key decision is not simply whether to specify TPE, TPU, silicone or another elastomer. It is whether the selected material pair, interface geometry and molding route can deliver the required function after exposure to the real temperature, chemicals, loads, assembly conditions and service environment.
A reliable sourcing decision separates requirements from recommendations. Requirements should state the function, mating condition, environment, critical dimensions, appearance limits and validation method. Recommendations—such as a candidate hardness, mechanical interlock, surface preparation or two-shot process—should remain subject to supplier DFM review and sample evidence. Resin grade, additives, colour, substrate finish, geometry, tooling, machine, handling, volume and customer specifications can all change the result.
Bond compatibility is not a universal property of a material family. Name the exact substrate and overmold grades, define whether the bond is chemical, mechanical or both, and approve the finished part against the actual application test.
01
1. Start with the grip or seal function, not a material label
A grip may need tactile friction, impact absorption, vibration isolation, retention on a rigid core, resistance to oils or cleaning agents, or a controlled release force. A seal may need compression recovery, low leakage under a defined pressure or fluid, resistance to extrusion, temperature stability, or repeated assembly. These functions are different even when the visible overmold appears similar. Put the failure mode and the acceptance test in the product requirement before asking suppliers to recommend a grade.
Identify the rigid substrate, flexible region, mating parts, compression direction, free-state and assembled dimensions, expected deflection, contact pressure, load duration and cycling. For a grip, specify the hand-contact or clamping condition and any abrasion or sweat/chemical exposure that matters. For a seal, define the fluid, pressure or vacuum condition, compression range, leak method, temperature conditioning and whether the seal is static or dynamic. Do not treat Shore hardness as a complete specification; it does not by itself define adhesion, compression set, friction, tear resistance or service life.
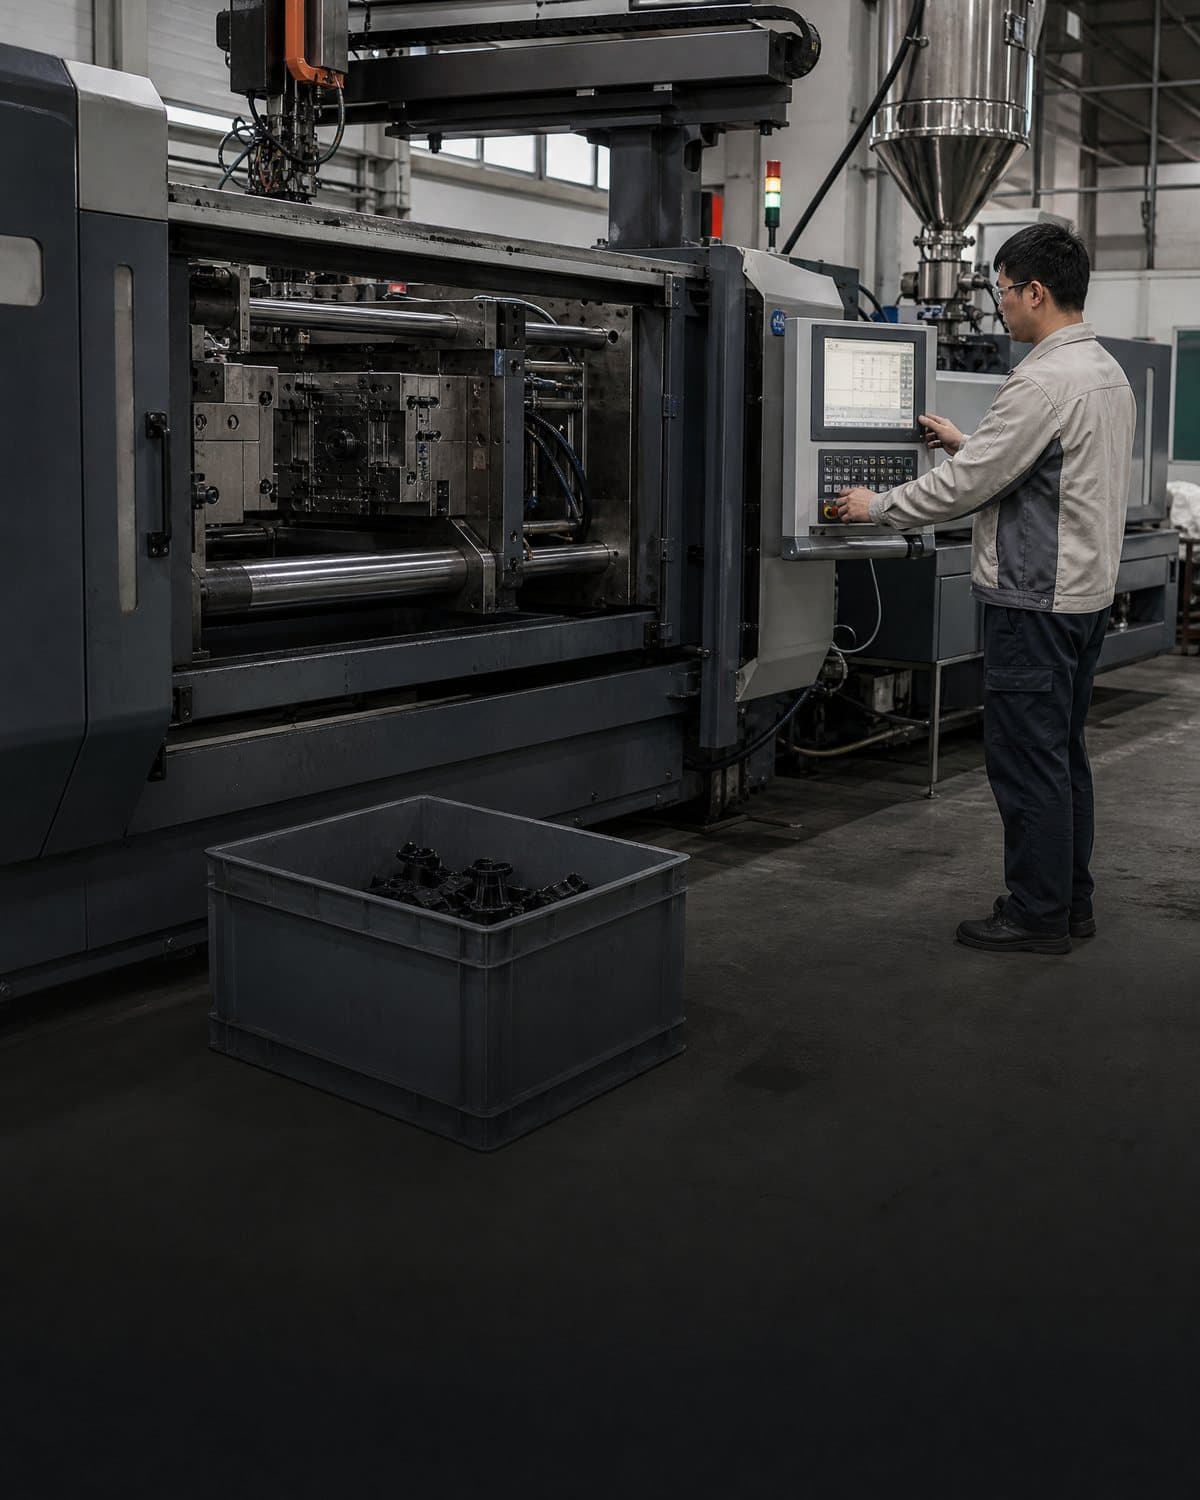
Mark critical zones on the controlled CAD and drawing: bond boundary, seal land, flash-sensitive edge, parting line, gate area, grip texture, datum and mating surfaces. A visual boundary may be acceptable in one zone and unacceptable in another. The supplier should explain how the proposed tool, venting, ejection and material flow protect those zones.
02
2. Compare material and bonding routes against the application
Candidate pairings should be evaluated at the grade level. A thermoplastic elastomer selected for adhesion to one engineering plastic may not adhere to another, and fillers, pigments, plasticizers, flame retardants, recycled content, moisture and surface contamination can change the interface. Chemical bonding may be possible when the substrate remains suitable for bonding during the second shot, but a mechanical interlock may still be prudent or necessary. If direct adhesion is uncertain, a separate adhesive, primer, insert, texture or retained geometry may be considered—but each adds process and validation questions.
Recommendations should reflect the service environment. TPU, TPE, TPV, silicone and other elastomer families have different balances of abrasion, flexibility, compression recovery, temperature resistance, chemical resistance and processing requirements. Use supplier data as a screening input rather than a guarantee for the finished geometry. Request the exact grade data sheet, processing guidance, colour/additive basis, lot traceability and any restrictions on substitutions.
The table below is a sourcing framework, not a universal material-selection rule. The final route should be approved using representative parts, the intended substrate, the controlled tool concept and the customer’s validation requirements.
A substrate that is easy to mold may not be easy to bond. Surface energy, cooling state, mould release, texture, venting, shrinkage mismatch and handling time can influence the result. Ask the supplier to state whether the proposed mechanism is chemical adhesion, mechanical retention, or both, and how it will be checked after conditioning.
| Decision route | Potential fit | Main risk to review | Evidence before approval |
|---|---|---|---|
| Direct chemical adhesion | Clean integrated appearance and no separate adhesive operation | Grade-specific compatibility, contamination, additives, ageing or processing-window sensitivity | Exact-grade pairing study, interface inspection and aged adhesion or functional test |
| Mechanical interlock | Useful when chemical compatibility is uncertain or additional retention is required | Stress concentration, trapped air, difficult filling, flash or interference with seal compression | Section review, pull/peel or torque test as applicable, and assembled-part check |
| Two-shot molding | Integrated transfer and potentially consistent registration for stable high-volume designs | Higher tooling commitment, transfer alignment, substrate distortion and limited change flexibility | Tool concept, process window, cavity/shot evidence and production-intent samples |
| Separate overmolding operation | Can support design changes, modest volume or a complex loading sequence | Handling, orientation, cleanliness, cooling state and repeatability between operations | Work instruction, locating method, bond/fit study and lot-level inspection plan |
| Adhesive or primer-assisted interface | May enable a material combination that does not reliably bond in molding alone | Additional chemical, cure, cleanliness, worker-safety and long-term ageing controls | Approved chemical system, process controls, compatibility review and environmental validation |
03
3. Design the interface for filling, retention and sealing
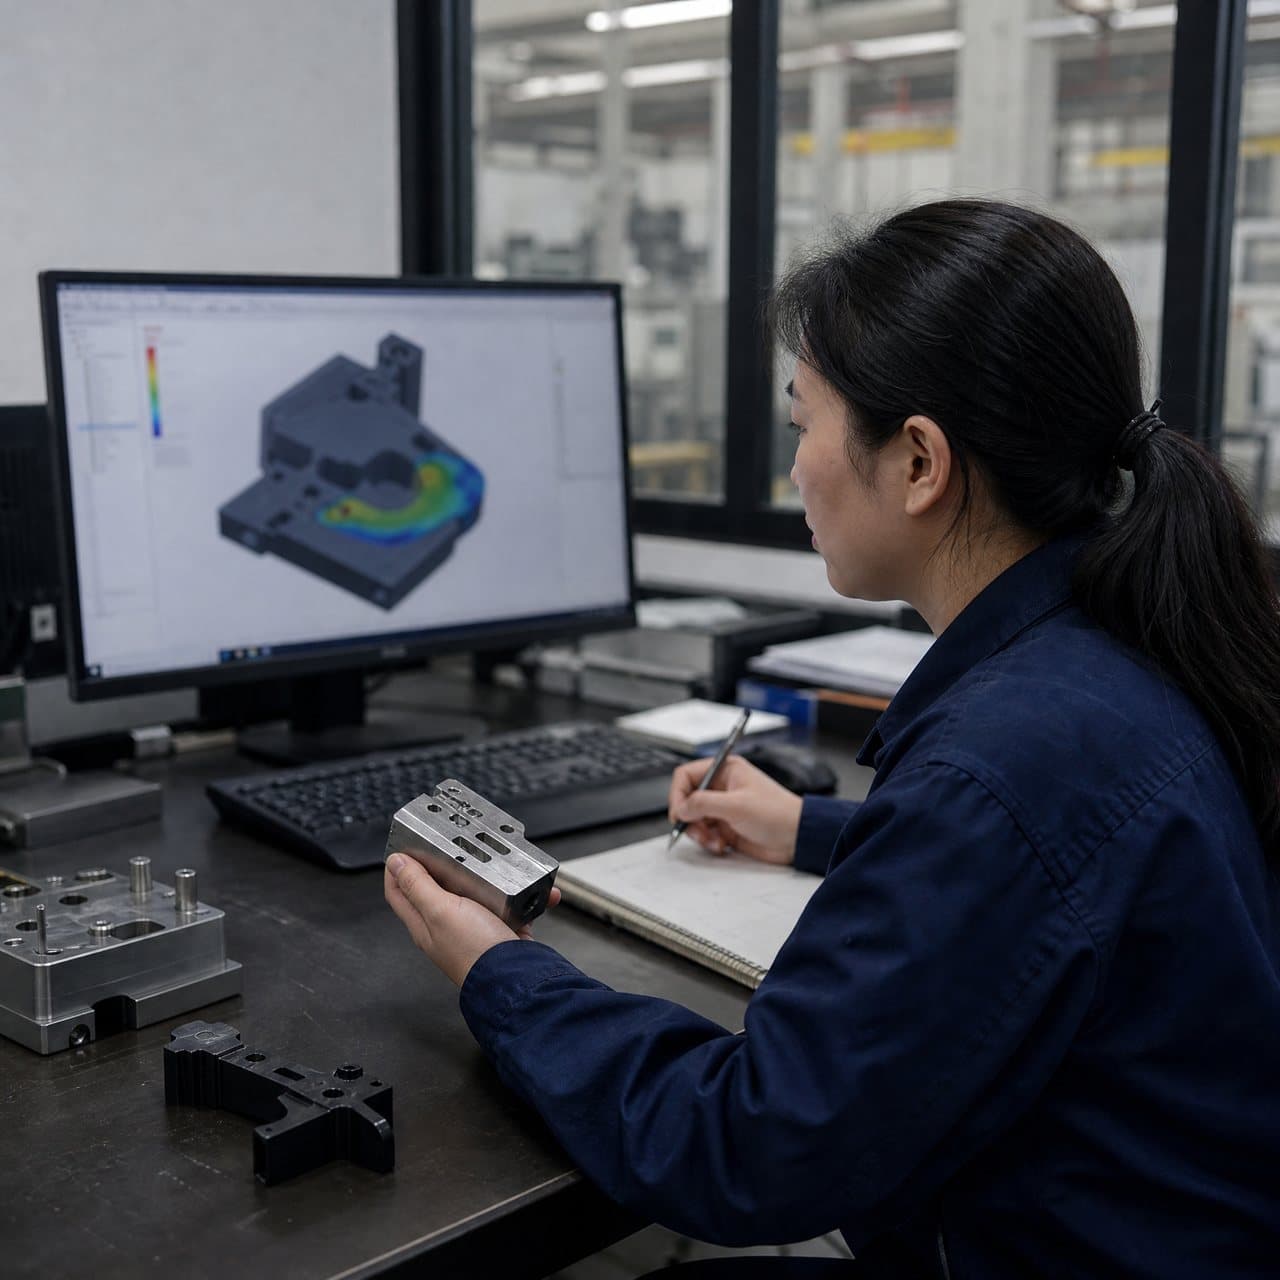
The interface geometry should support the intended load without creating a new molding defect. Use positive stops, undercuts, holes, grooves, ribs or other retention features only where the mold can form and release them and where they do not compromise the seal land or substrate strength. A broad bond area is not automatically stronger; peel, torsion, axial pull, compression and shear can load the boundary differently. Ask the supplier to show the load path and the expected flow-front or weld-line locations around the interface.
For seals, distinguish the elastomer’s free-state geometry from the installed condition. Define compression, squeeze, gap, gland or locating features, mating surface finish where relevant, and any pressure direction. The overmold should not be allowed to substitute for an unreviewed tolerance stack. For grips, define the retention force, allowable movement, tactile zone, texture and edge transition. If the flexible material is also a datum or locator, state how it will be measured without deforming it.
Gate, vent and parting-line decisions deserve early approval. Flash at a seal edge can cause leakage or assembly interference; a gate vestige on a hand-contact zone can affect comfort; a weld line through a retention feature may require functional testing. Request marked-up CAD showing permitted and prohibited locations, along with the proposed ejection and trimming approach.
04
4. Choose the process route and supplier evidence
Two-shot molding forms the substrate and the overmold within an integrated tool using a transfer, rotation or core-back concept. It may suit stable geometry and volume, but the tool commitment and change-control implications should be clear. A separate overmolding operation forms the substrate first, then loads and locates it in a second mold. It may offer flexibility, but handling, orientation, substrate temperature, cleanliness and operator or automation controls become part of the quality plan. Compare total programme risk and evidence—not only tool price or quoted piece price.
At RFQ stage, ask each supplier to identify the assumed substrate grade, elastomer grade, colour, hardness direction, shot sequence, gate and vent locations, locating features, cavity strategy, expected secondary work, inspection method and proposed validation. Require disclosure of any alternative grade or process route. A quoted cycle, yield, tool life, price or capacity is a programme-specific assumption until it is demonstrated for the released design and process.
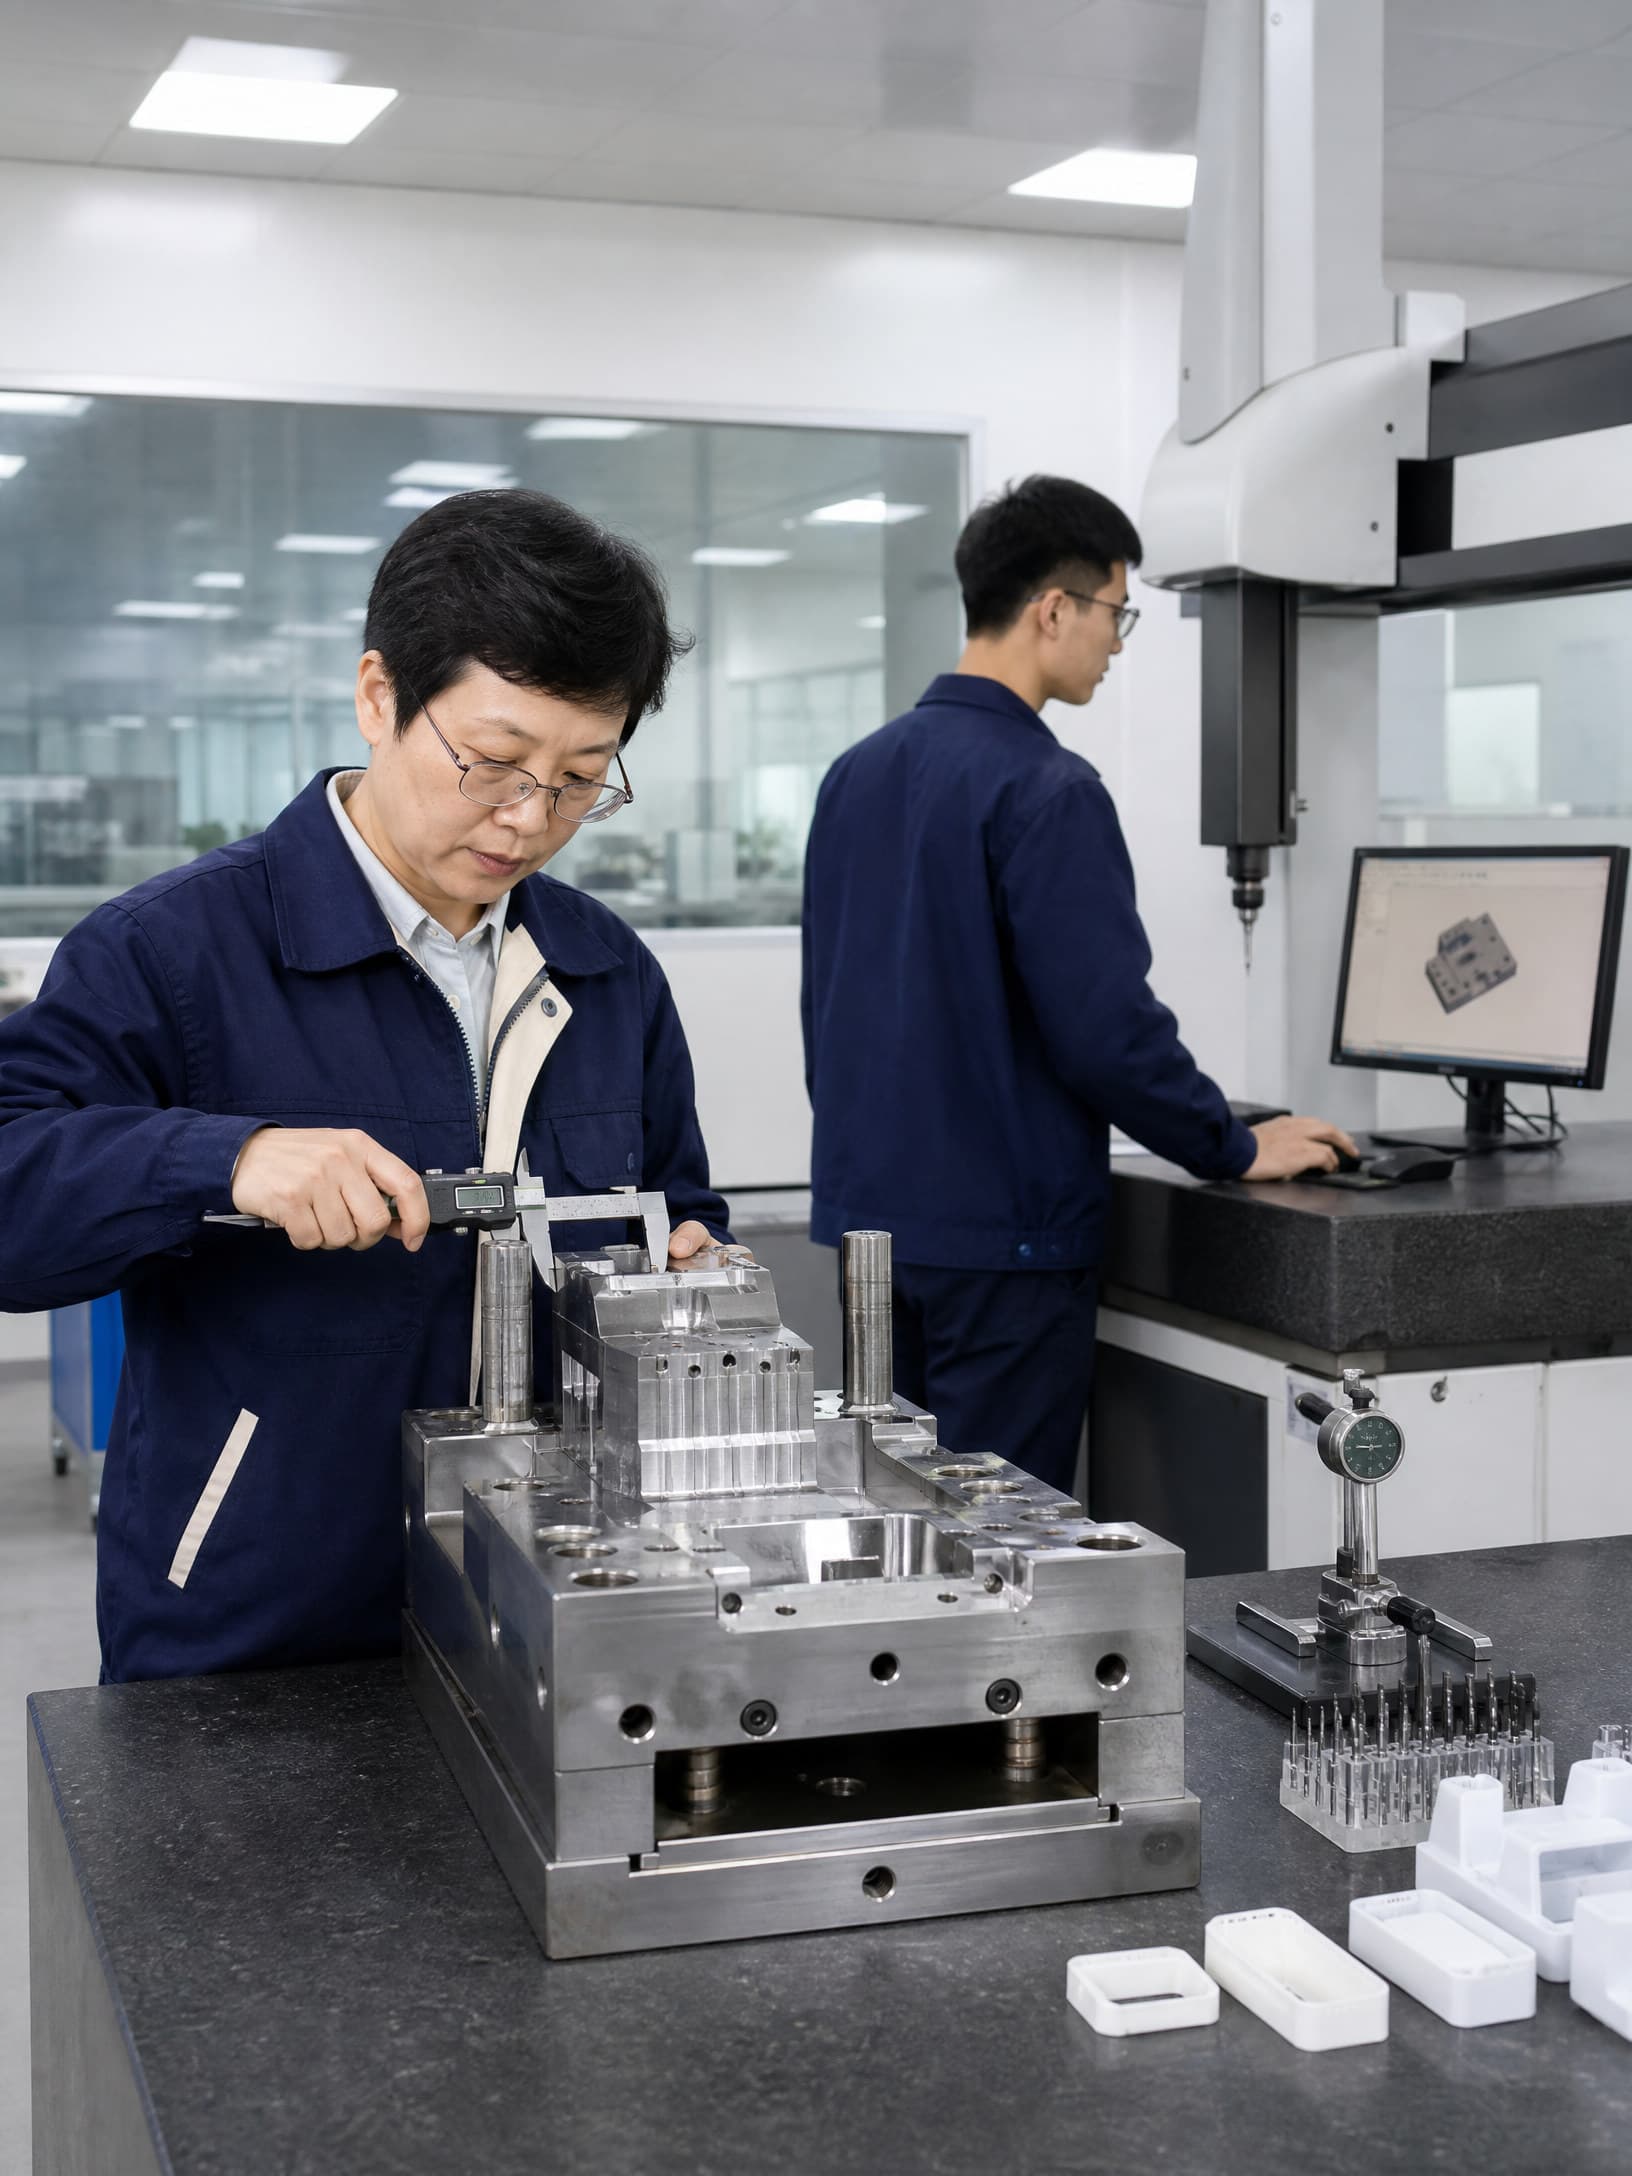
Useful supplier evidence can include a DFM review, material compatibility rationale, interface cross-section, flow or filling assessment where justified, tool concept, handling work instruction, bond or retention test plan, dimensional inspection plan and first-trial risk list. For soft features, define conditioning, measurement force and fixture before comparing results. A contact probe can deform an elastomer; optical, vision, CMM, functional gauges or a combination may be appropriate only after repeatability is considered.
05
5. Use staged approval gates for the finished part
Gate 1—requirements: approve the function, exact mating condition, substrate and overmold material direction, environment, CTQs, cosmetic zones and test method. Gate 2—DFM and tooling: approve the interface geometry, retention mechanism, gates, vents, parting line, ejection, process route and open assumptions. Gate 3—sample: inspect substrate and finished dimensions, bond boundary, flash, appearance, assembly, grip retention or seal performance using representative samples. Gate 4—production readiness: confirm material traceability, process records, inspection frequency, reaction plan, packaging and change notification.
Validation should match the risk. Depending on the application, this may include pull, peel, torque, compression, leak, pressure, abrasion, repeated assembly, thermal cycling, chemical exposure, humidity, UV, vibration or ageing. Do not select a test merely because it is easy to run. Define sample conditioning, fixture, load direction, duration, acceptance limit and failure disposition in advance. A short-term adhesion result does not by itself establish service life.
Before purchase-order release, require a written list of what is a requirement, what is a supplier recommendation and what remains open. If a supplier proposes a resin substitution, surface treatment, geometry change, new adhesive, machine transfer or tool repair that could affect bonding, sealing, grip feel, appearance or CTQs, route it through the agreed engineering change and revalidation process.
Practical takeaway
Before you move
to the next review.
- Define the grip or seal function, failure modes, mating condition, environment and part-level acceptance tests before selecting a material family.
- Name the exact substrate and overmold grades, colour/additive basis, hardness direction and permitted substitution process; do not rely on a generic TPE, TPU or silicone label.
- Mark bond boundaries, seal lands, grip zones, CTQs, gates, vents, parting lines, flash limits and measurement datums on controlled CAD or drawings.
- Request a documented comparison of direct adhesion, mechanical interlock, two-shot molding and separate overmolding for the actual geometry, volume and change profile.
- Hold approval until representative samples demonstrate the required dimensional, assembly, bond, retention, leak, environmental and appearance evidence under agreed conditions.
FAQ
Common questions
What is the best material for an overmolded grip or seal?
There is no universal best material. The suitable grade depends on the required grip or seal function, substrate, compression or load, temperature, chemicals, abrasion, ageing, appearance, tooling route and customer specification. Compare named grades using representative samples and the application-specific validation plan rather than choosing from hardness alone.
Does a TPE automatically bond to an ABS, PC or nylon substrate?
No. Adhesion is grade- and process-dependent. The substrate and TPE formulation, additives, colour, surface condition, mould release, timing, temperature, geometry and tool design can all affect the interface. Ask the supplier to state the proposed chemical or mechanical bonding mechanism and provide evidence on the actual material pair.
Should an OEM choose two-shot molding or a separate overmolding operation?
Choose by programme risk, not by a universal volume rule. Two-shot molding may provide integrated registration for a stable design but can require greater tooling commitment. Separate overmolding may support changes or complex loading but adds handling, locating, cleanliness and repeatability controls. Compare the actual geometry, forecast, change profile, validation burden and total cost assumptions.
How should overmold bond strength or seal performance be approved?
Define the failure mode and test before tooling release. Depending on the application, evidence may include pull, peel, torque, compression, leak, pressure, repeated assembly, abrasion, chemical, thermal or ageing tests. State the sample condition, fixture, load direction, duration, acceptance limit and lot or cavity basis. A visual boundary or one short-term test is not proof of universal service life.
References
Source material
- [1] Protolabs — Overmolding and Insert Molding
- [2] Teknor Apex — The Essential Guide to Overmolding Process and Materials
- [3] ASTM International — ASTM D429, Standard Test Methods for Rubber Property—Adhesion to Rigid Substrates
- [4] ASTM International — ASTM D395, Standard Test Methods for Rubber Property—Compression Set
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.