
For a food-contact component, a resin name or supplier letter is only one input to a procurement decision. The buyer needs a documented chain from intended use and destination market to exact formulation, molded-part controls, test evidence, approval status and change notification. That chain should be agreed before tooling is released, because a change in resin source, colourant, contact surface or process can alter the evidence needed for the finished article.
This guide is for overseas OEM, procurement, quality, engineering and product teams buying custom injection molded parts. It separates requirements from recommendations and treats validation as a part-specific, risk-based decision. FDA explains that the regulatory status of a food-contact material depends on the individual substances reasonably expected to migrate and on the applicable authorization. In the EU, plastic articles placed on the market need a written declaration of compliance at relevant marketing stages under Regulation (EU) No 10/2011. Neither principle makes a generic “food-safe” claim equivalent to approval of a finished molded part.
Do not approve a food-contact molded part from a material datasheet alone. Require an evidence map that links the exact grade and additives, intended use, destination market, finished-part revision, validation method and release owner.
01
What documentation should a buyer require before quoting?
Start with a controlled use statement. It should identify the destination markets, food categories, direct or indirect contact, single-use or repeated-use expectation, contact duration, storage conditions, temperature profile, hot-fill or reheating exposure, cleaning method and any sterilisation or chemical exposure. These are requirements when they define the legal or functional basis of the product; a supplier should not be asked to infer them from a part number.
Request an evidence index rather than a loose folder of certificates. At minimum, ask the bidder to identify the exact resin manufacturer and grade, colour or masterbatch, additives, filler, recycled-content or regrind policy, lot traceability method, declaration or letter supplied, test reports, report dates, laboratories, sample description and stated conditions of use. Ask which documents are supplier-controlled and which decisions remain with the OEM or its regulatory adviser.
For an EU-bound article, Regulation (EU) No 10/2011 describes a written declaration of compliance and supporting information for plastic materials and articles. For the United States, FDA lists several possible authorization routes, including applicable regulations, GRAS status, prior sanctions, threshold-of-regulation exemptions or an effective Food Contact Substance Notification. An FCN is tied to the manufacturer, substance and conditions identified in the notification, so traceability to the actual material source matters.
02
How should validation be divided into approval gates?
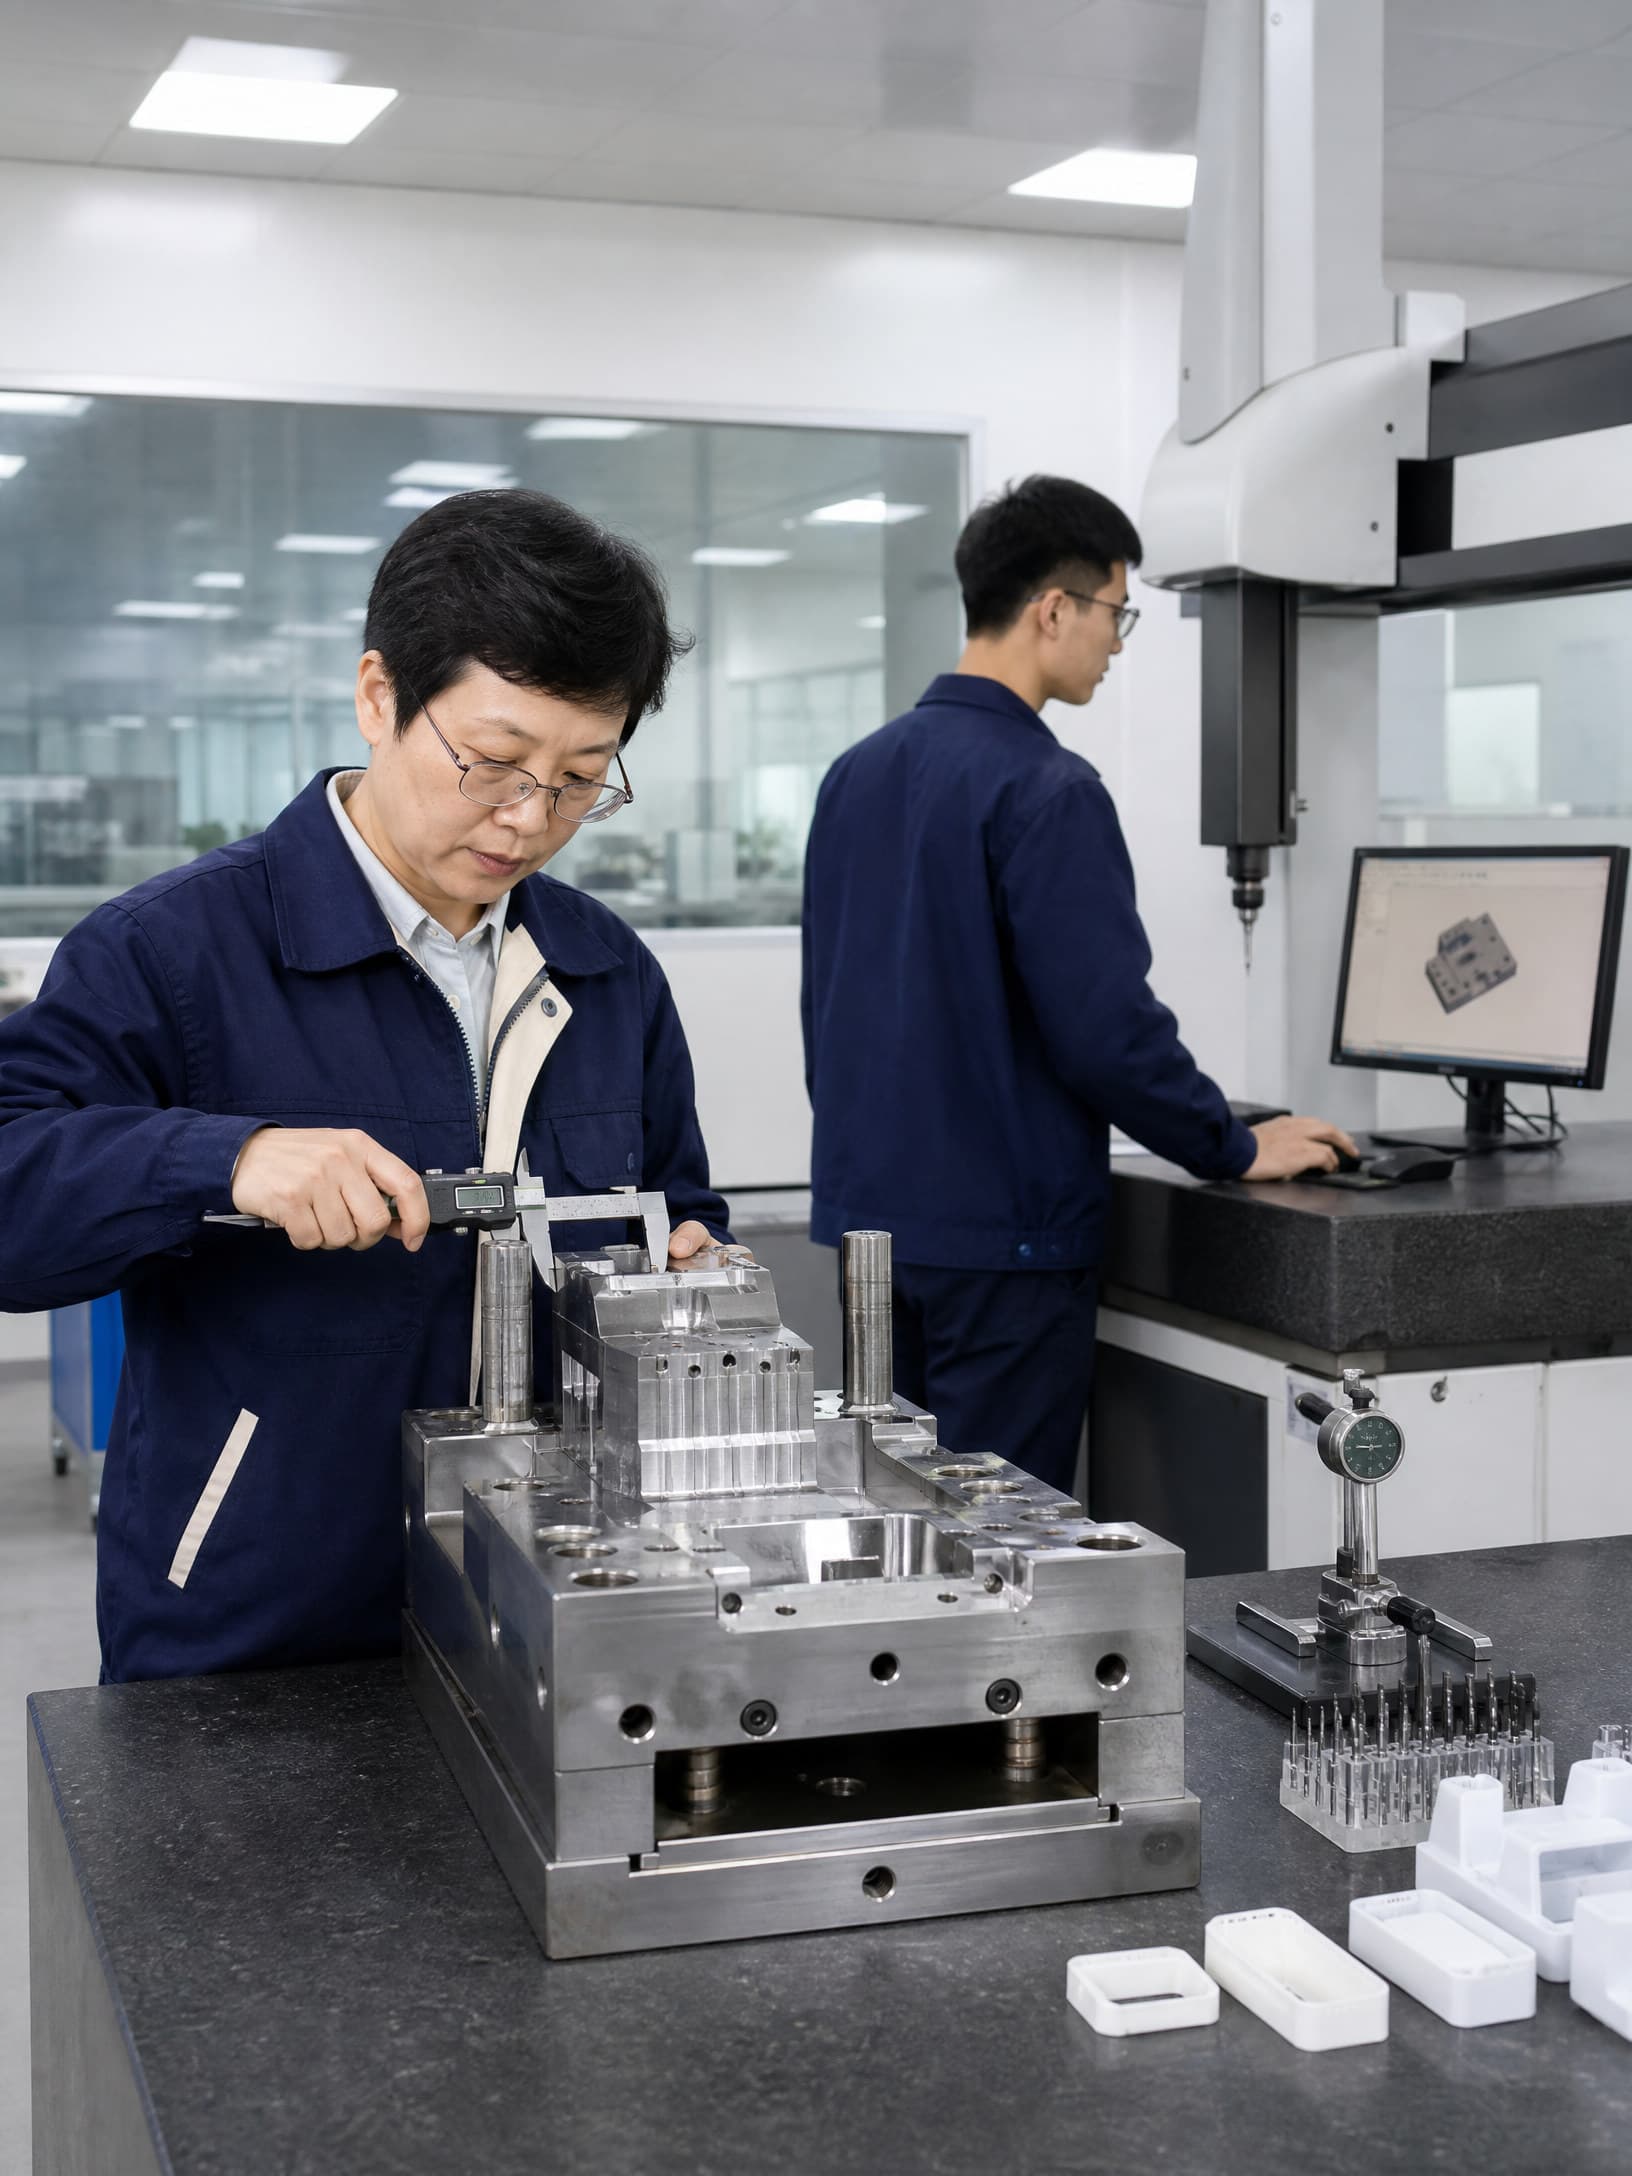
Use staged gates so procurement does not treat a quotation, first-off sample or dimensional report as final compliance approval. A practical sequence is: Gate 1, intended-use and market review; Gate 2, material and formulation evidence review; Gate 3, tool and process readiness review; Gate 4, molded-part inspection and agreed functional or migration assessment; Gate 5, production release with lot records and change control. The exact tests, sample quantities and acceptance limits must be set by the product owner and competent technical or regulatory reviewers.
At the tooling gate, review the contact surface and features that could affect cleaning, retention, leakage, odour, residue or assembly. Consider gate location, weld lines, flash, ejector marks, surface texture, vents, inserts and secondary operations. These are engineering review topics, not automatic reasons to reject a design. The evidence plan should state which features are critical and how they will be checked.
At the release gate, connect the approved part revision to the approved material identity, tool identifier, process record, inspection plan, packaging and disposition of nonconforming product. A first-article approval can establish what was accepted at that revision, but it does not by itself demonstrate long-term migration, repeated-use durability or compliance in every market. Those conclusions require the agreed product-specific evidence.
03
Compare supplier evidence without confusing documents with validation
When comparing quotes, score the completeness and applicability of evidence separately from piece price. A low-cost proposal that leaves the formulation, test basis or change pathway unclear can create later rework, retesting or market-access risk. Conversely, a long document list is not automatically stronger if the reports cover a different grade, colour, geometry, use condition or manufacturing source.
Use the table below as a procurement comparison aid. It is not a universal compliance checklist. Mark each item as required, recommended or not applicable, and record the accountable reviewer and approval date. Ask every bidder to state assumptions and exclusions in writing so that commercial comparisons remain meaningful.
The buyer should also distinguish supplier capability evidence from product evidence. A quality certificate, audit report or general clean-room statement may describe a system or facility, but it does not prove that a specific molded article meets a food-contact requirement. Request only claims and certificates that the supplier can substantiate, and verify scope, validity, issuing body and applicability to the supplying entity.
| Decision area | Minimum required input | Evidence to request from supplier | Approval owner |
|---|---|---|---|
| Intended use | Market, food type, time, temperature, cleaning and reuse profile | Written scope confirmation and stated assumptions | OEM product and regulatory team |
| Material identity | Exact grade, source, colourant, additives, filler and regrind rule | Current technical data, declaration or letter, lot traceability and change notice route | Materials and quality team |
| Finished-part validation | Approved drawing revision and contact-surface definition | Inspection report, agreed functional checks and any required migration assessment | Engineering and quality |
| Production control | Tool ID, process record, sampling plan and nonconformance reaction | Control plan, records retained, batch identification and containment procedure | Supplier quality and OEM quality |
| Change control | Triggers covering material, source, additives, tool, process and use | Written notification timing, impact review and reapproval pathway | Named change authority |
04
What should validation cover for the molded article?
Validation should be tied to the failure modes and use conditions of the actual component. Depending on the application, the plan may need dimensional and visual inspection, seal or leak performance, fit and function, cleaning compatibility, thermal conditioning, repeated-use cycling, odour or taste assessment, or chemical exposure. Migration testing may be relevant, but the required food simulants, contact conditions, analytical method and acceptance criteria are not the same for every article.
Define the sample basis before testing. Record the part revision, cavity or tool identification, resin lot, colour and additive system, molding date, process state, conditioning, packaging and laboratory method. If a test uses representative plaques or standard specimens rather than finished parts, document why that representation is technically justified and what limitations remain. A coupon result should not silently become a finished-article approval.
For EU projects, the regulation provides migration and food-simulant provisions and requires the declaration of compliance to be renewed when substantial composition or production changes affect migration or when relevant new scientific data becomes available. For other markets, use the applicable local route. The product owner should approve the validation rationale, while the supplier should provide accurate manufacturing and material records needed to support it.
05
How do you release supply and control changes after approval?
Make the release package operational. It should identify the approved part and drawing revision, exact material and permitted alternatives, contact surfaces, critical dimensions, visual limits, inspection methods, packaging, lot coding, record-retention expectations and escalation contacts. Define what happens when a lot fails: containment, investigation, disposition, customer notification and reinspection should not be improvised after shipment.
Require written notification before changes that could affect the evidence basis. Examples include resin manufacturer or grade, colourant, additive, filler, recycled content, regrind ratio, mold cavity or surface, gate or vent design, process window, machine, subcontracted operation, cleaning agent, packaging or declared end use. Not every change needs the same level of revalidation, but every change should receive a documented impact assessment by the named owner.
Before awarding business, ask the supplier to demonstrate how a lot can be traced back to material and production records and how obsolete documents are prevented from being reused. A supplier audit can test whether the stated process exists, but audit completion does not replace approval of the specific part. Release only when the agreed evidence gaps are closed or formally accepted by the responsible OEM team.
Practical takeaway
Before you move
to the next review.
- State destination markets, food categories, contact duration, temperature, storage, cleaning, reuse and sterilisation conditions before requesting a quote.
- Identify the exact resin grade, manufacturer, colour or masterbatch, additives, filler, regrind or recycled-content rule and permitted alternatives.
- Request an evidence index linking declarations, authorization basis, test reports, sample identity, laboratory details, lot traceability and document revision.
- Define approval gates for use scope, material, tooling and process readiness, finished-part validation, first-article release and routine production.
- Agree written change-control triggers, notification timing, impact assessment, revalidation responsibility and nonconformance containment before production supply.
FAQ
Common questions
Is a food-contact declaration for the resin enough to release a molded part?
Usually not by itself. It can support the material assessment, but the buyer should confirm that it covers the exact grade, formulation, source and intended conditions of use. The finished article, its geometry, manufacturing controls and destination-market obligations still require a product-specific review and release decision.
Does every food-contact injection molded part need migration testing?
Do not write a universal yes or no into the RFQ. The need and method depend on the market, formulation, article, food type, contact conditions and available supporting evidence. The product owner and competent technical or regulatory reviewer should document the rationale, including whether finished-part testing, calculation, supplier data or another route is appropriate.
Can we approve a colour or resin substitution as an equivalent change?
Treat it as a proposed change until its impact is reviewed. Colourants, additives, source, processing behaviour and migration profile can differ even when the base polymer family is unchanged. Require the supplier to identify the new formulation and provide the evidence needed for the applicable reapproval gate.
What should an overseas buyer ask a molding supplier to retain for each lot?
Agree the record set contractually. It may include part and tool identification, production date, material and lot identity, approved process or machine record, inspection results, quantity, packaging code, deviations and disposition. Retention period and access should follow the OEM's product, market and quality requirements rather than an assumed universal period.
References
Source material
- [1] U.S. Food and Drug Administration — Determining the Regulatory Status of Components of a Food Contact Material
- [2] U.S. Food and Drug Administration — Food Types & Conditions of Use for Food Contact Substances
- [3] European Commission — Food Contact Materials
- [4] EUR-Lex — Commission Regulation (EU) No 10/2011 on plastic materials and articles intended to come into contact with food
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.